Chocolate Brand Case Study | Luxury Heat-Resistant Packaging Specifications
Solving Core Packaging Challenges for Chocolate Brand Case Study | Luxury Heat-Resistant Packaging
Concise B2B technical benchmarks designed to eliminate transit failures, regulatory penalties, and shelf-life loss.
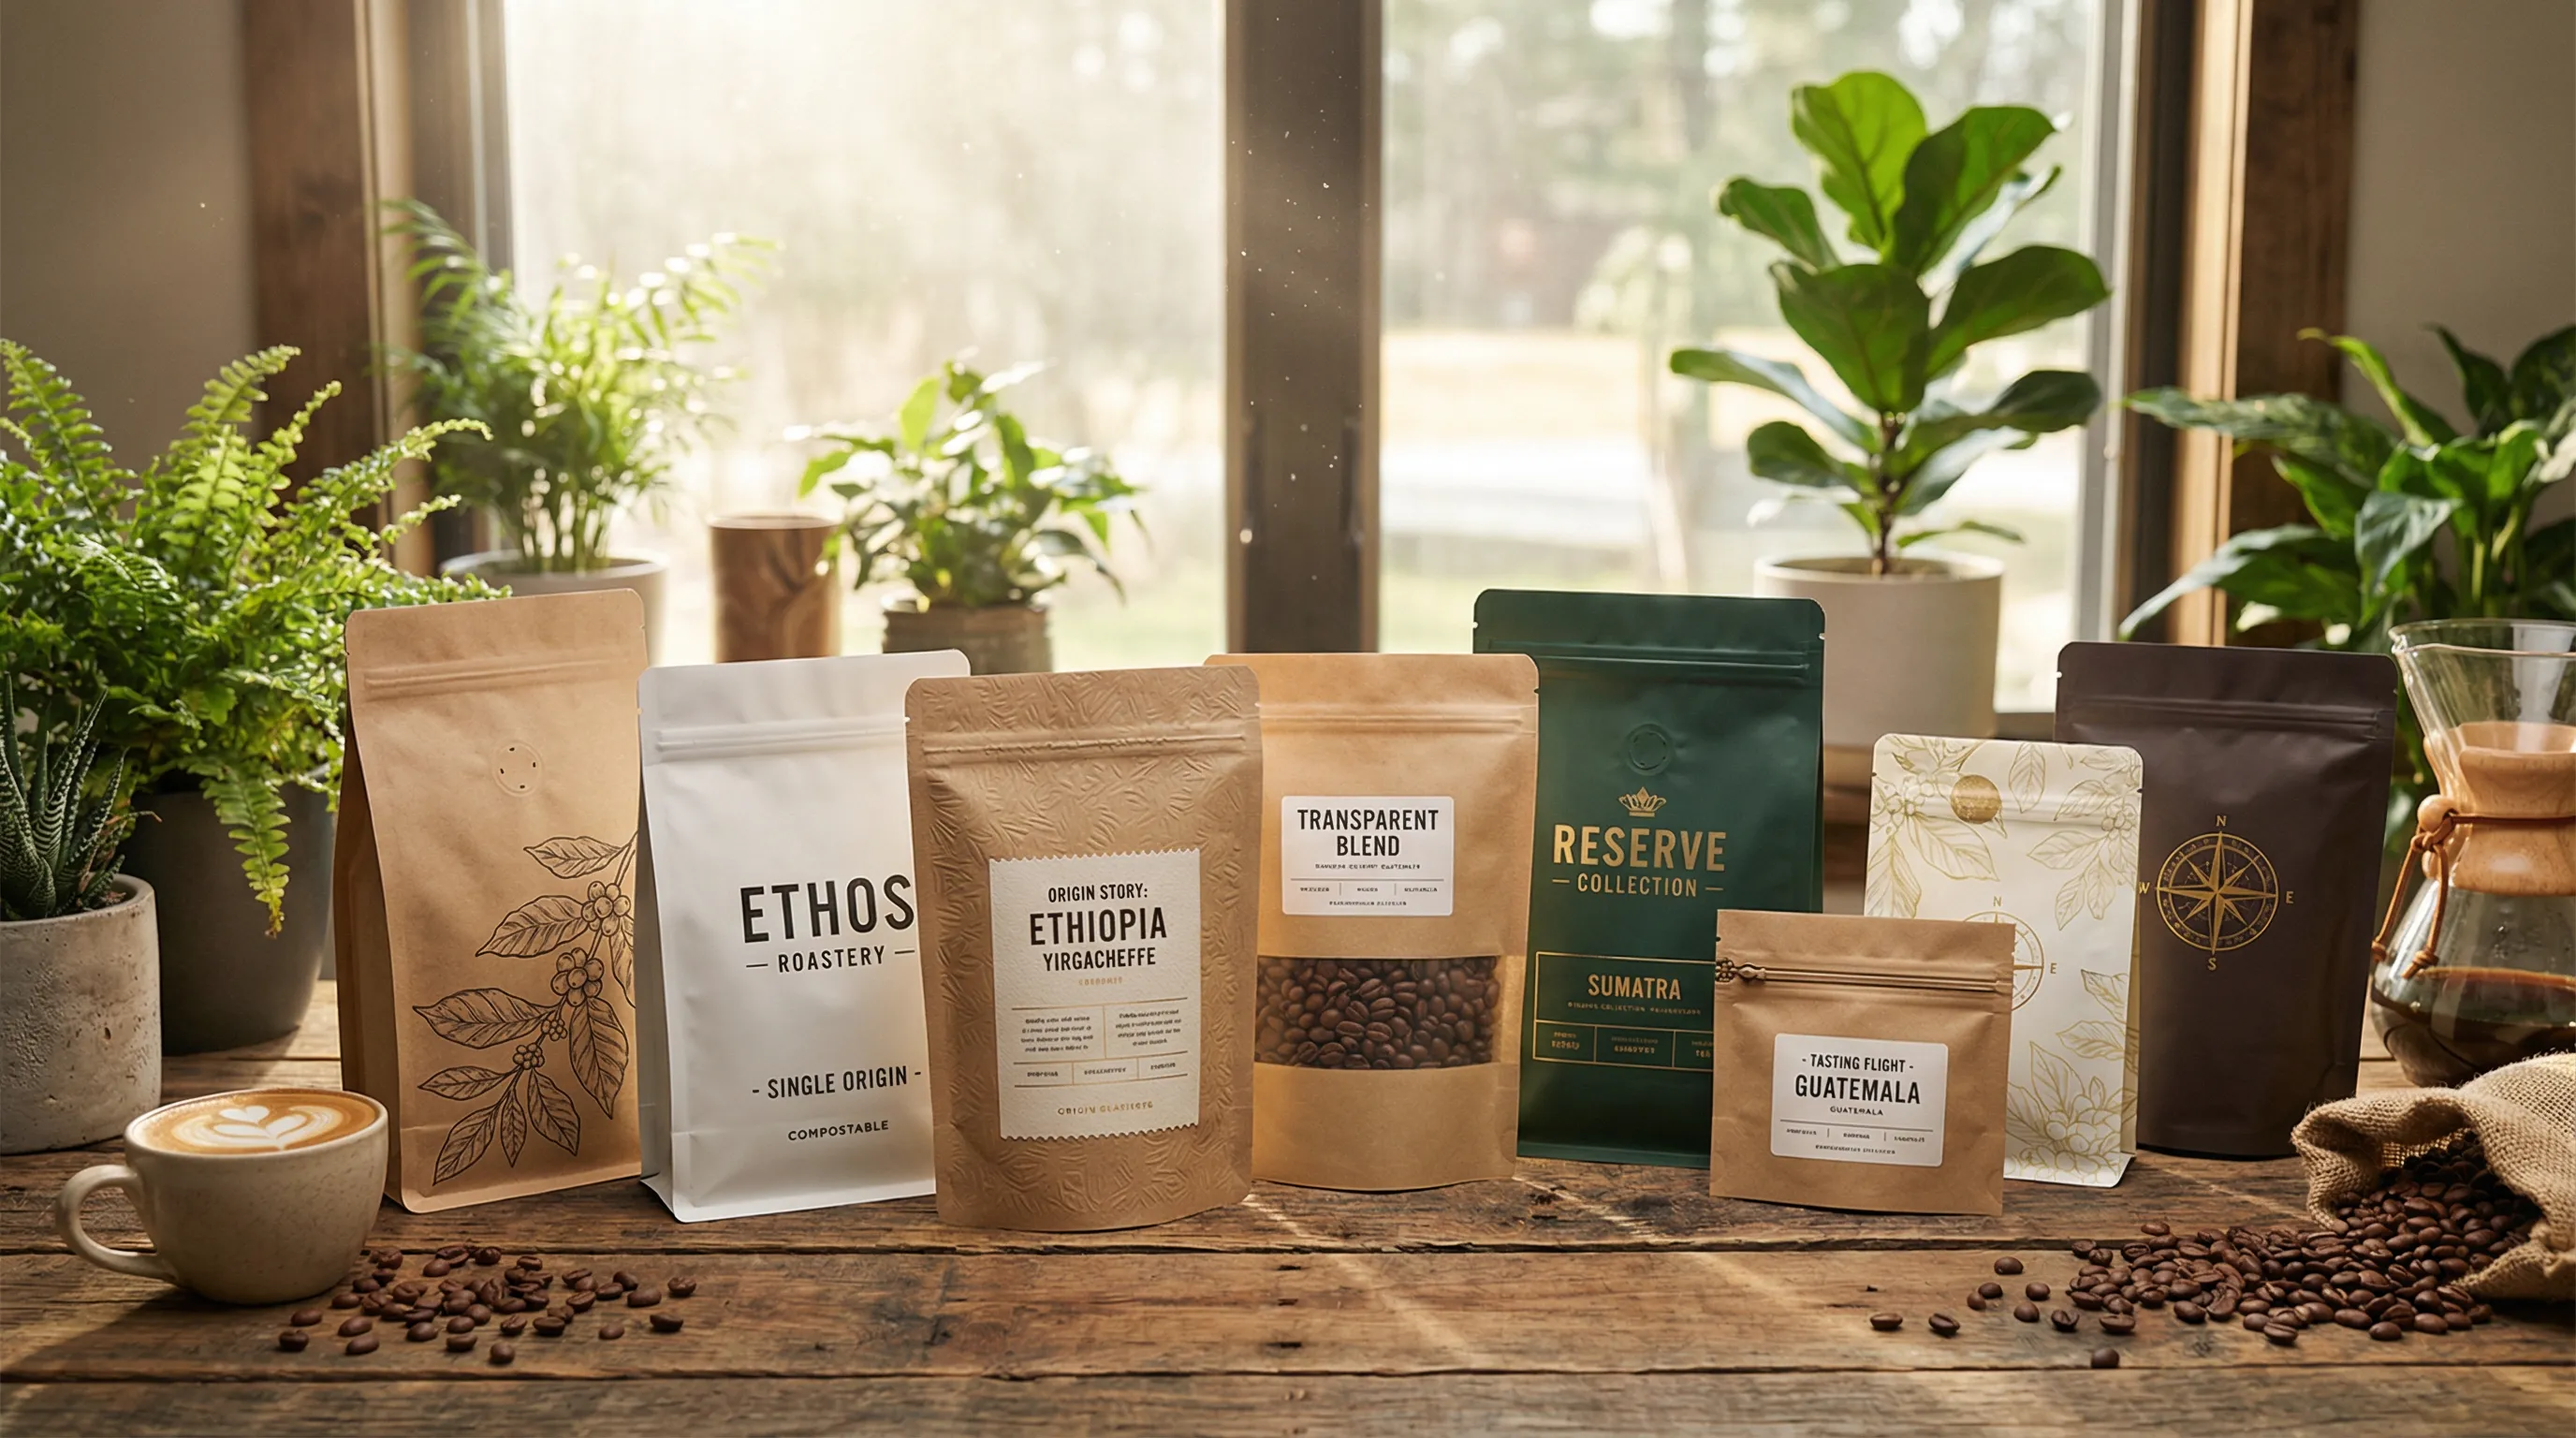
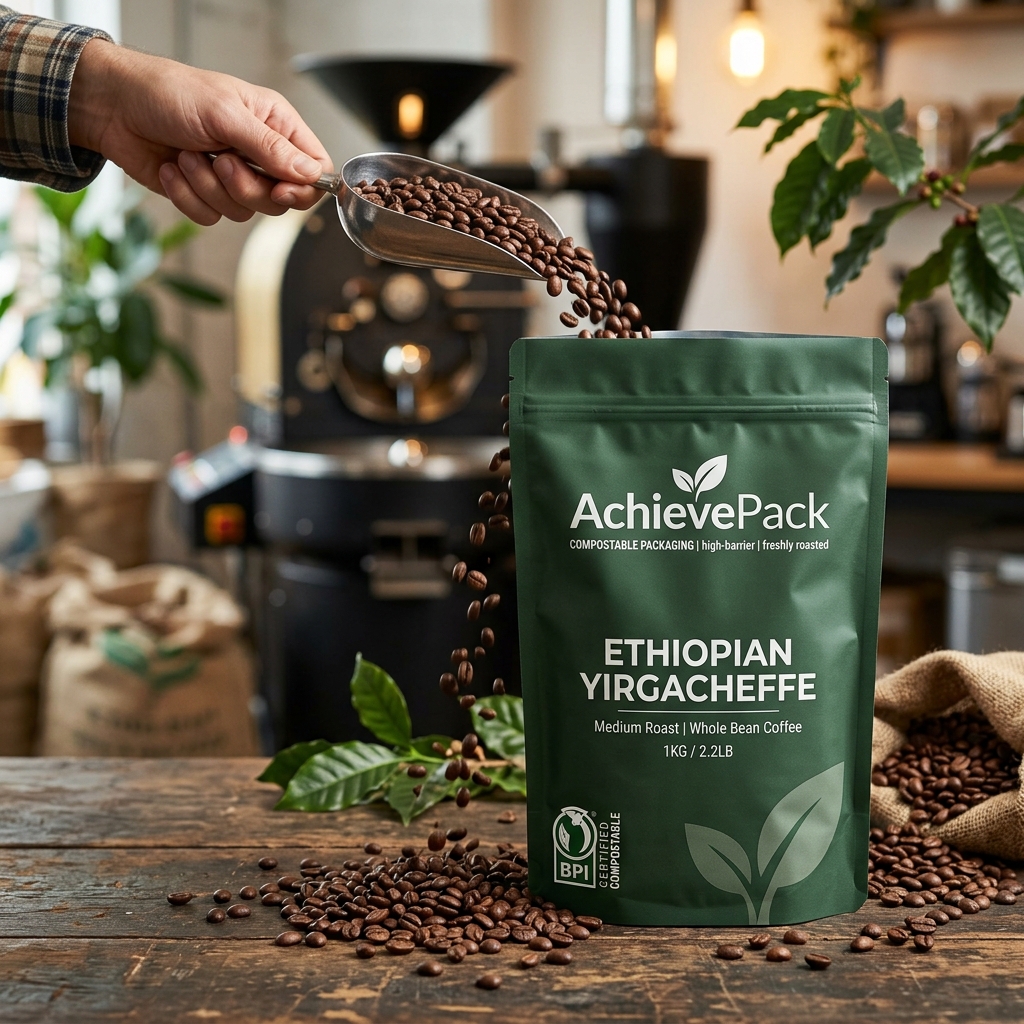
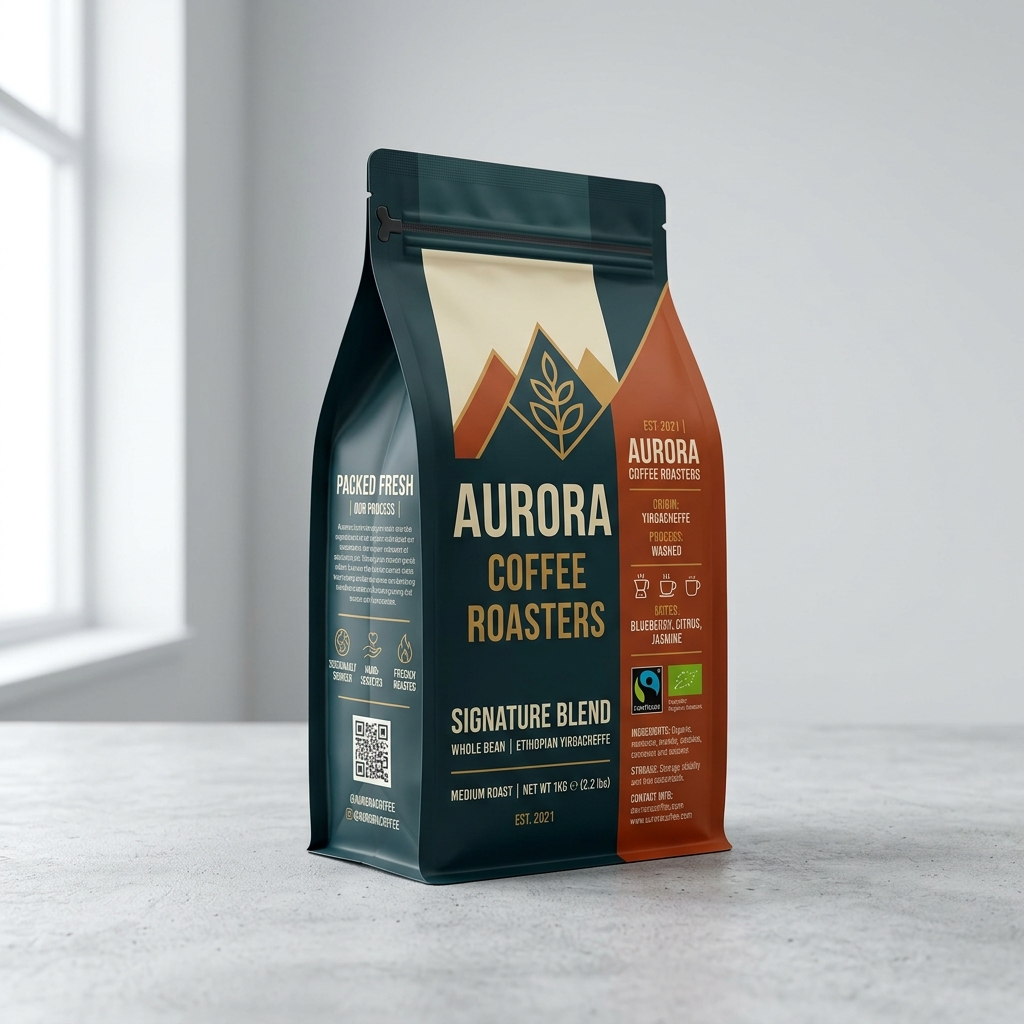
Aroma Loss & Degassing Failure in Speciality Roast
Risk: Beans oxidize quickly, resulting in customer complaints and lost brand value.
One-Way Eco Degassing Valve + Metallized High-Barrier Film
Preserves CO2 outgassing without admitting oxygen or moisture.
Plastic Tax Liability & EU PPWR Compliance Risks
Risk: Non-recyclable multi-layer plastics incur heavy customs tariffs & fines in EU/US.
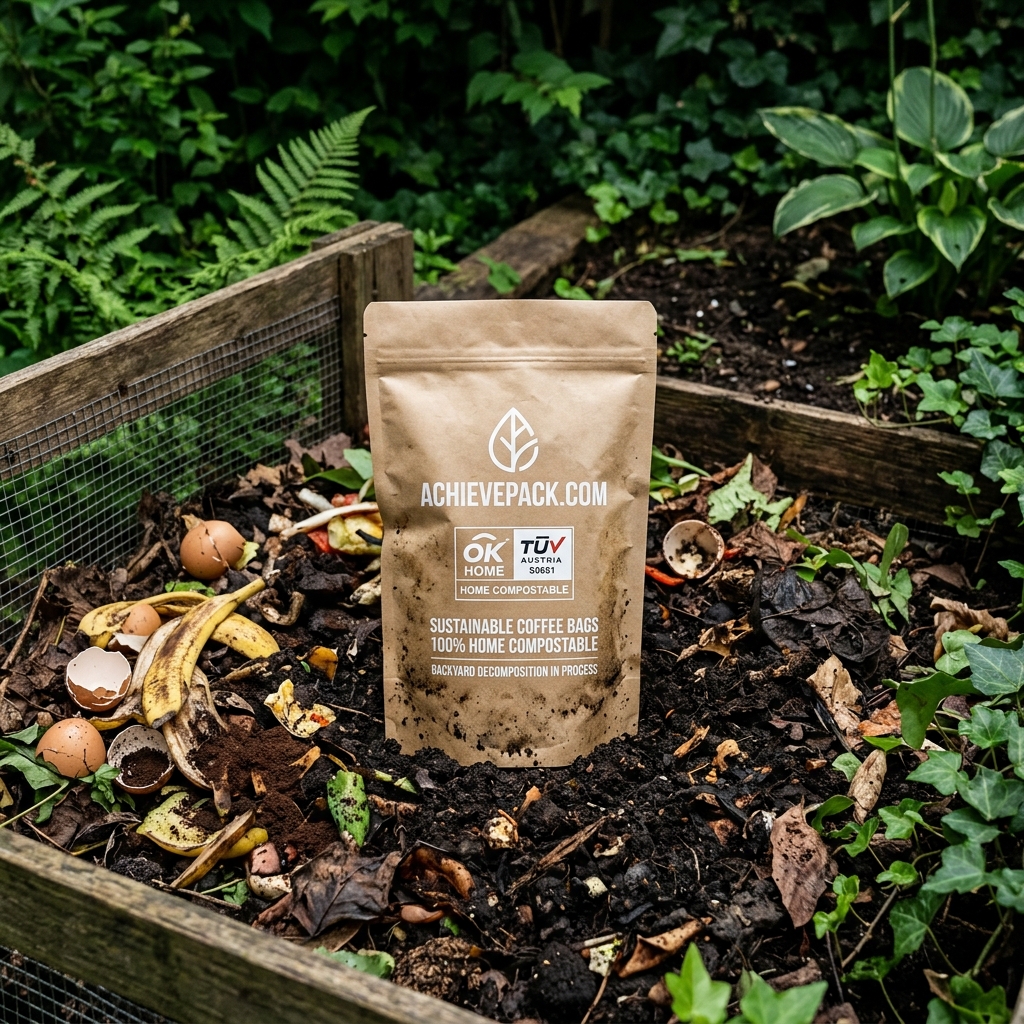
100% Home Compostable (PLA) or Mono-Material Recyclable PE
Fully GRS & TÜV OK Compost HOME certified for global distribution.
High MOQs & Generic Stock Packaging Stifling DTC Launches
Risk: Small brands forced to buy 10,000+ units or rely on plain generic bags.
Digital HD Printing with 500-Unit Low MOQs & 3D Interactive Design
Print multi-SKU designs instantly with zero plate fees.
Experience 3D Packaging Design & Free Dielines
Preview your pouch in 3D WebGL Studio and export production-ready dielines.
Who Is This Client?
Company
Bean-to-bar chocolate maker (name withheld)
Industry
Luxury Artisan Chocolate
Location
Abu Dhabi, UAE
Package Type
Premium Flat Bottom Bags
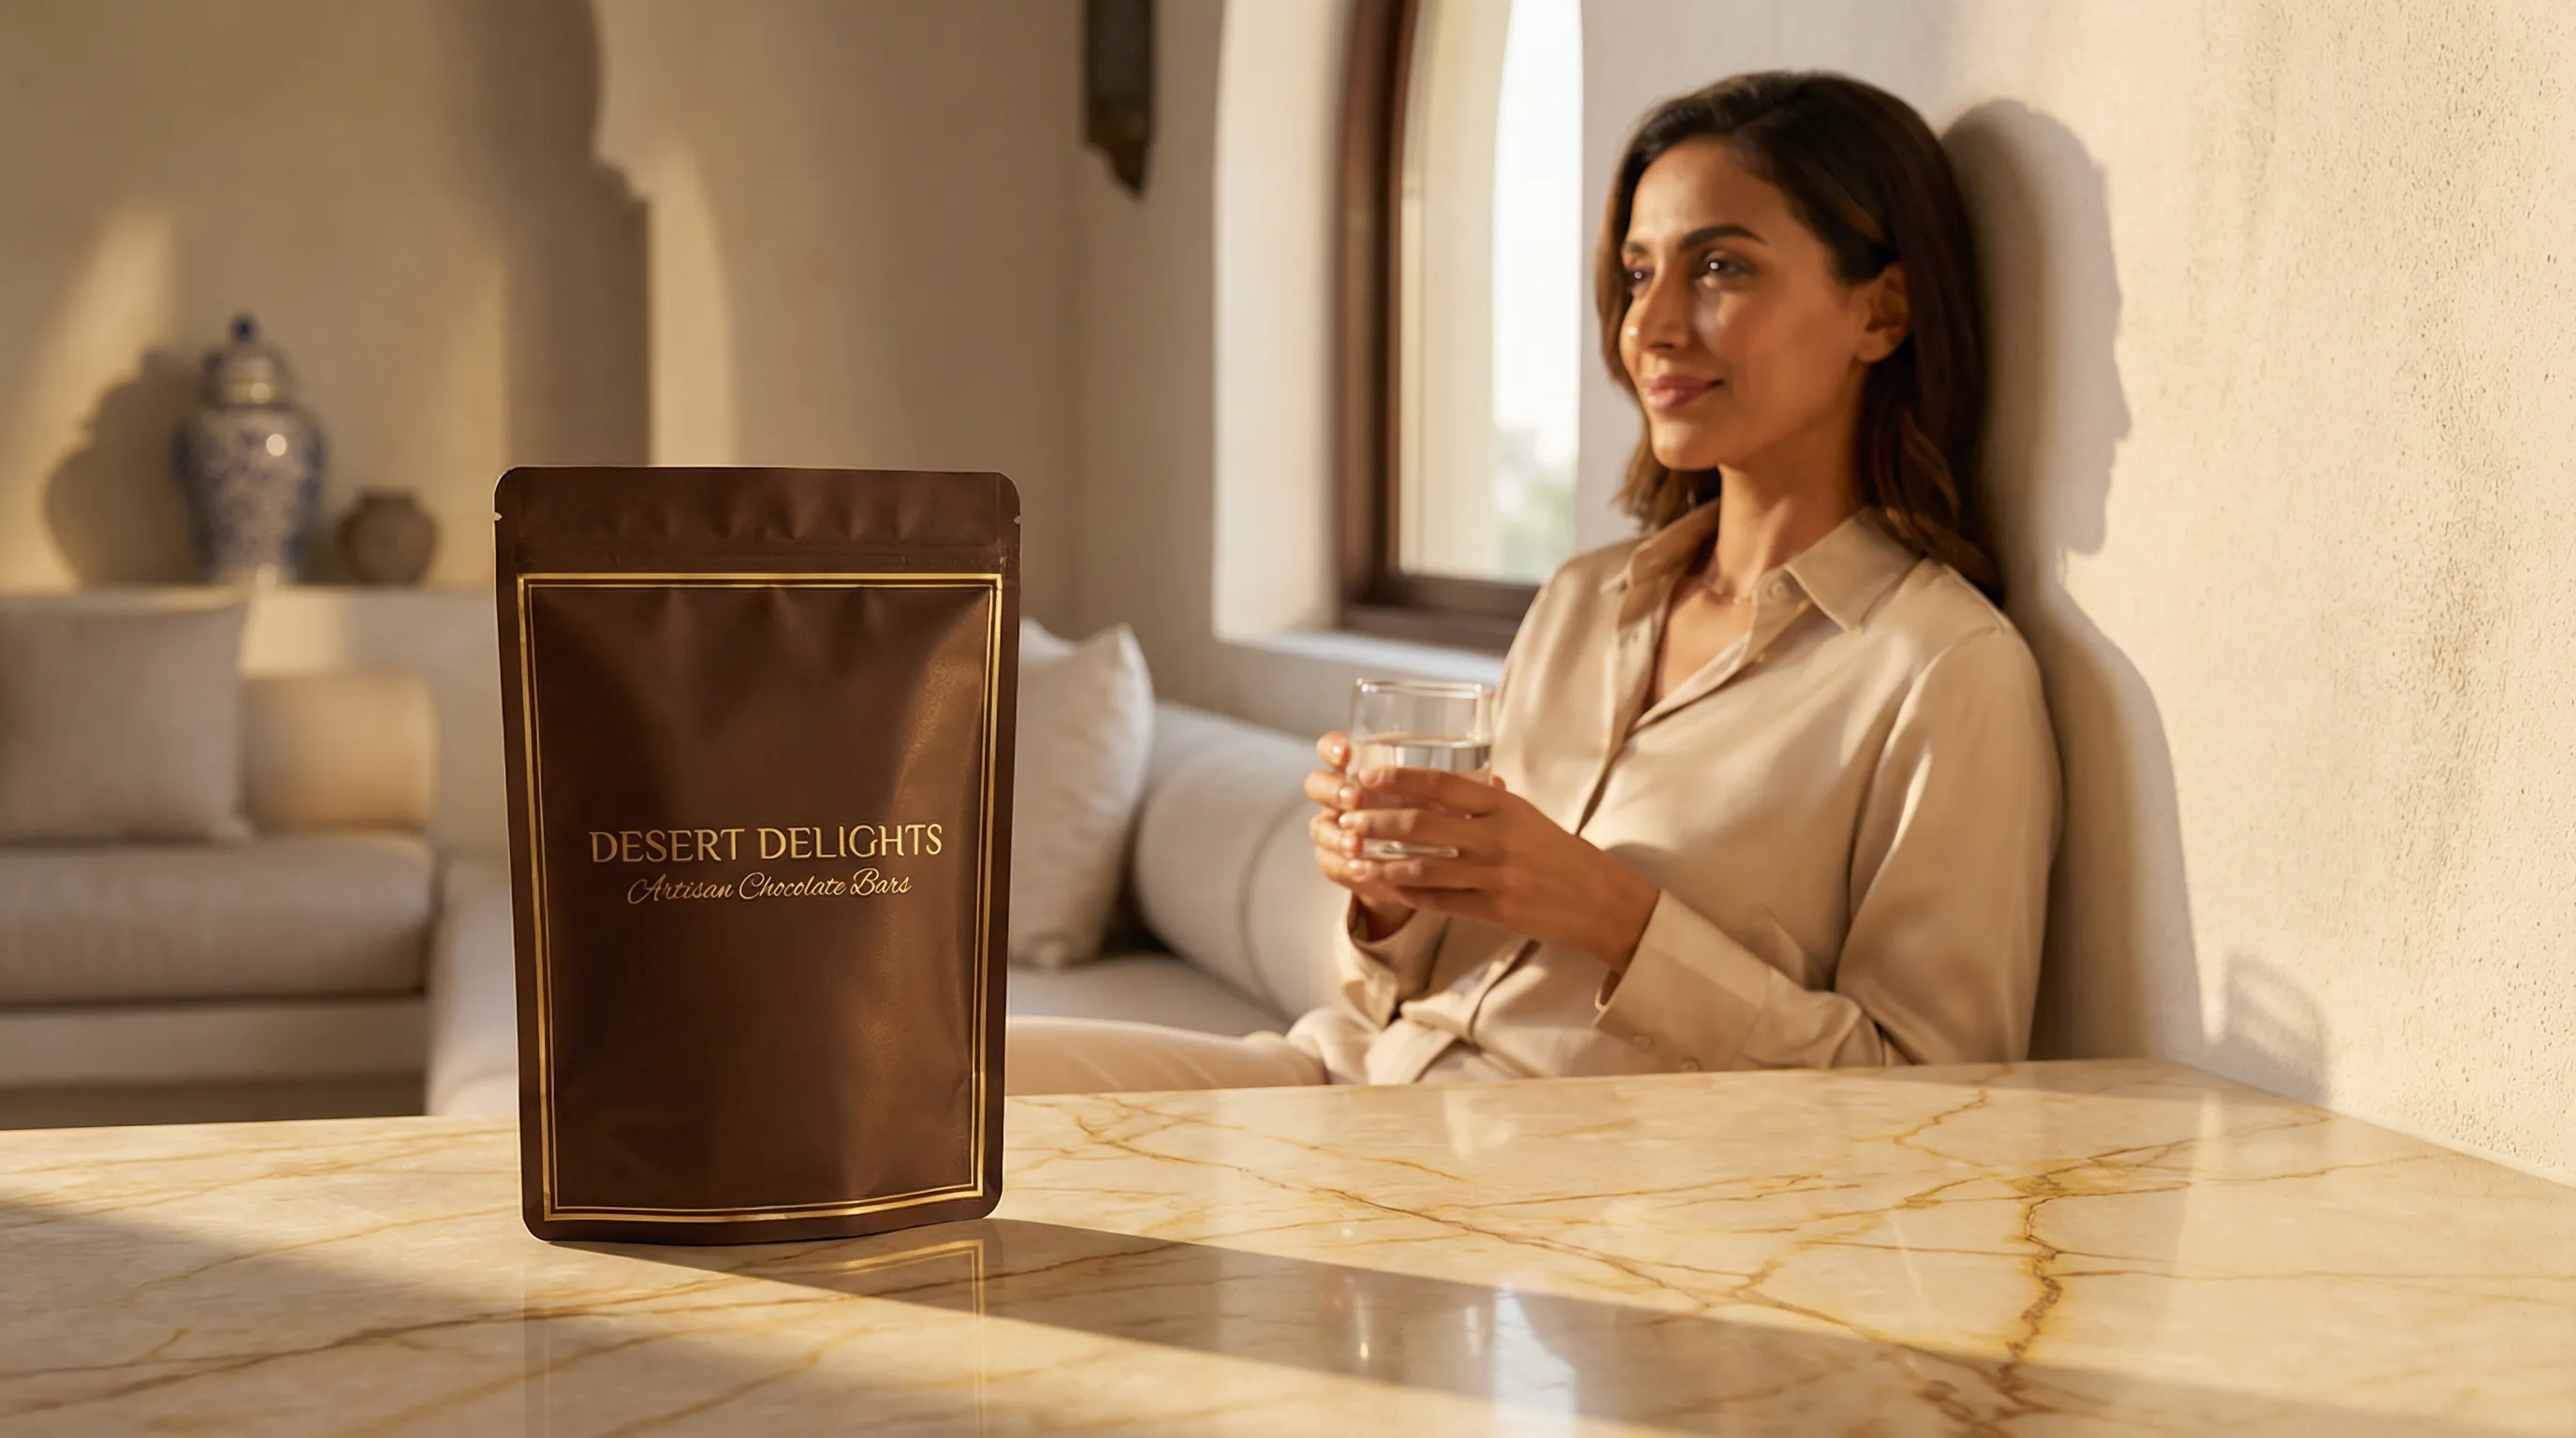
A luxury bean-to-bar chocolate maker in Abu Dhabi supplying high-end hotels and retail. Operating in extreme heat, they needed packaging that protects chocolate while conveying premium quality.
What Challenge Did They Face?
- ✗Extreme heat exposure during Middle East distribution
- ✗Luxury presentation required for 5-star hotel clients
- ✗Gift-worthy packaging for retail and corporate gifting
- ✗Sustainability story for eco-conscious luxury market
How Did Achieve Pack Help?
Maximum Barrier Structure
Recyclable mono-PP with aluminum-free barrier technology for maximum heat and moisture protection.
Gold Foil Stamping
Premium gold foil accents on matte black finish for luxury shelf presence.
Soft-Touch Lamination
Velvety texture that invites touch and conveys premium quality.
Flat Bottom Stability
Stands beautifully on hotel boutique shelves and gift displays.
What Results Did They Achieve?
"The packaging elevated our brand instantly. Hotels that previously said no are now stocking our chocolates. The soft-touch finish gets compliments every time."
What This Case Study Does NOT Mean for You
Before you spec this structure, know the limits:
- • Heat-tested to 45°C does NOT mean heat-proof. A pouch slows heat transfer; it is not refrigeration. Chocolate still needs shaded, temperature-managed logistics.
- • Recyclable mono-PP is NOT curbside-recyclable everywhere. Whether your customer's local stream accepts it depends on their municipality—word your claims accordingly.
- • Gold foil and soft-touch finishes are NOT free upgrades. They add unit cost and require plate printing—so the MOQ is higher than a basic digital run.
- • Their 55% gift-sales increase is NOT a guarantee. Packaging supported a sales push that included pricing, placement, and product quality.
Want to feel the finishes before committing? The $40+ sample kit (credited to your first order) includes soft-touch and foil-stamped examples. Questions: /support/contact.
What Packaging Specs Were Used?
Coffee Packaging Engineering & Valve Testing
Roasting coffee releases carbon dioxide and is extremely sensitive to oxygen. We validate our degassing valve release pressure, OTR/WVTR barrier, and heat seal strength to ensure coffee aroma protection and long-term shelf life.
MOCON OTR Barrier Test
Tested under ASTM D3985 to preserve coffee aromatics and lock out oxygen.
GC-MS Solvent Residue
Gas Chromatography-Mass Spectrometry guarantees zero odor transfer into coffee beans.
Heat Seal Strength (ASTM F88)
Optimized seal strength to support heavy 1kg coffee bags without seam ruptures.
Valve Seating Pressure
Tested pressure release to expel internal CO₂ while maintaining a hermetic oxygen seal.
Puncture Test (ASTM F1306)
Prevents whole roasted coffee beans from piercing the inner laminate layers.
VFFS Line Speed Match
Sliding friction coefficient optimized for high-speed automatic bagging lines.
Packaging Transformation for Chocolate Brand Case Study | Luxury Heat-Resistant Packaging
See how upgrading from generic commoditized bags to precision-engineered flexible barrier packaging eliminates transport failures and boosts shelf authority.
Standard / Generic Packaging (Before)
Standard stock bags fail under transit stress and expose sensitive goods to moisture, UV light, and oxygen.
- Rapid Oxidation & Flavor DegradationCheap films allow O2 & moisture ingress, spoiling contents in < 30 days.
- High Seal Breakage in TransitThin seams fail under drop tests, leading to customer refunds & lost trust.
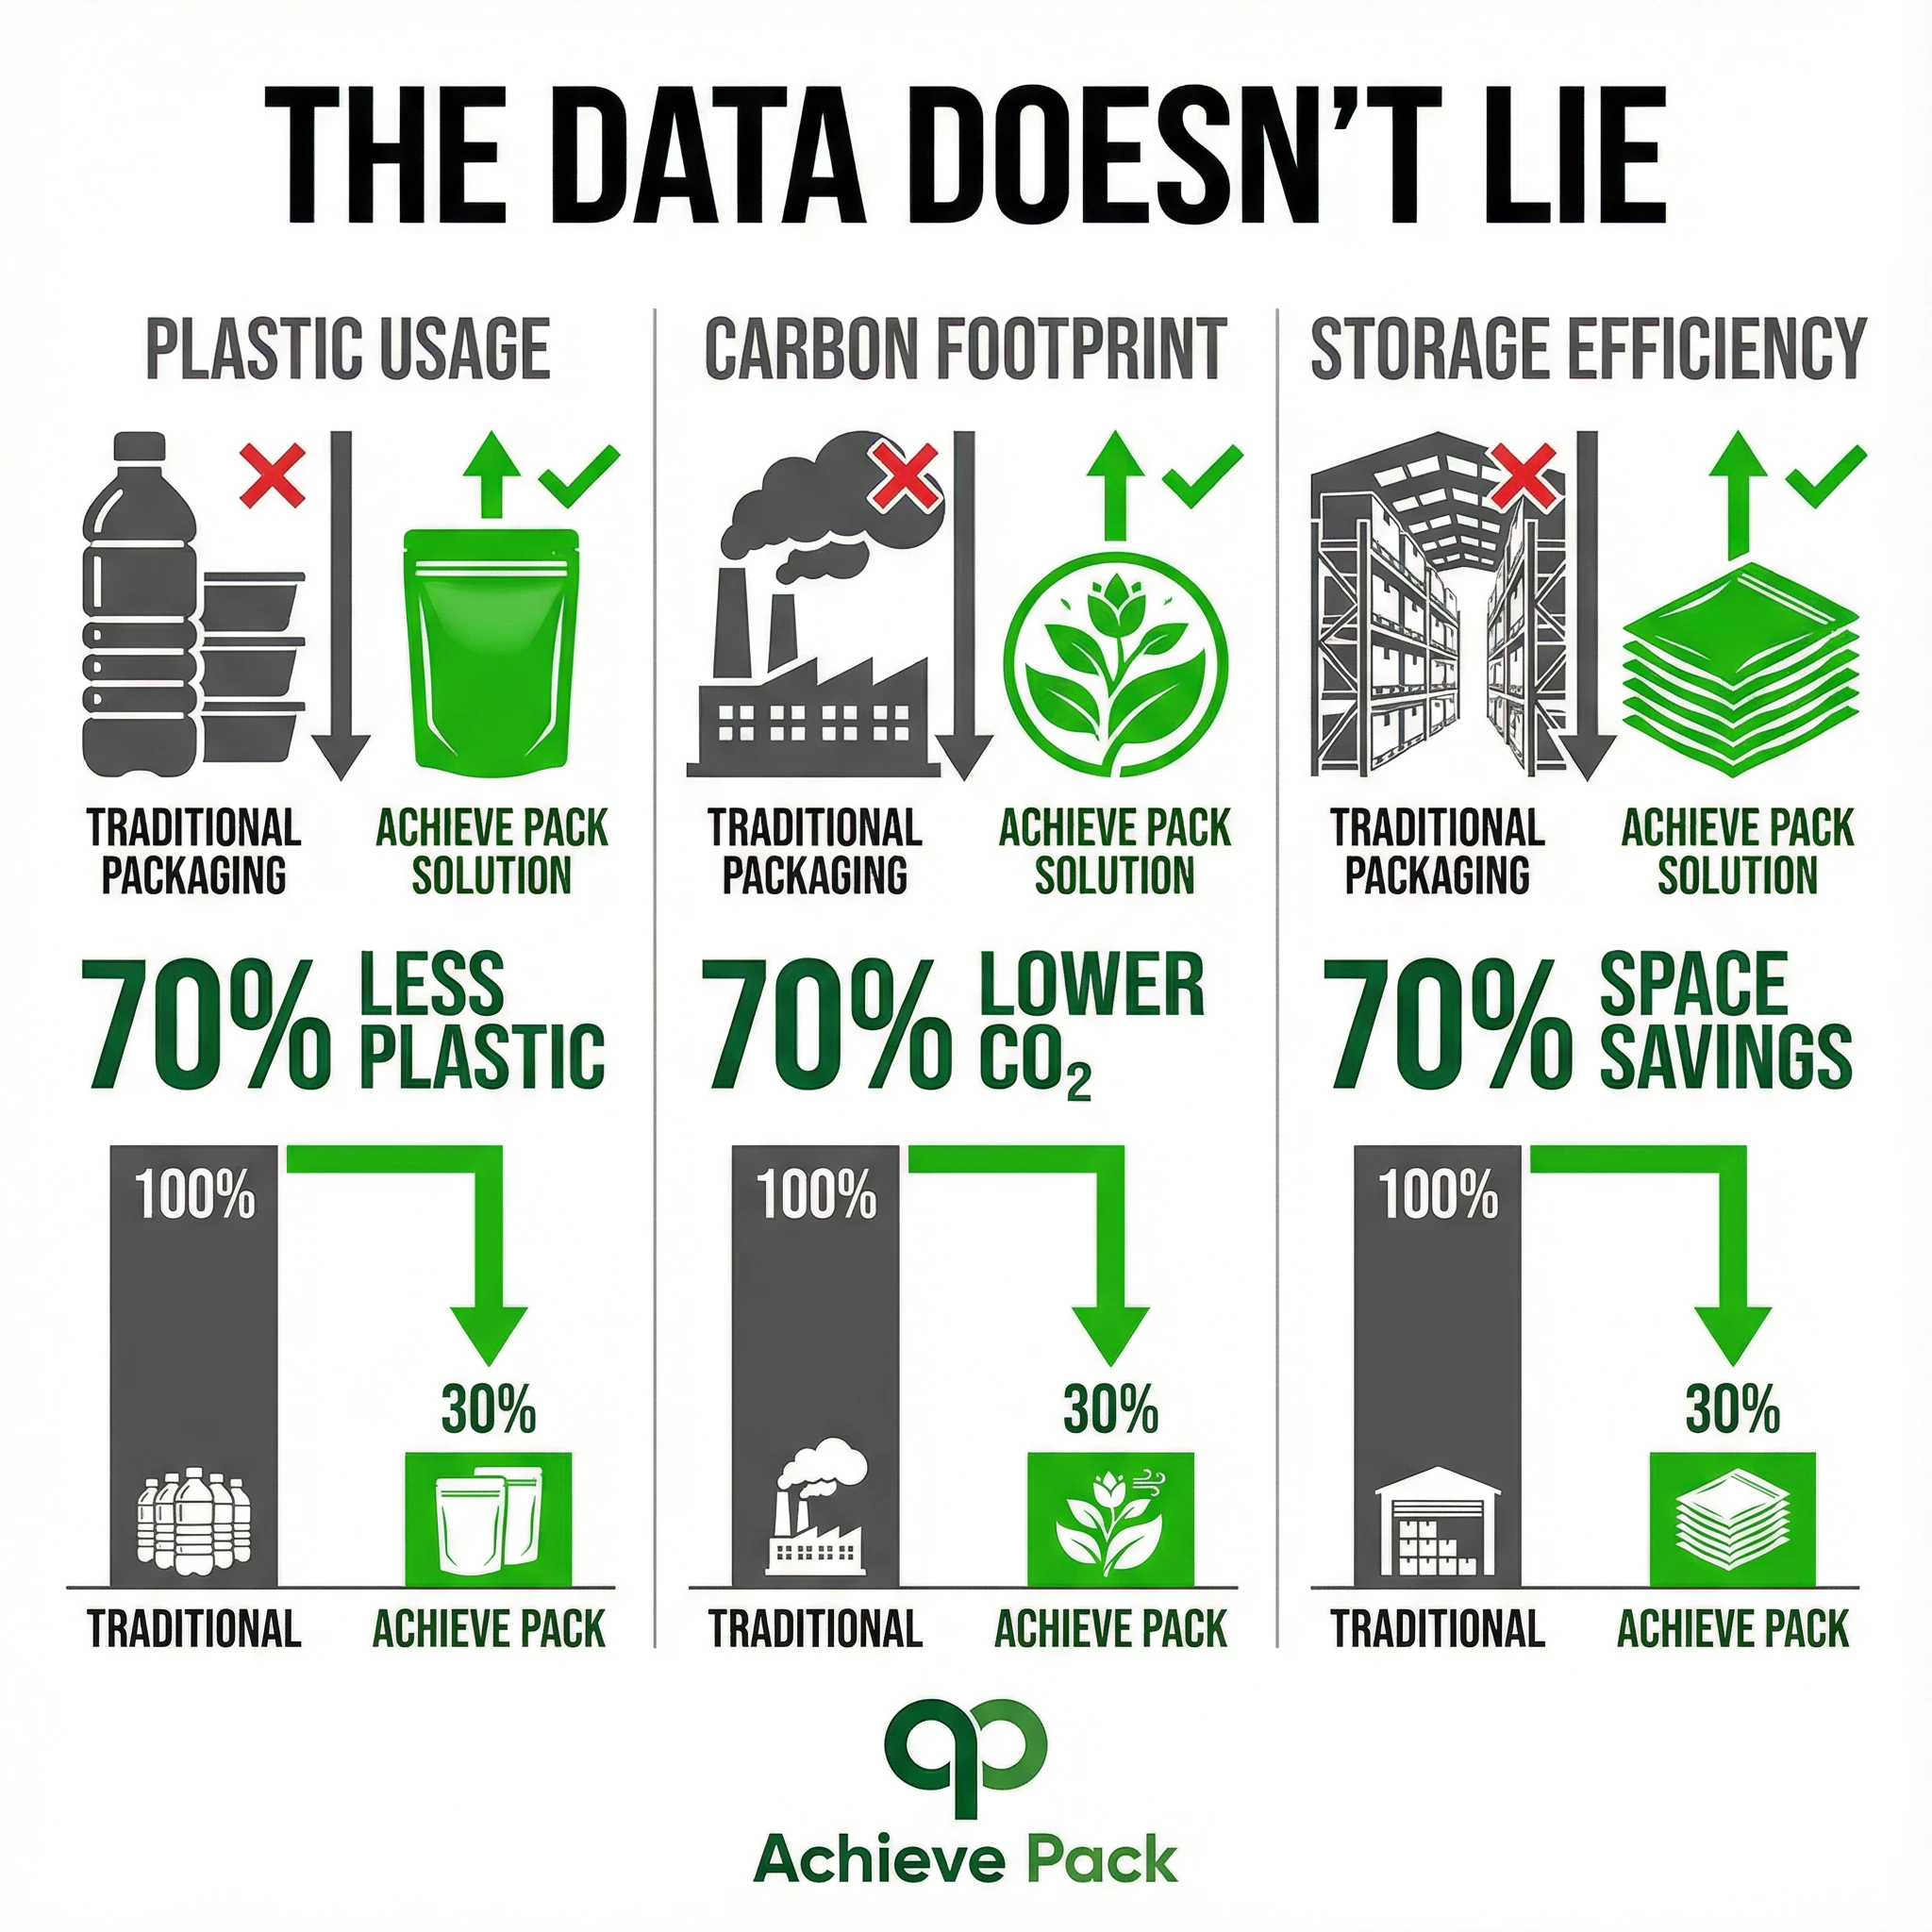
- Heavy Plastic Tax PenaltiesMulti-layer unrecyclable packaging incurs up to €800/ton in EU PPWR fines.
- High MOQs & Plate Cost FrictionTraditional printers force 10,000+ unit minimums and $1,500 cylinder fees.
Achieve Pack / Pouch Eco Solution (After)
Custom engineered multi-layer pouch structure tailored to your exact moisture barrier, seal strength, and aesthetic requirements.
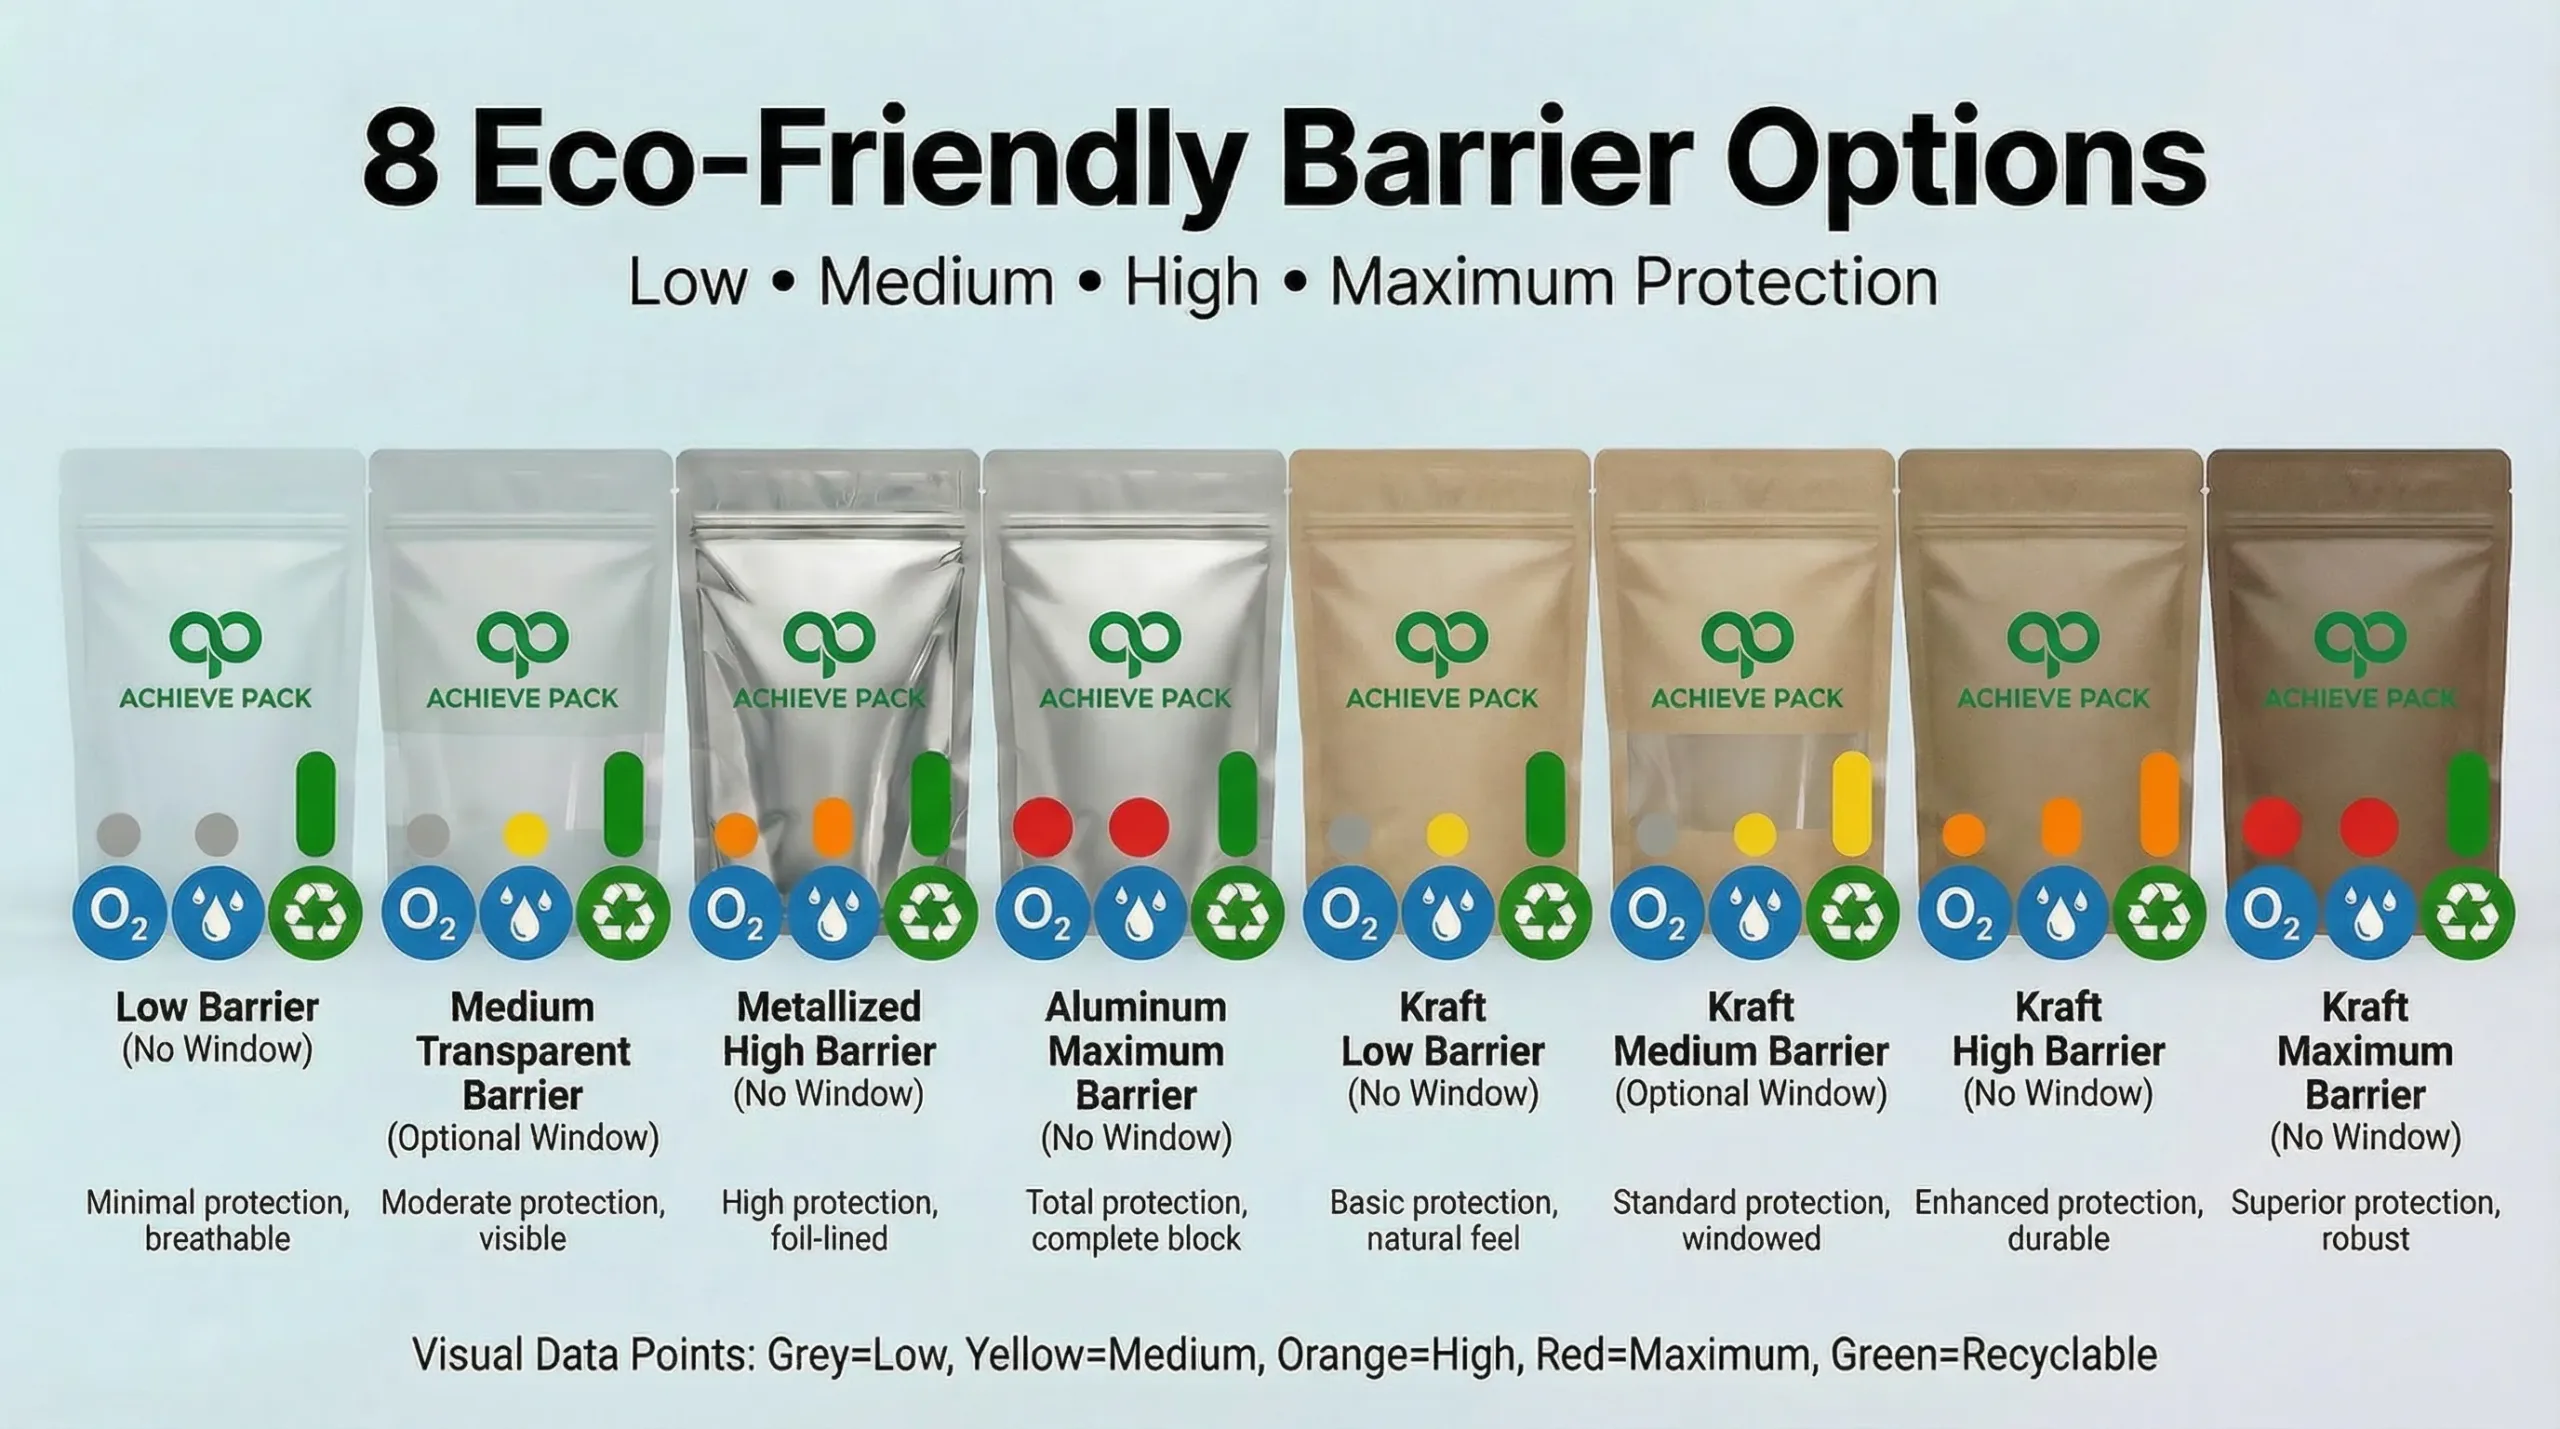
- Ultra High-Barrier Foil/EVOH CoreGuaranteed OTR < 0.1 cc/m²/day, keeping contents fresh for 18–24 months.
- Reinforced 45N/15mm Localized Heat Seal180°C precision seam dwell time prevents bursting even under 2-meter drops.
- 100% Certified Eco ComplianceTÜV OK Compost HOME (EN13432) & Mono-PE Recyclable structures (0% Tax).
- HD Digital Printing with 500-Unit Low MOQsPrint multi-SKU runs in 7 business days with zero setup plate charges.
Questions We Get Asked
Can flexible packaging protect chocolate in hot climates?▼
Is foil stamping sustainable?▼
Related Stuff
How We Ensure Absolute Accuracy and Trustworthiness
At Achieve Pack, sustainable packaging isn't just about printing; it's about hands-on material science. This article has been written and verified by Ryan Wong, a packaging specialist with 14+ years of experience engineering biopolymer stacks for DTC startups and Fortune 500 companies.
All research, material barrier specifications (OTR, WVTR), heat-seal values (N/15mm), and compostability timelines cited in our guides are backed by testing inside the Achieve Pack Materials Testing Lab. We cross-reference our data with official certification registries from BPI (Biodegradable Products Institute), TÜV Austria (OK Compost HOME), and FSC (Forest Stewardship Council).
Ryan Wong
Supply Chain Director
B.Eng honors degree graduate from Hong Kong Polytechnic University. Serving brands in 8 countries.
View Expert Profile →Shipping Premium Chocolate Into Hot Markets?
Tell us your distribution route and temperature exposure. We'll spec a barrier structure that protects the product—and tell you honestly where packaging ends and cold chain begins.
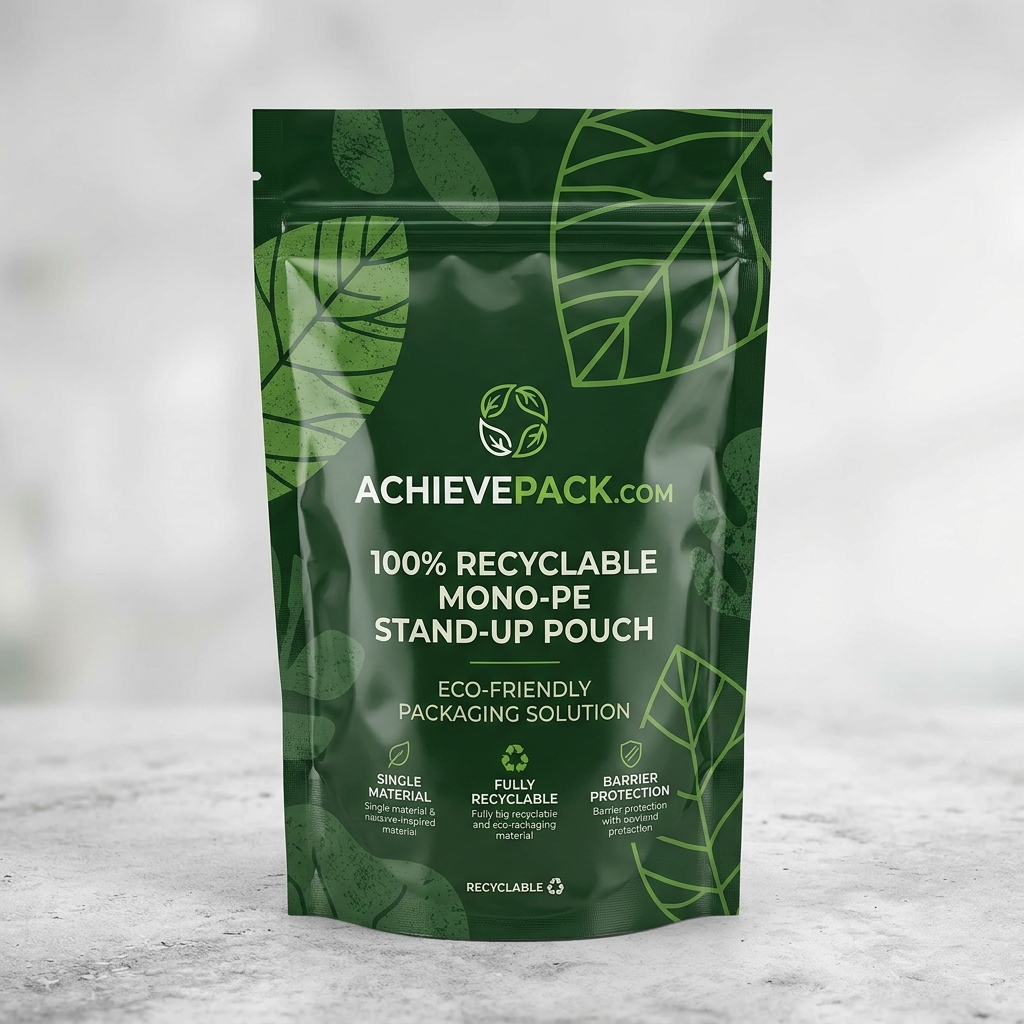
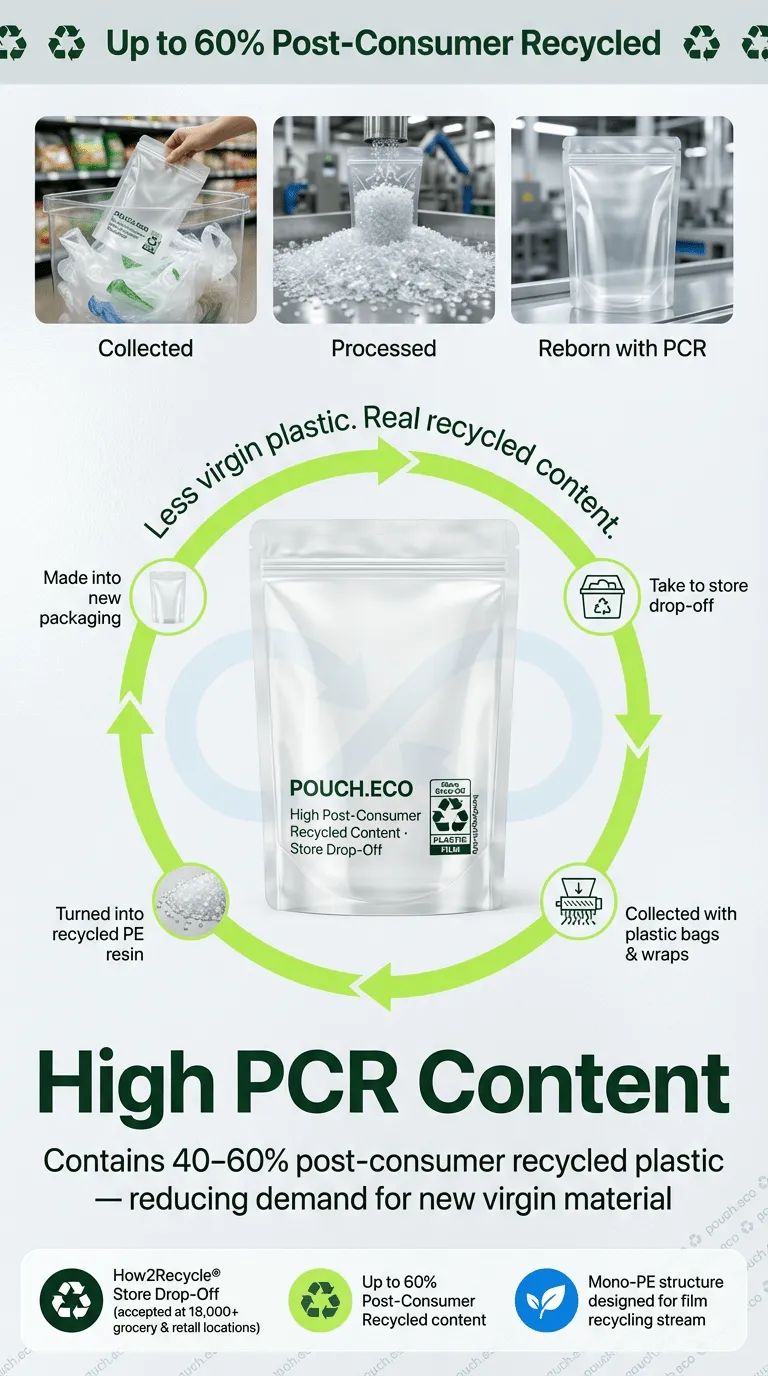
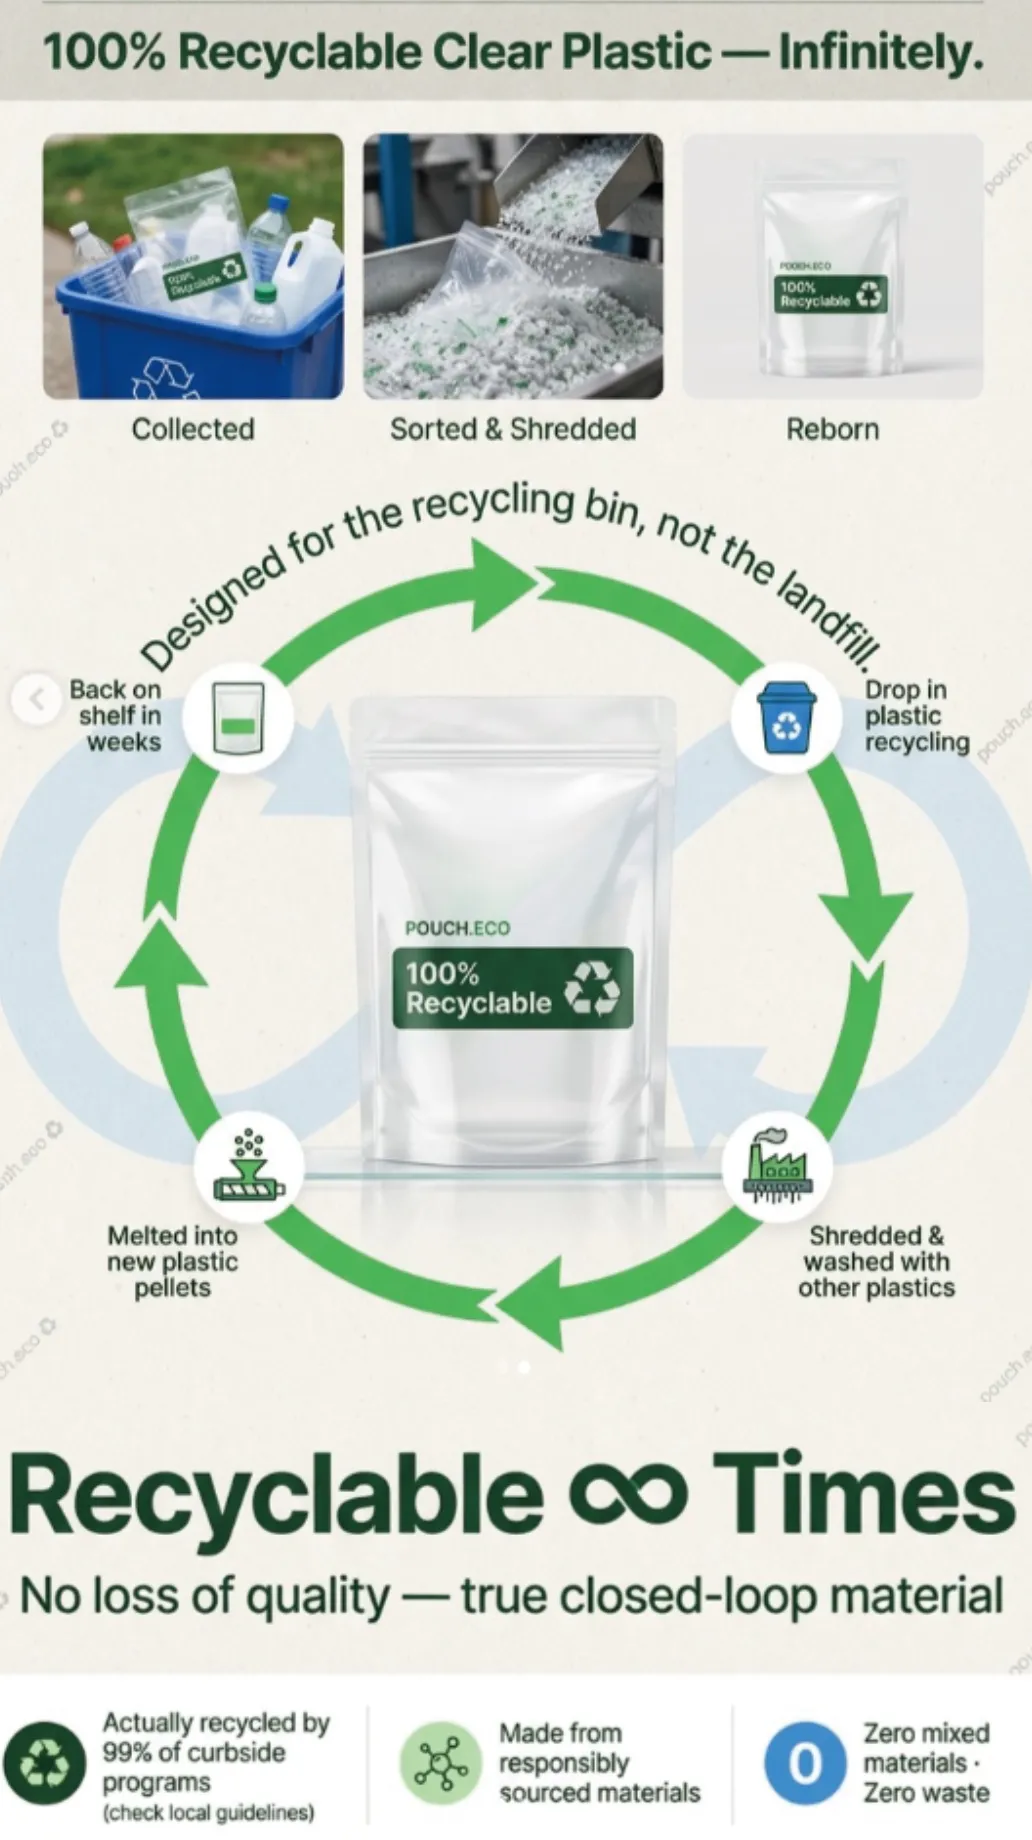
Recyclable Mono-Material
Engineered using Mono-PE or Mono-PP structures to enable simple, circular sorting and recycling. Combined with specialized high-barrier coatings to preserve freshness without compromising recyclability.
- 100% recyclable mono-polymer structure
- Meets EU Circular Economy directives
- EVOH barrier layer for oxygen protection
- Highly customizable surface finishes