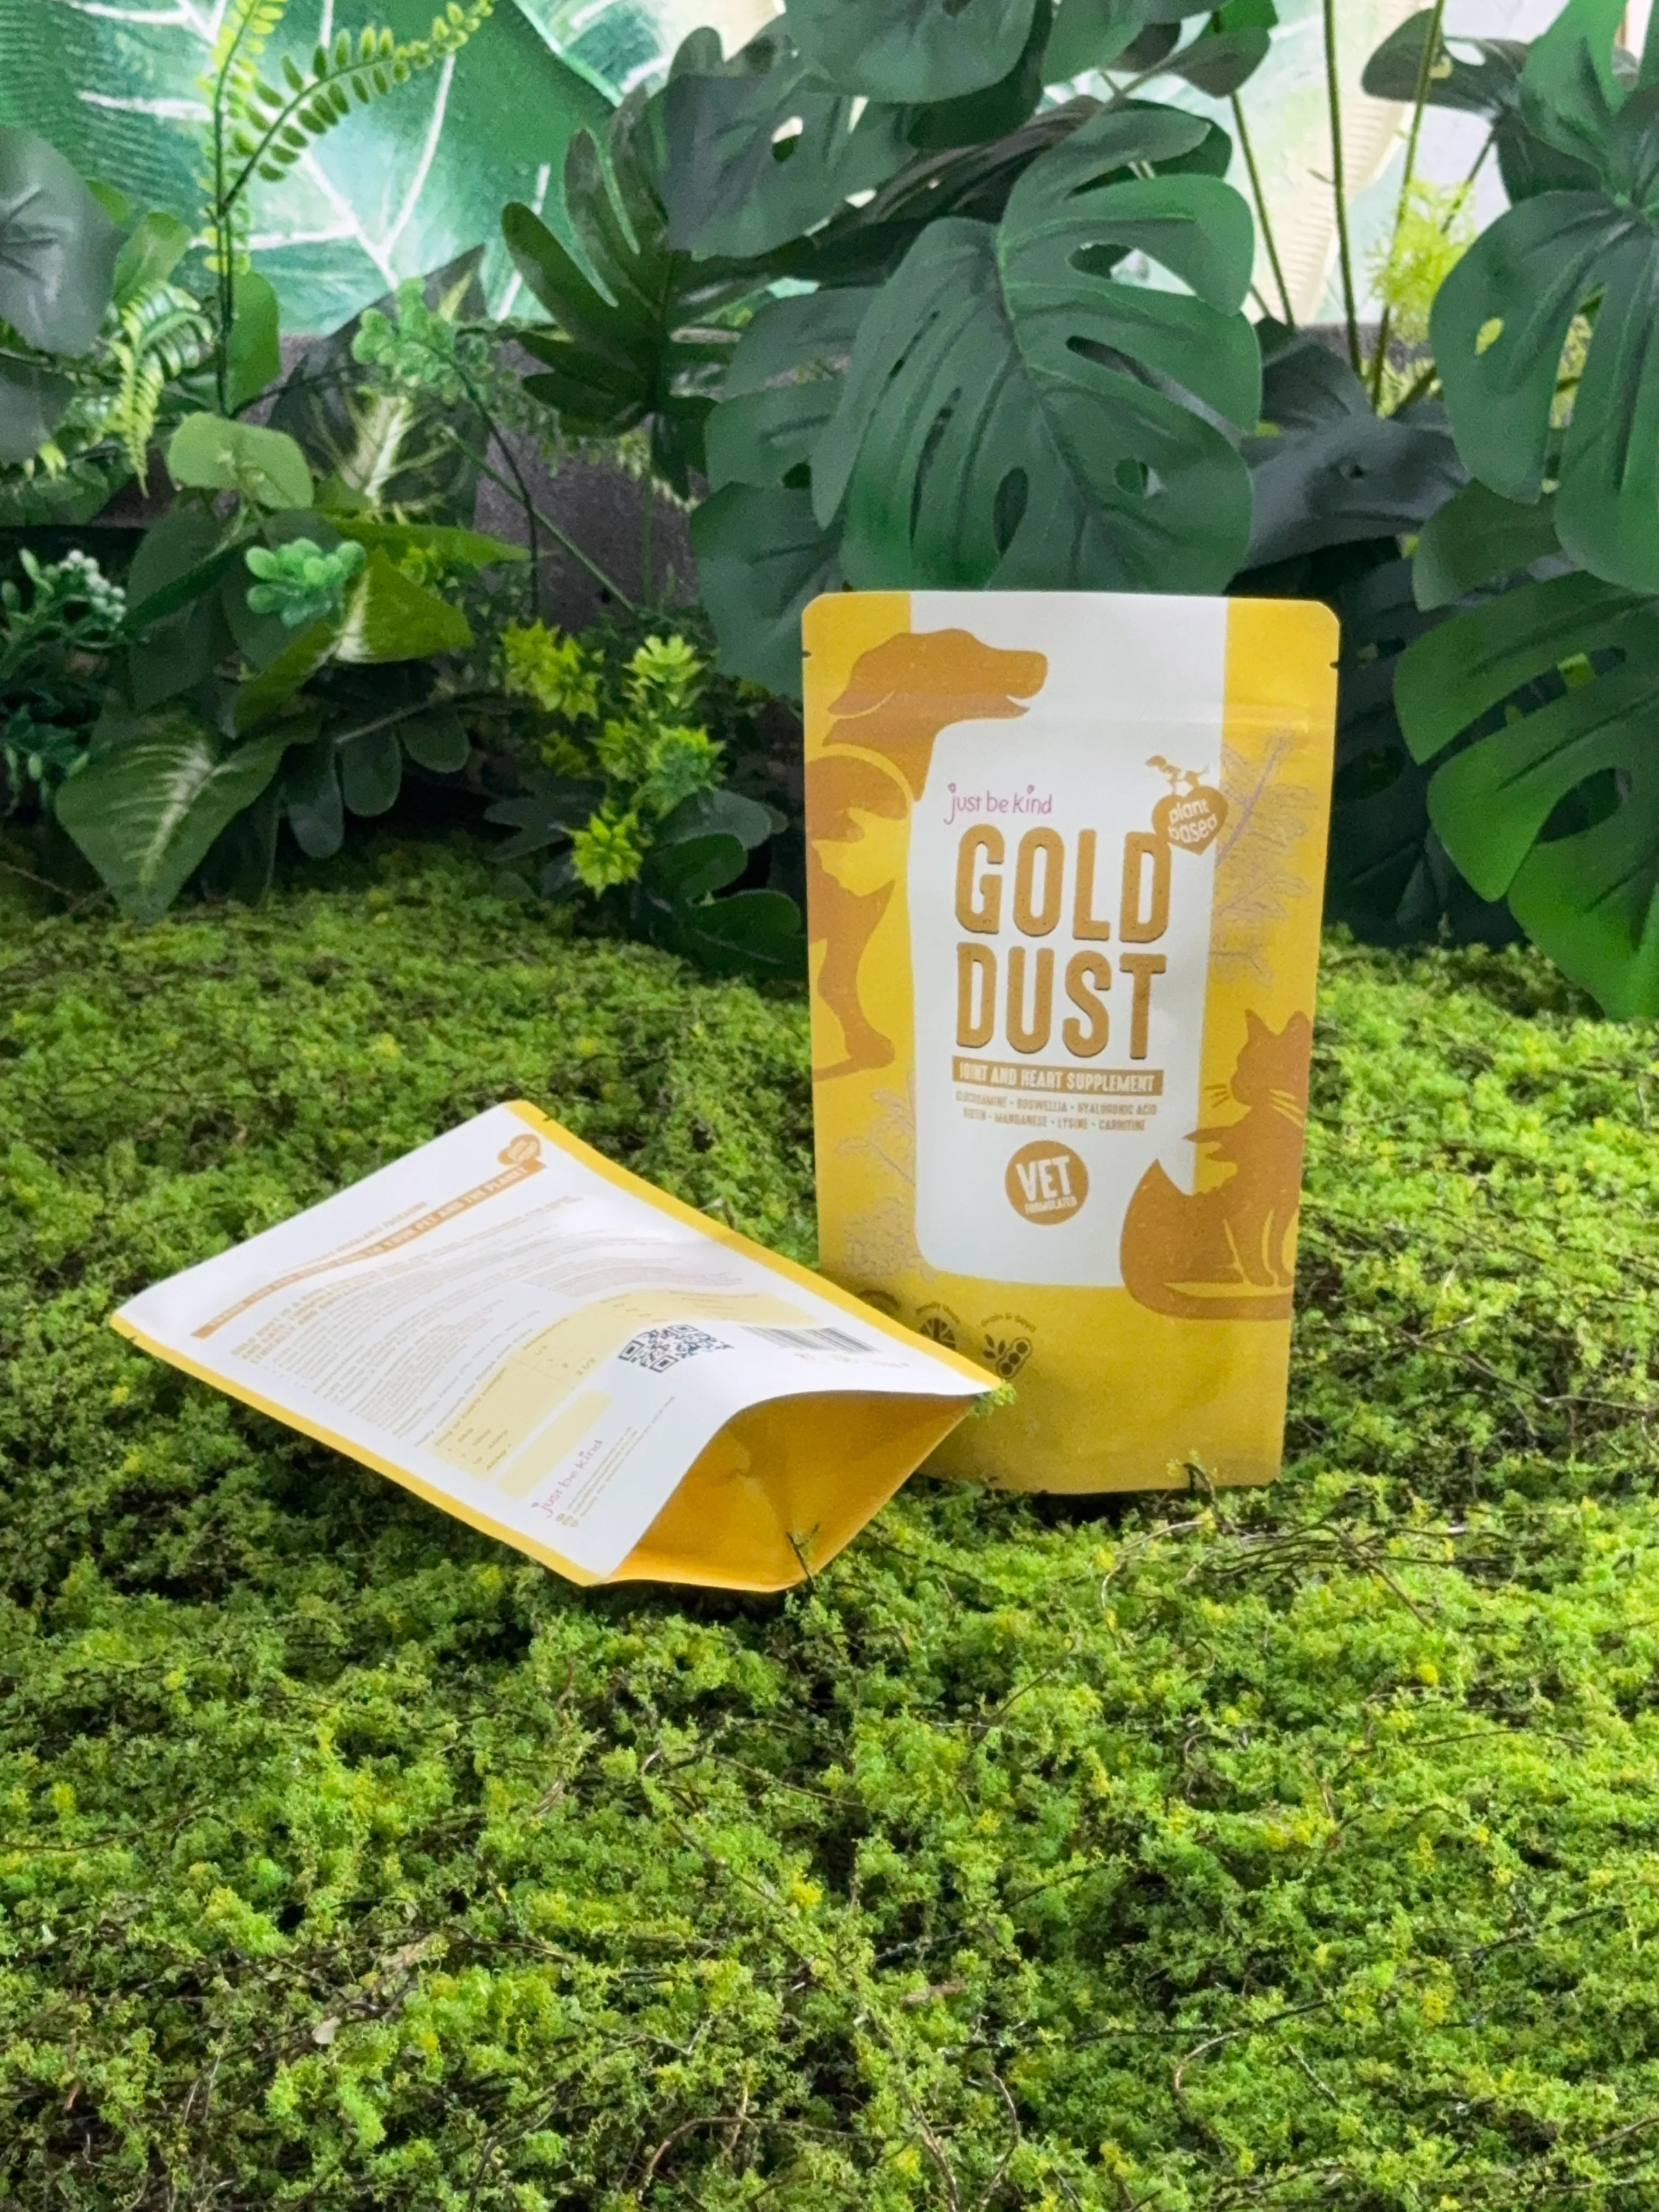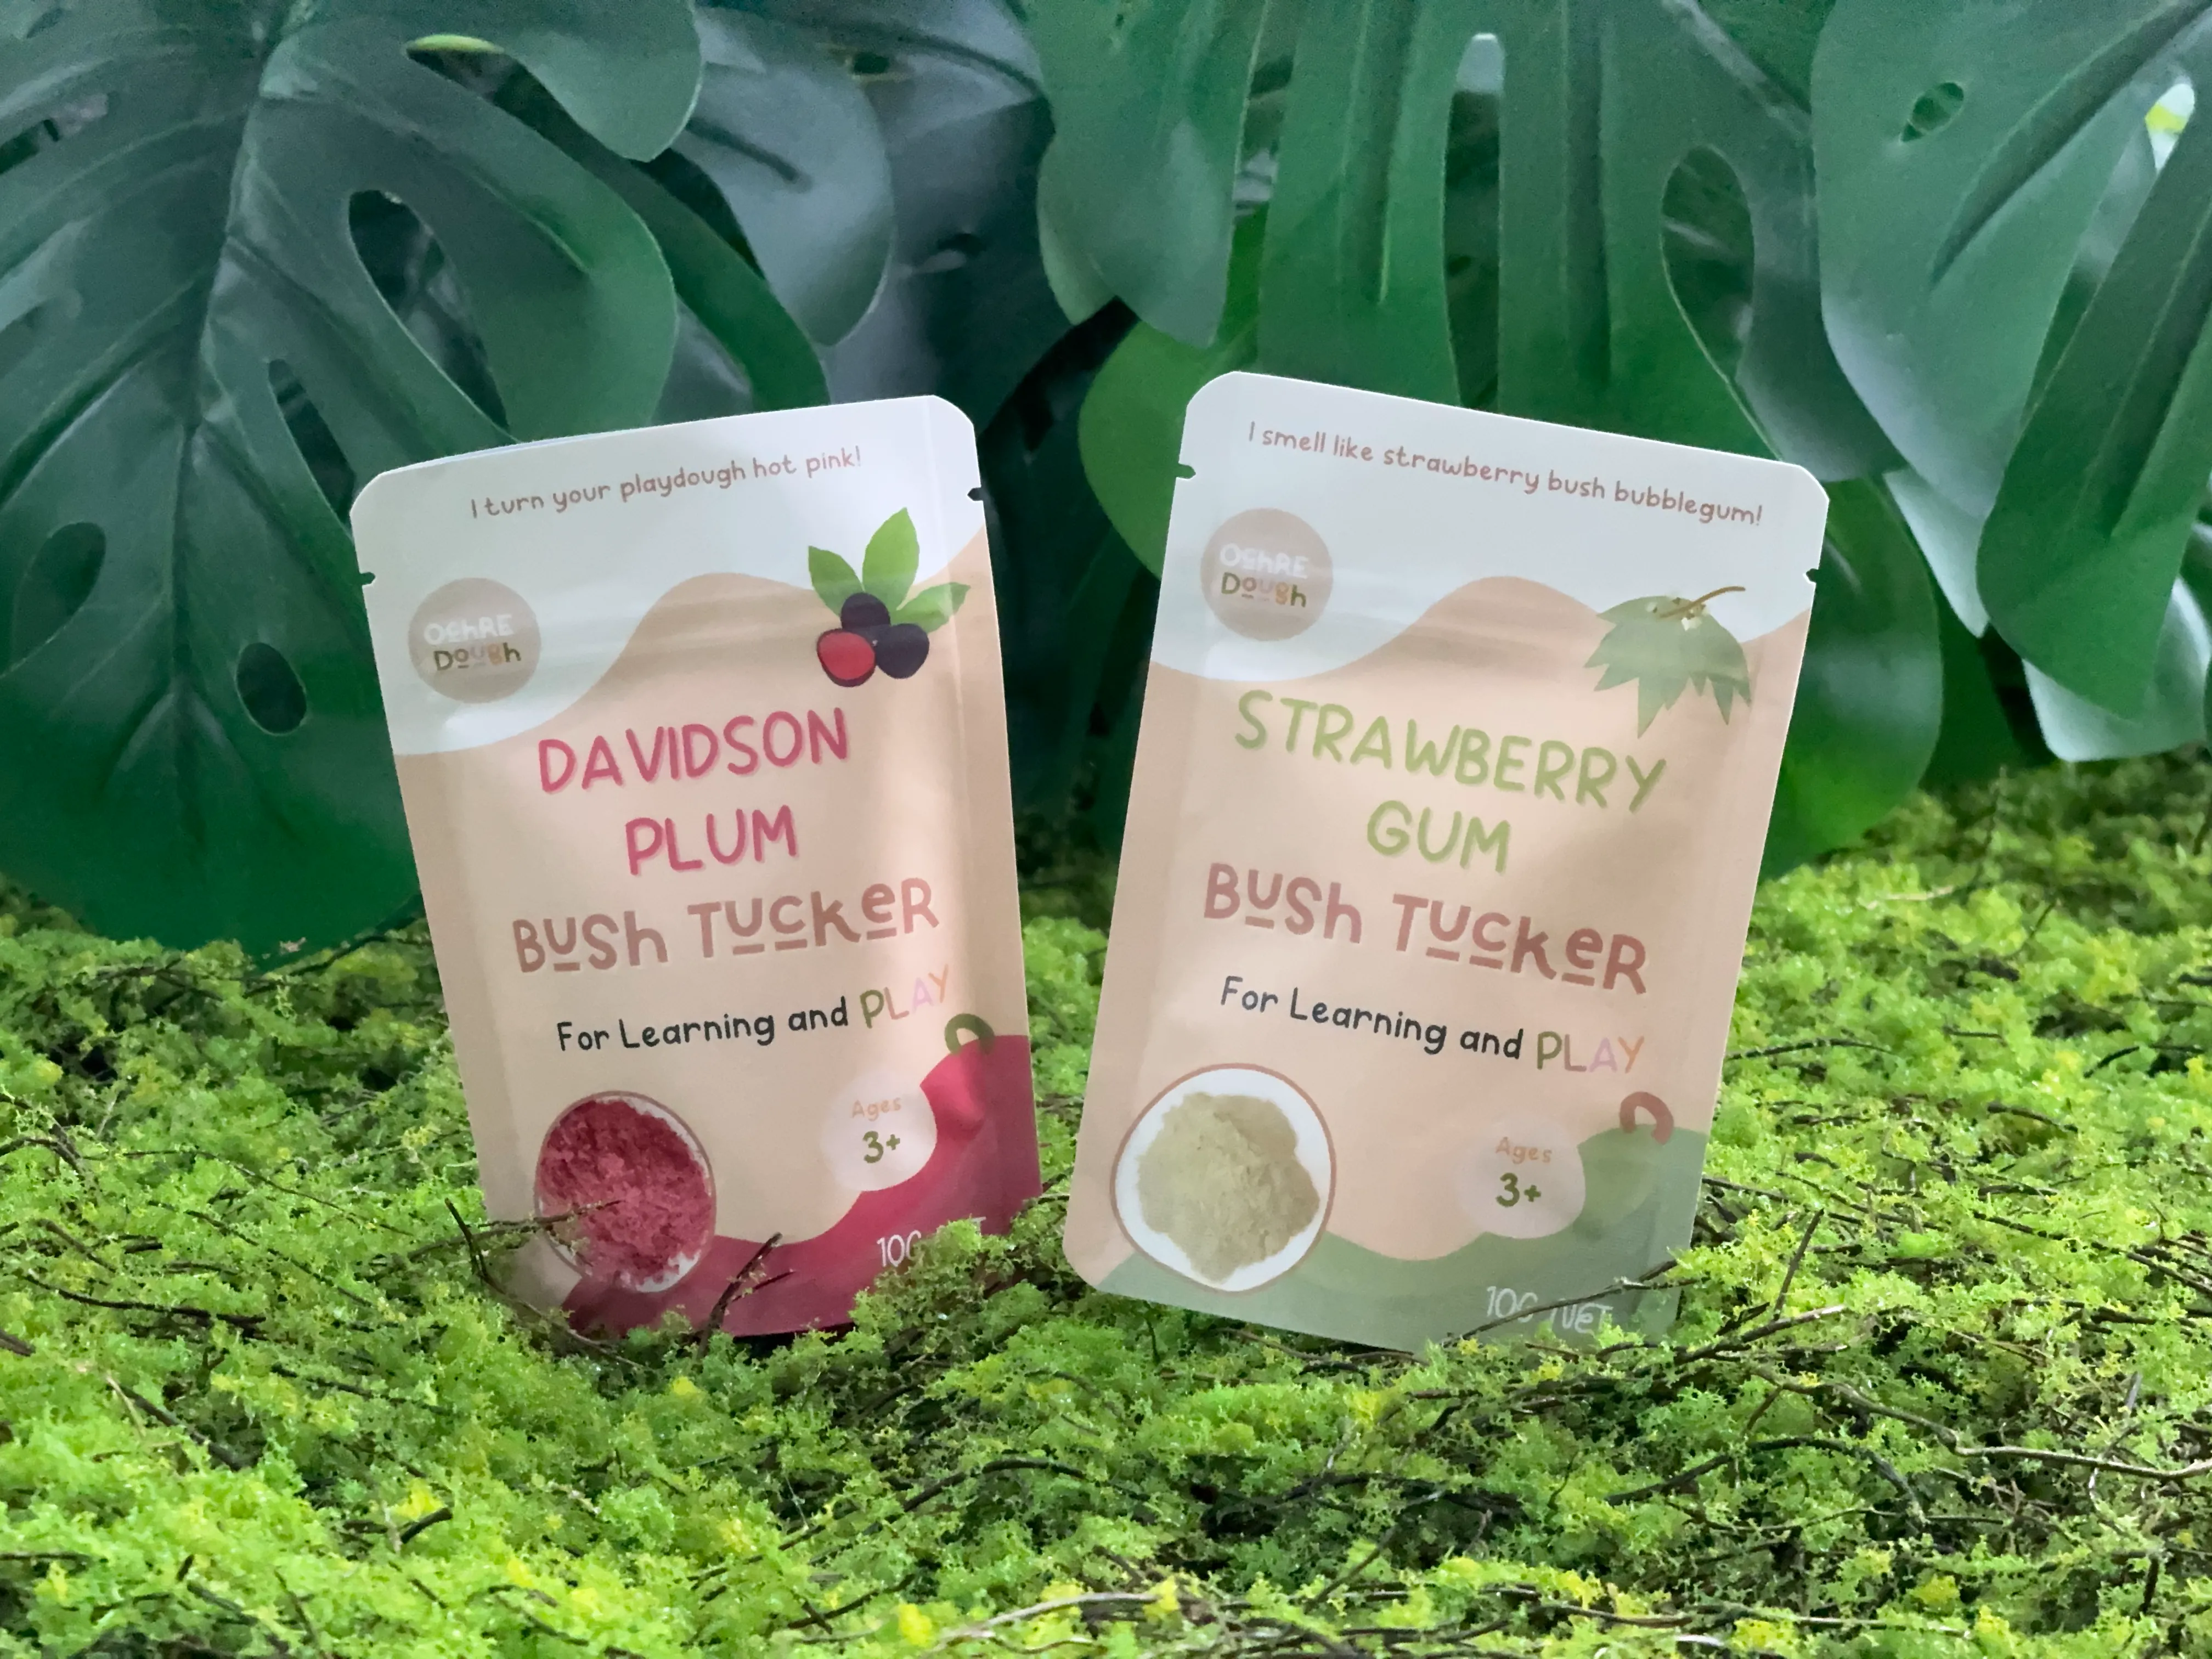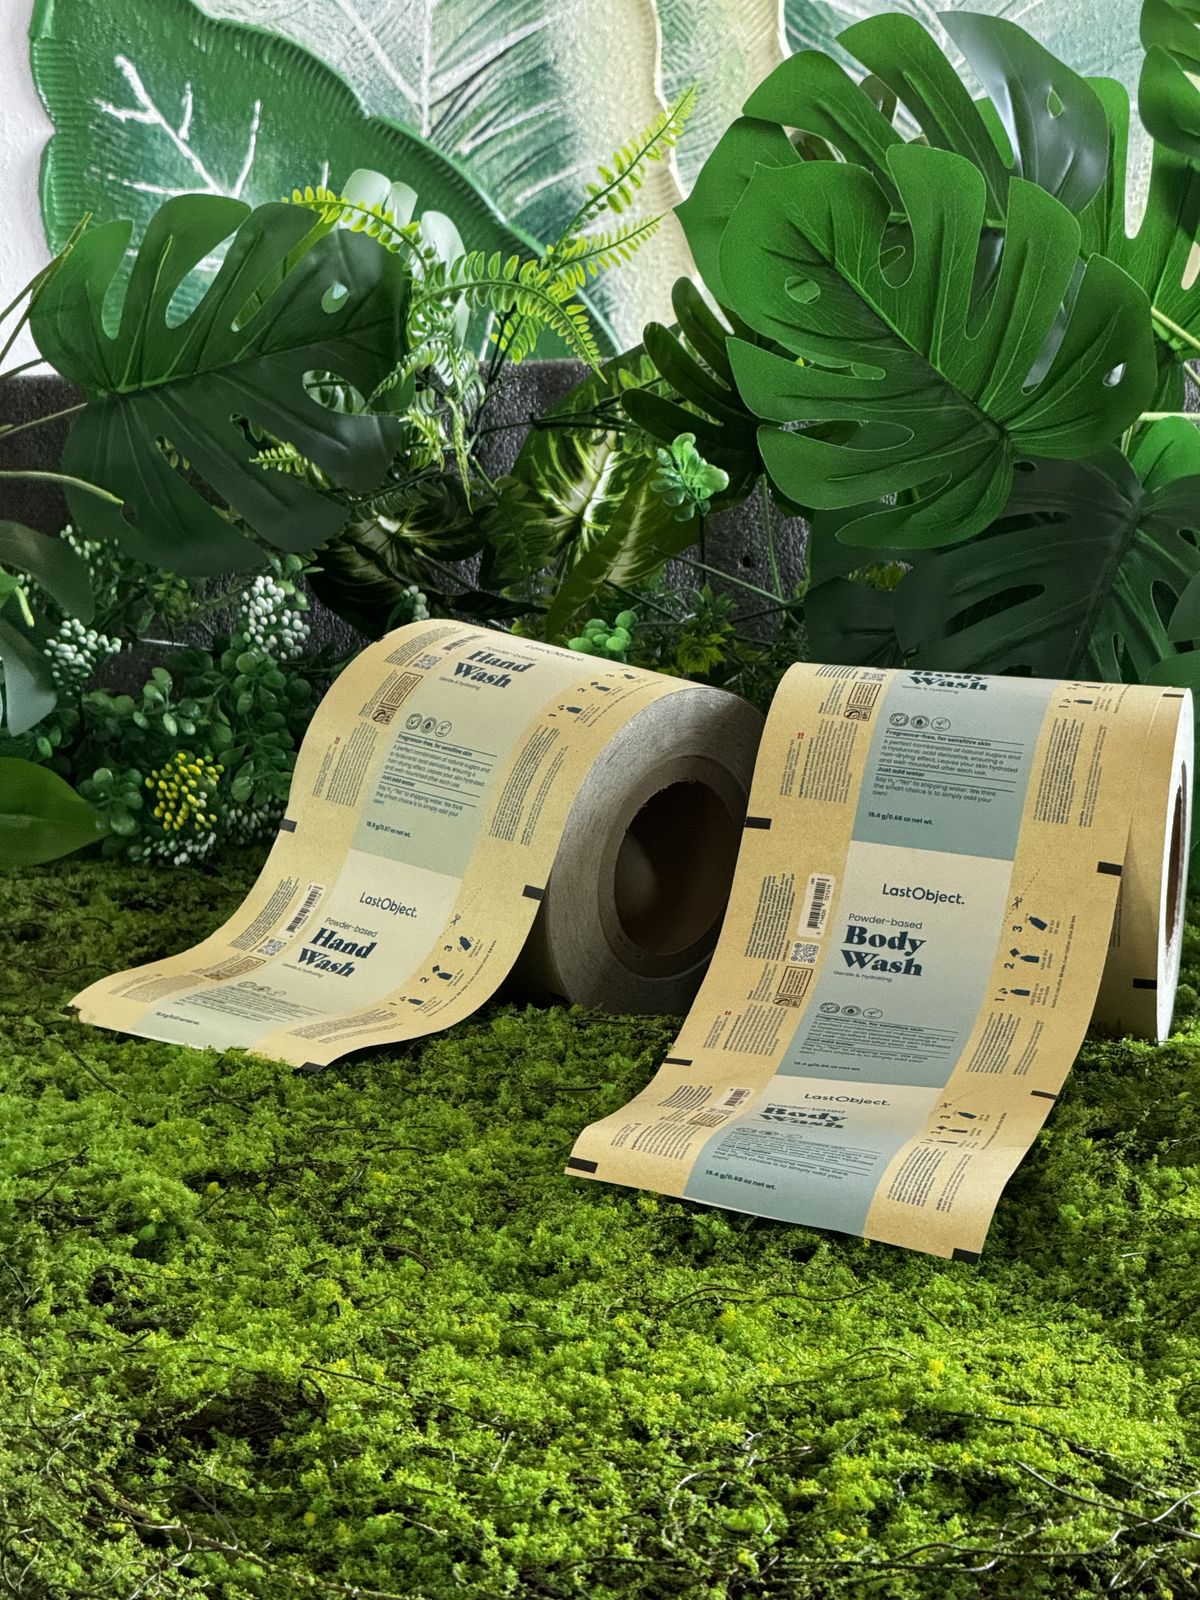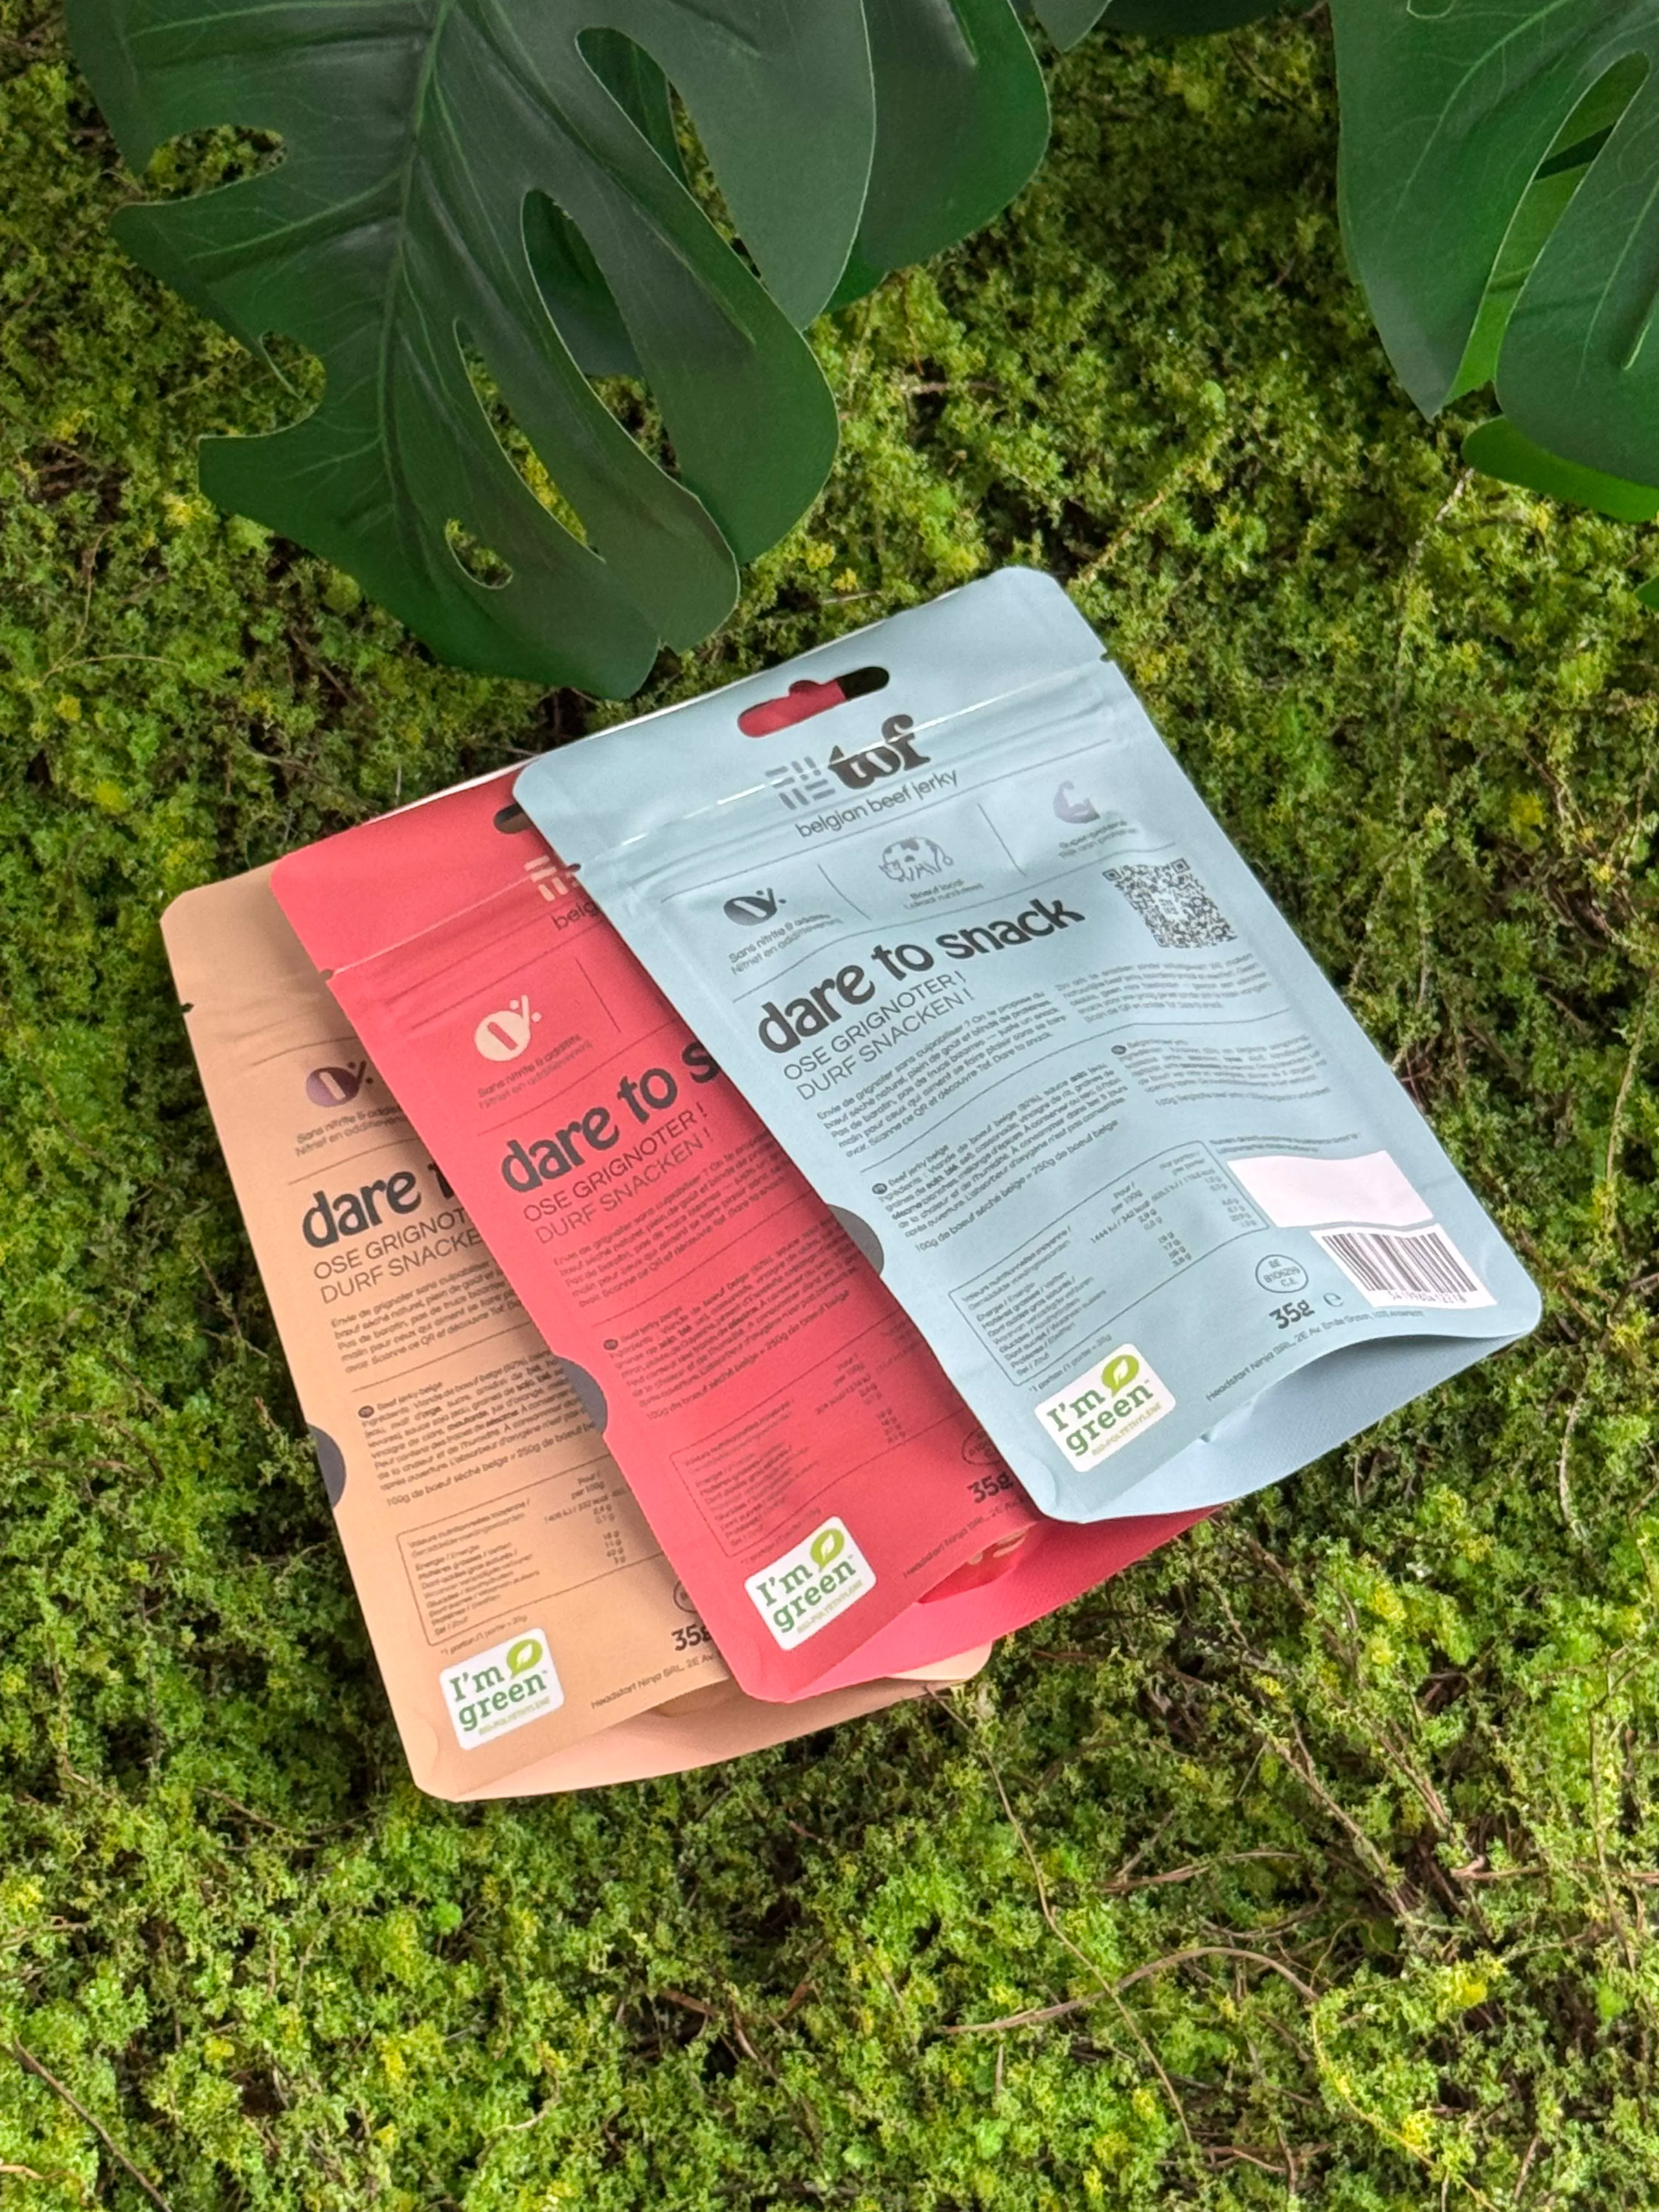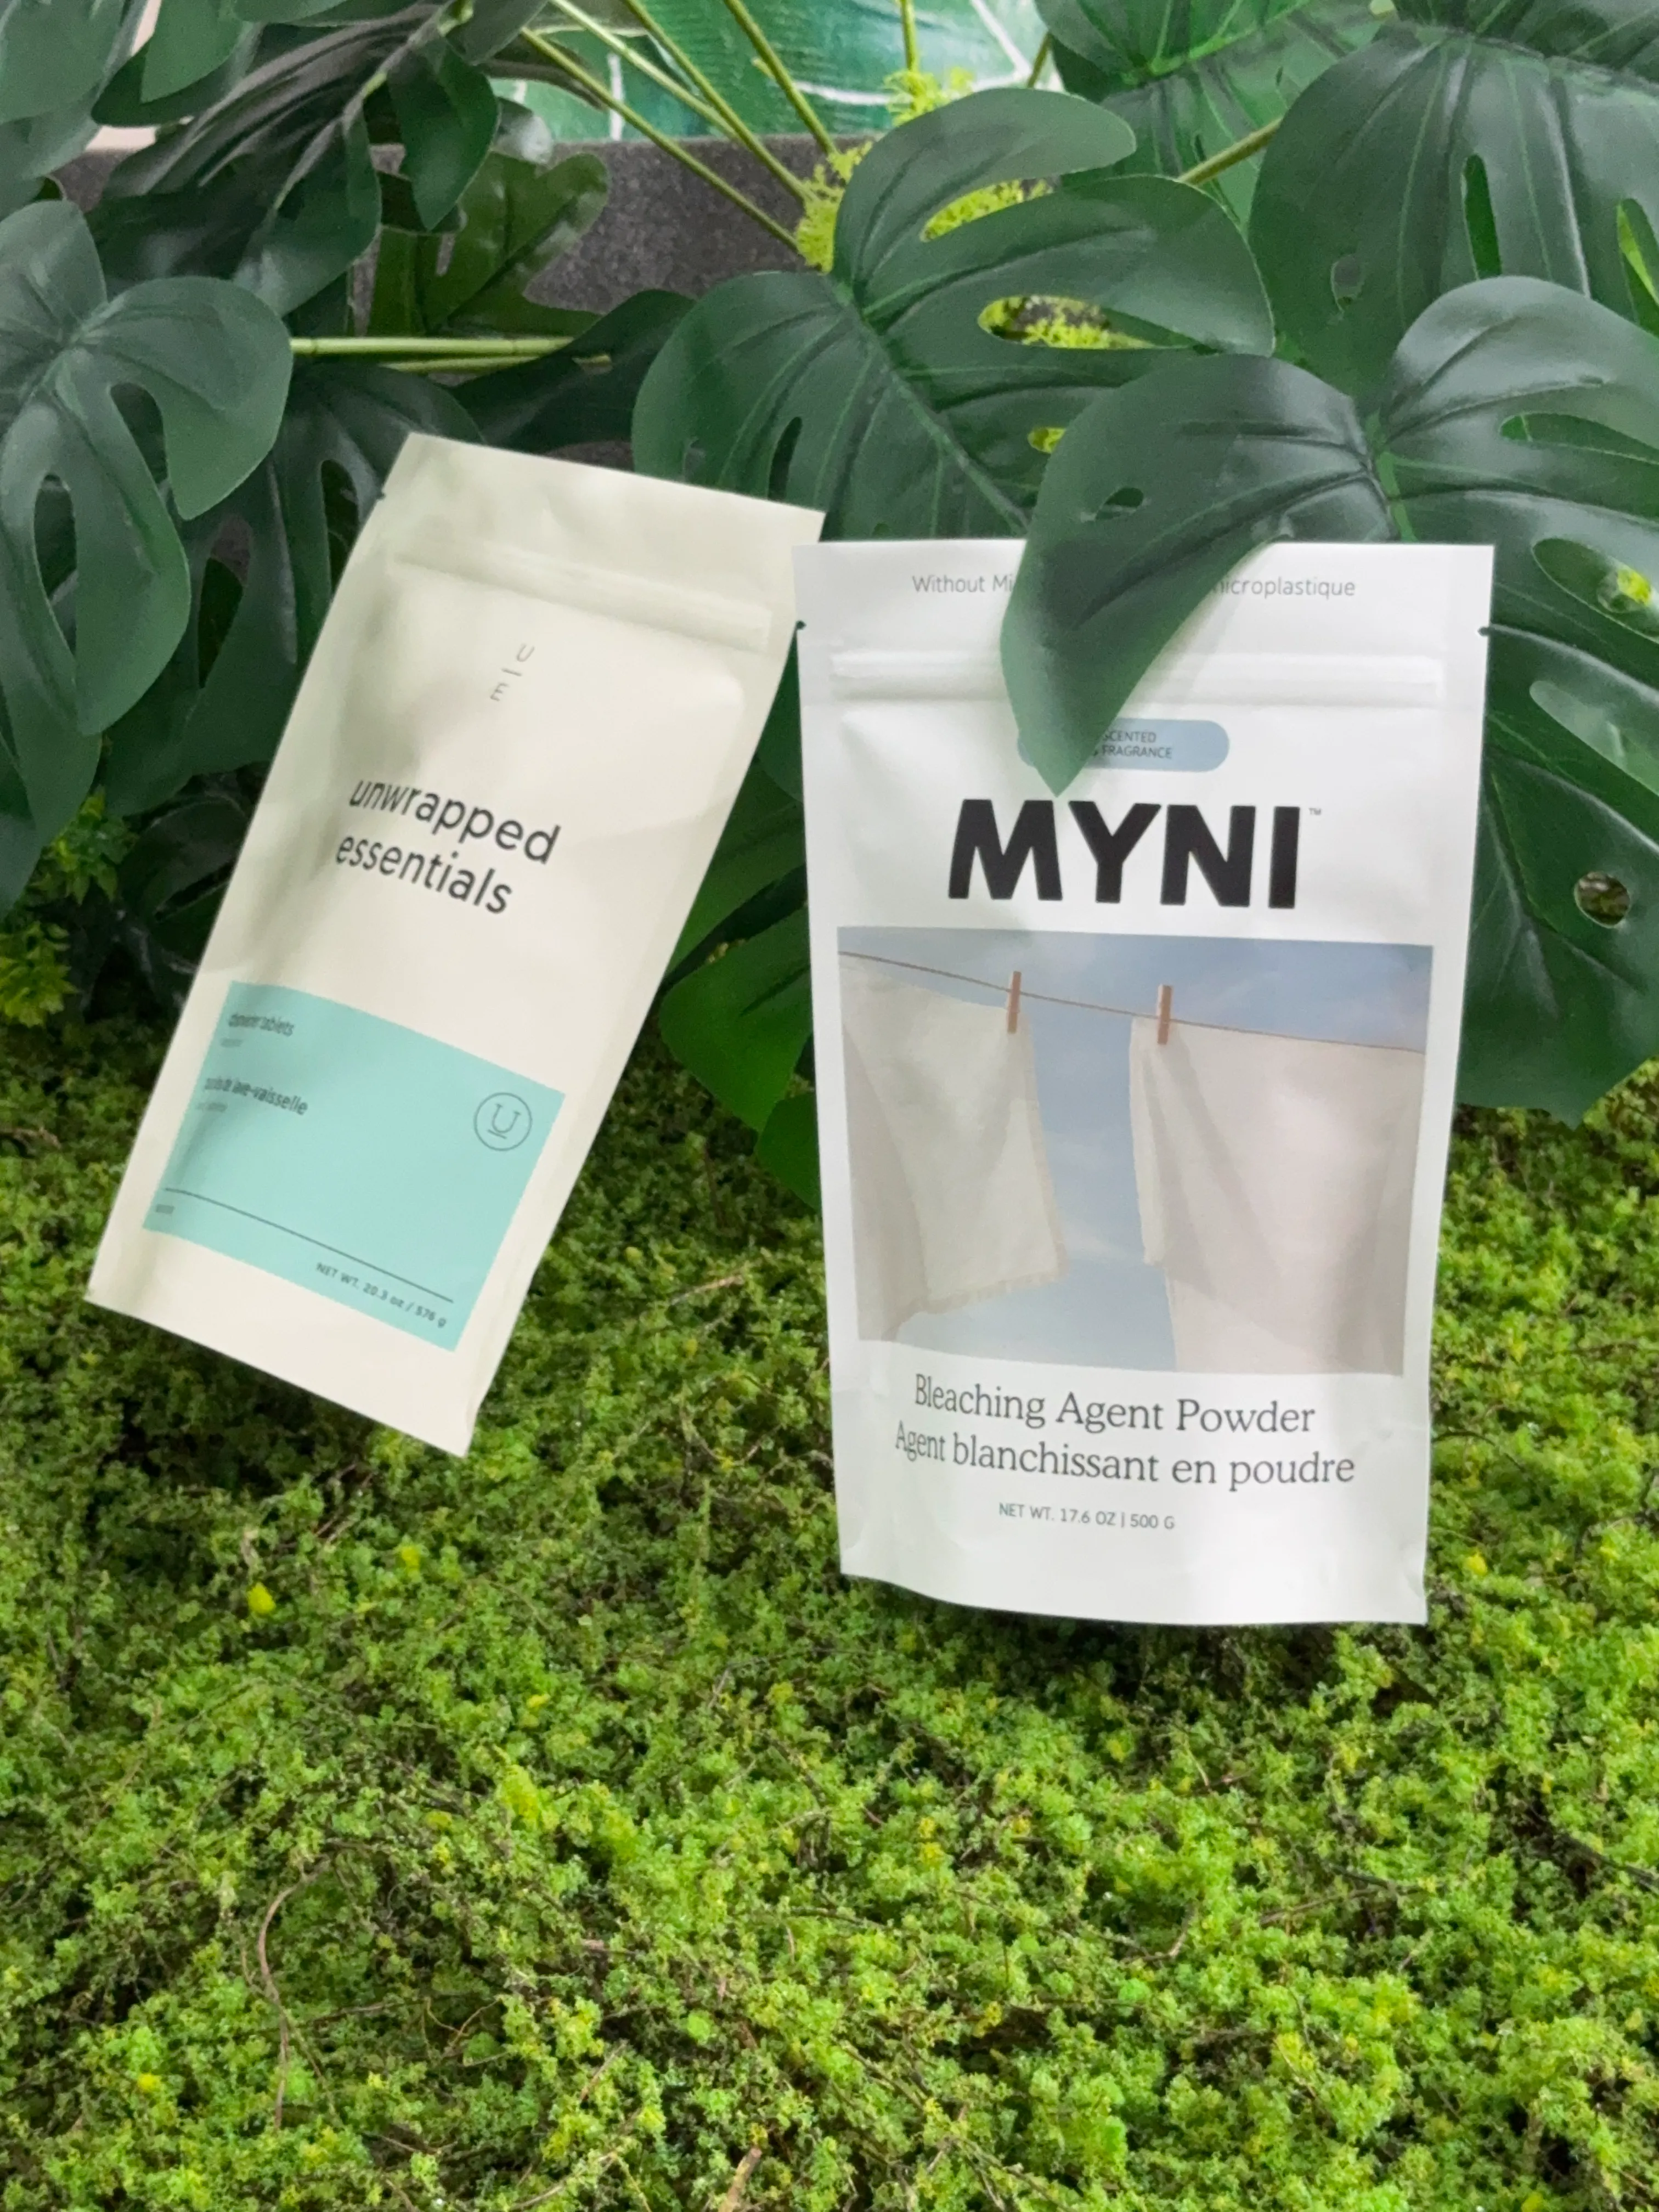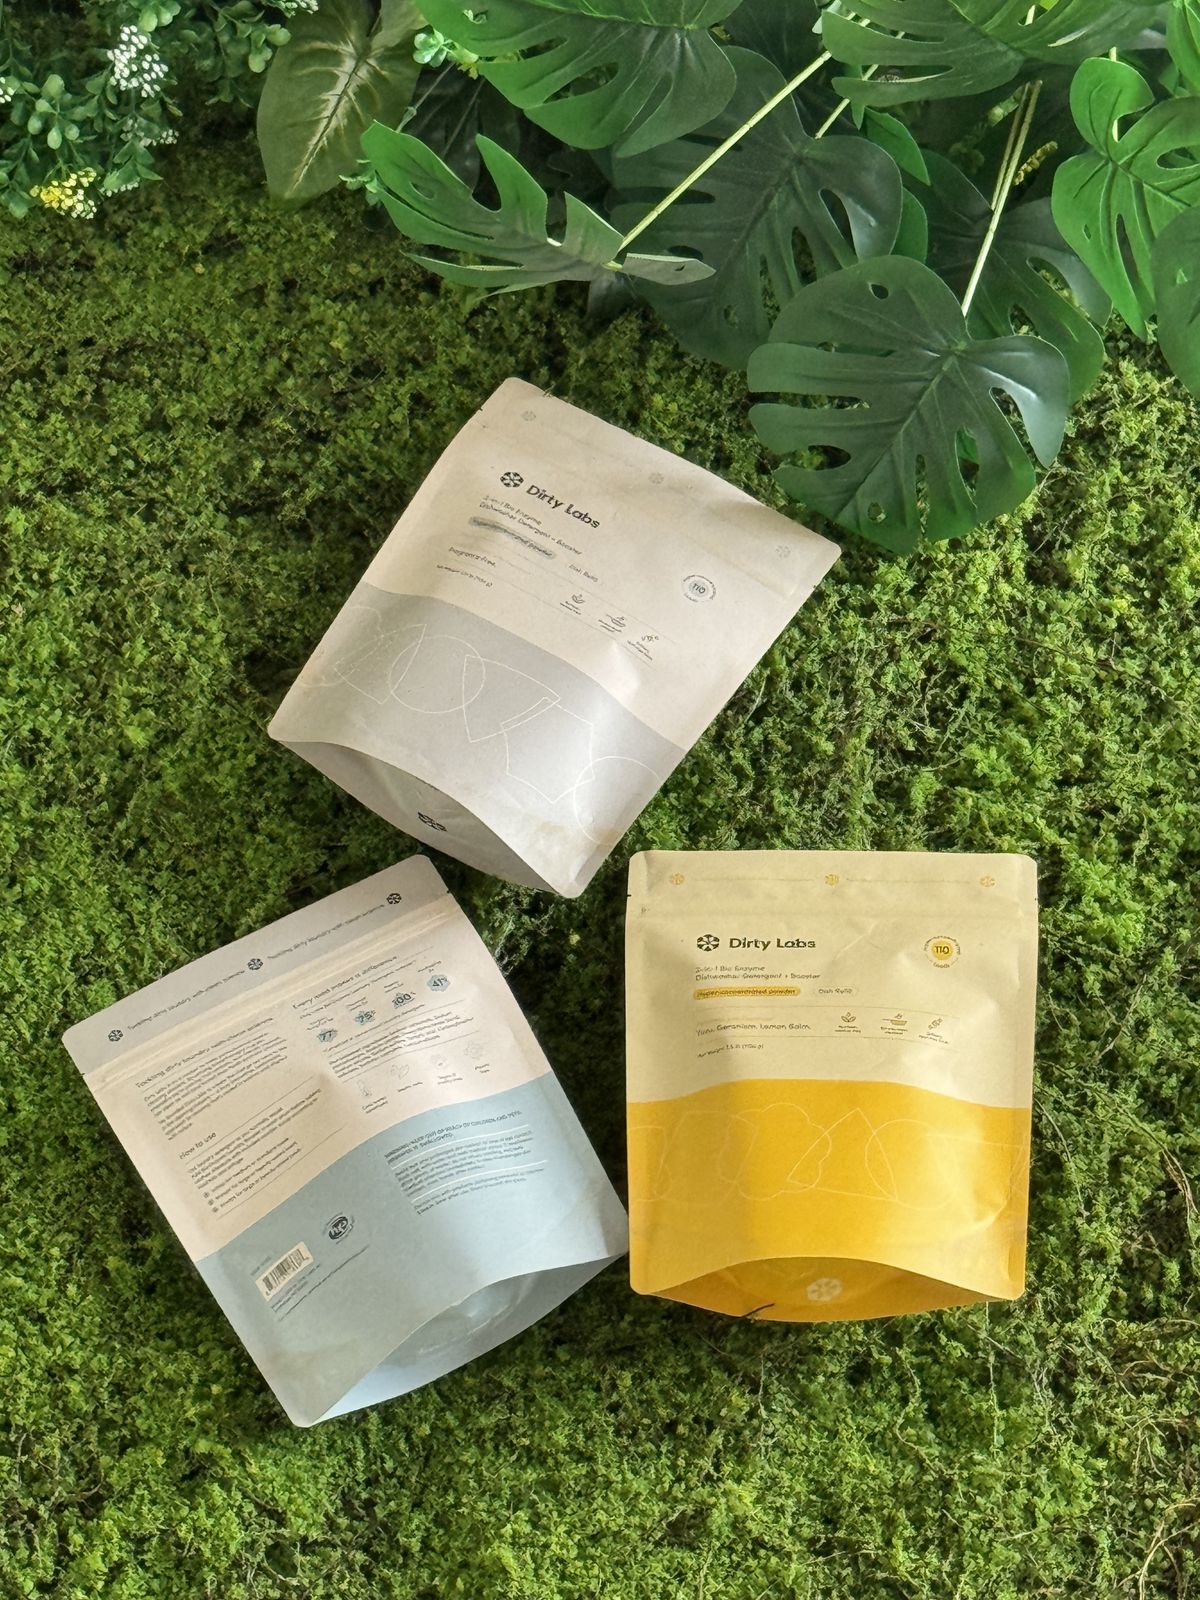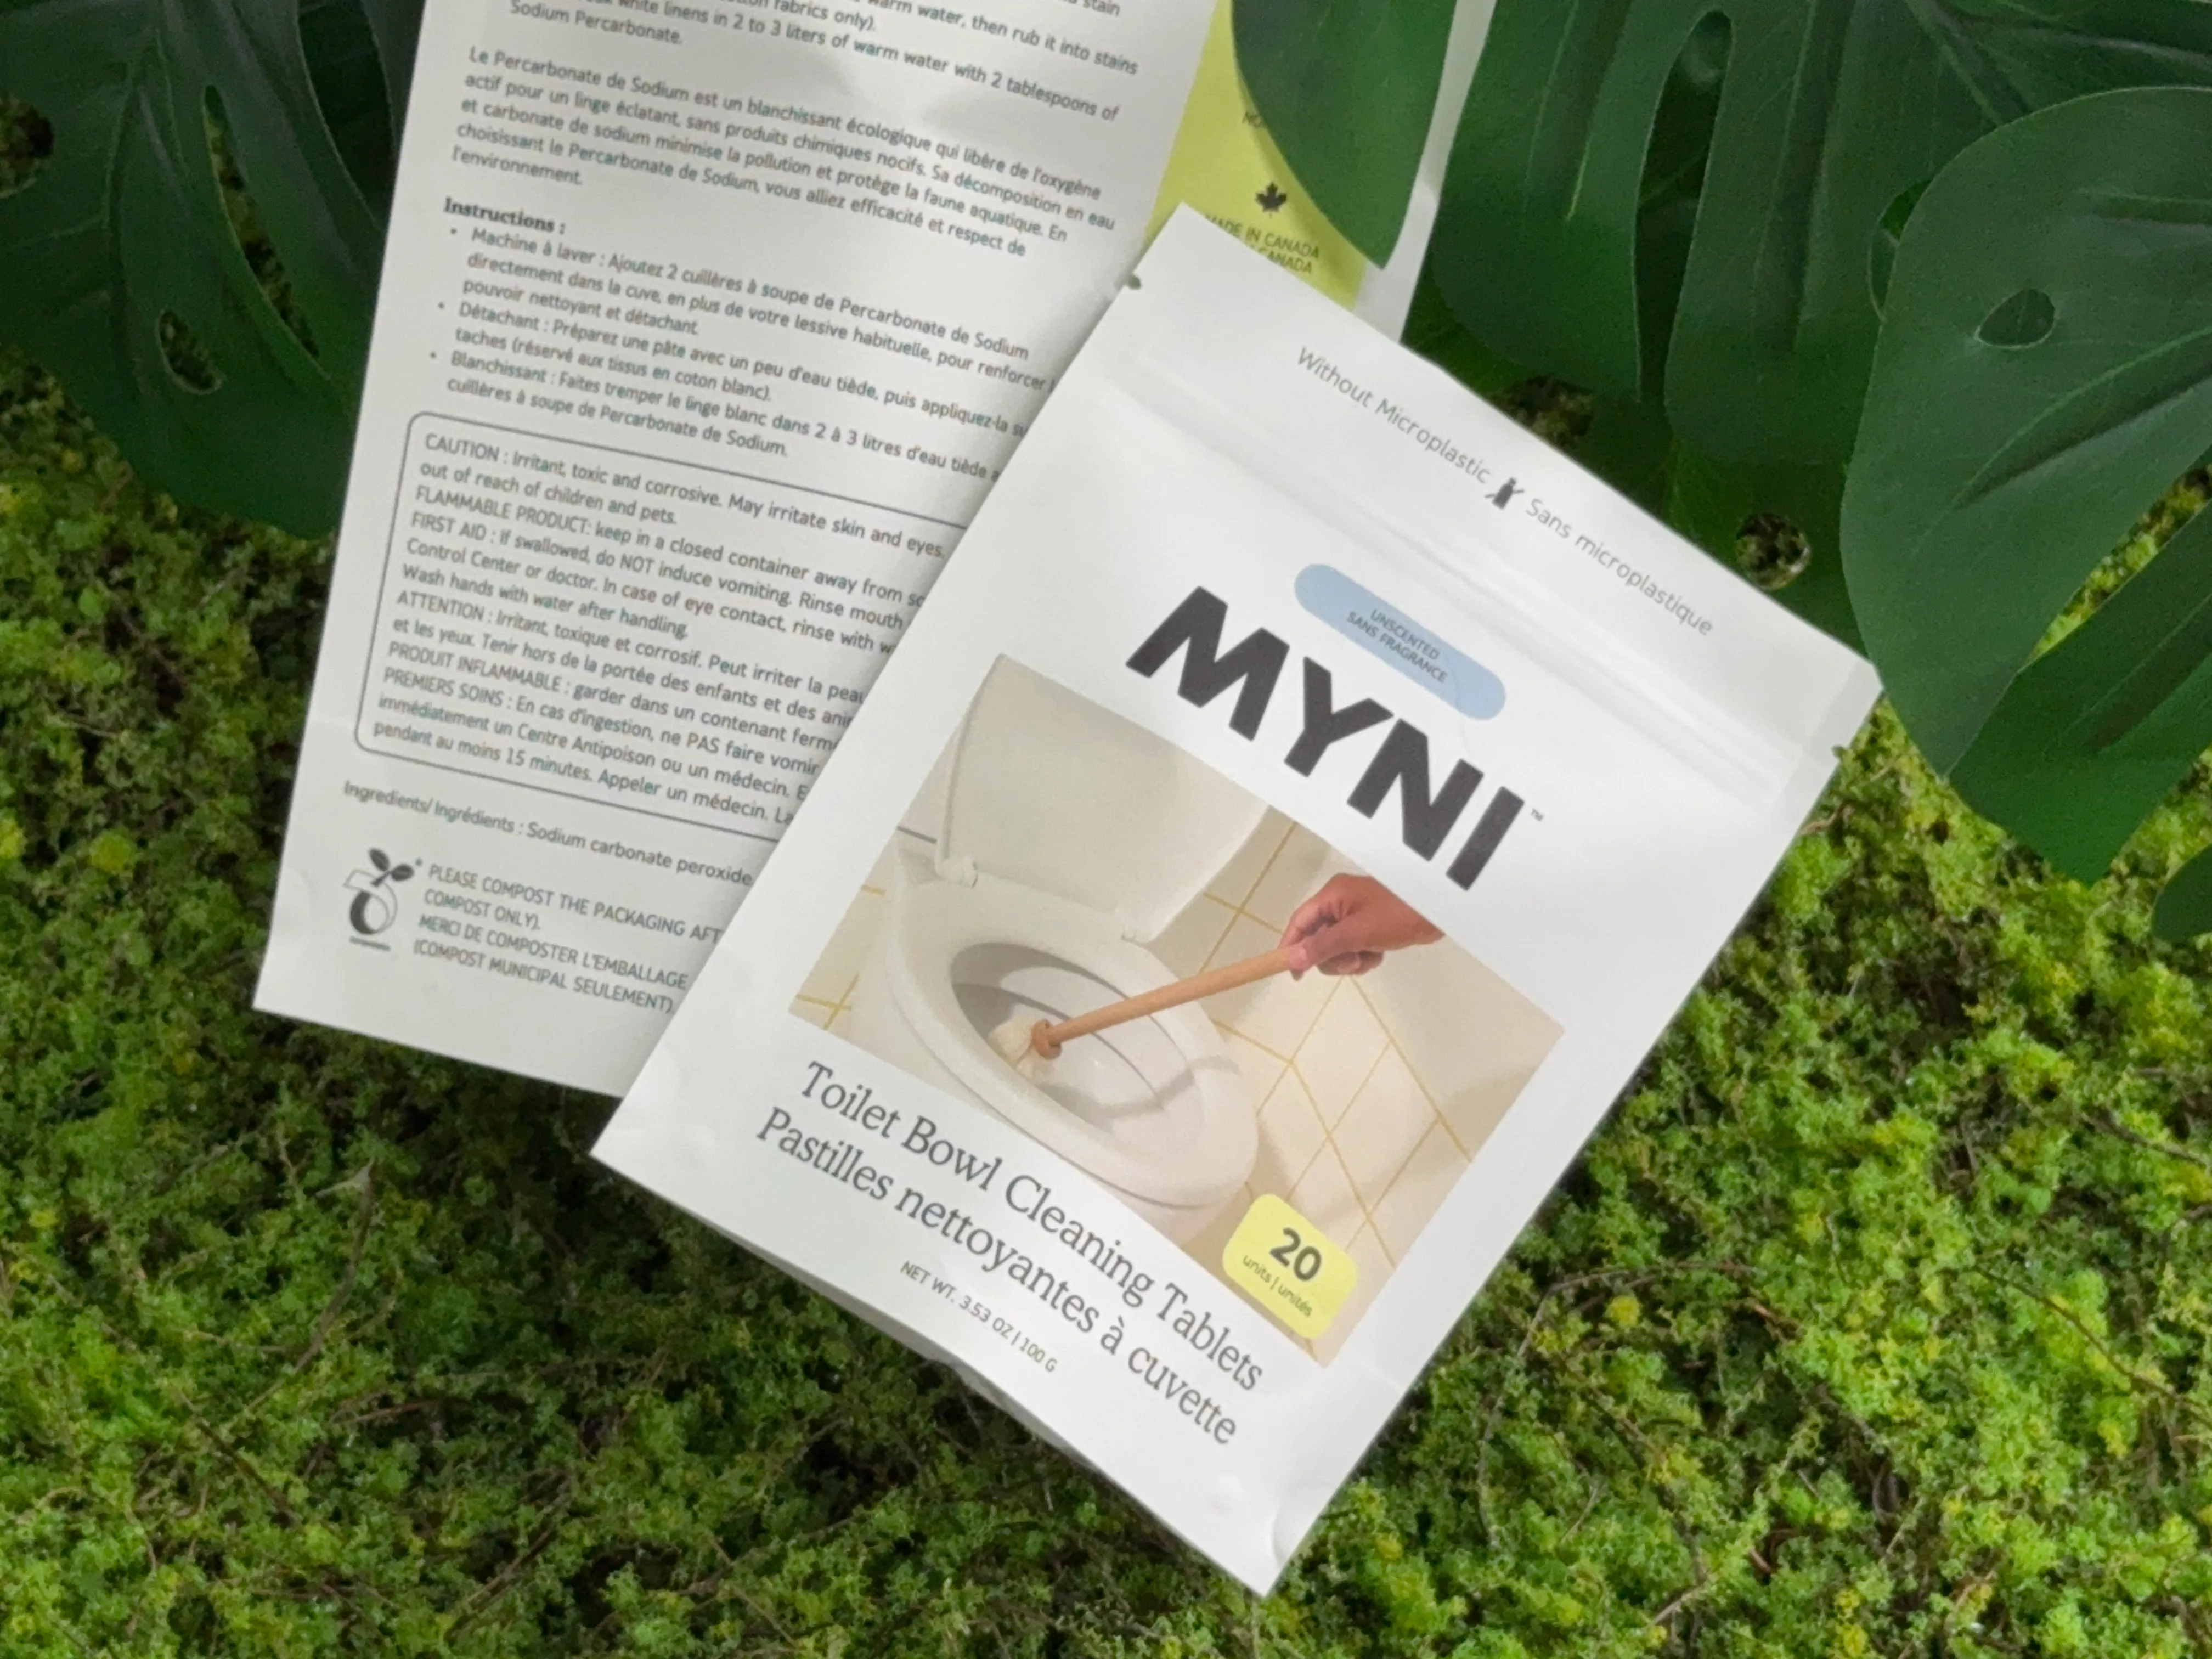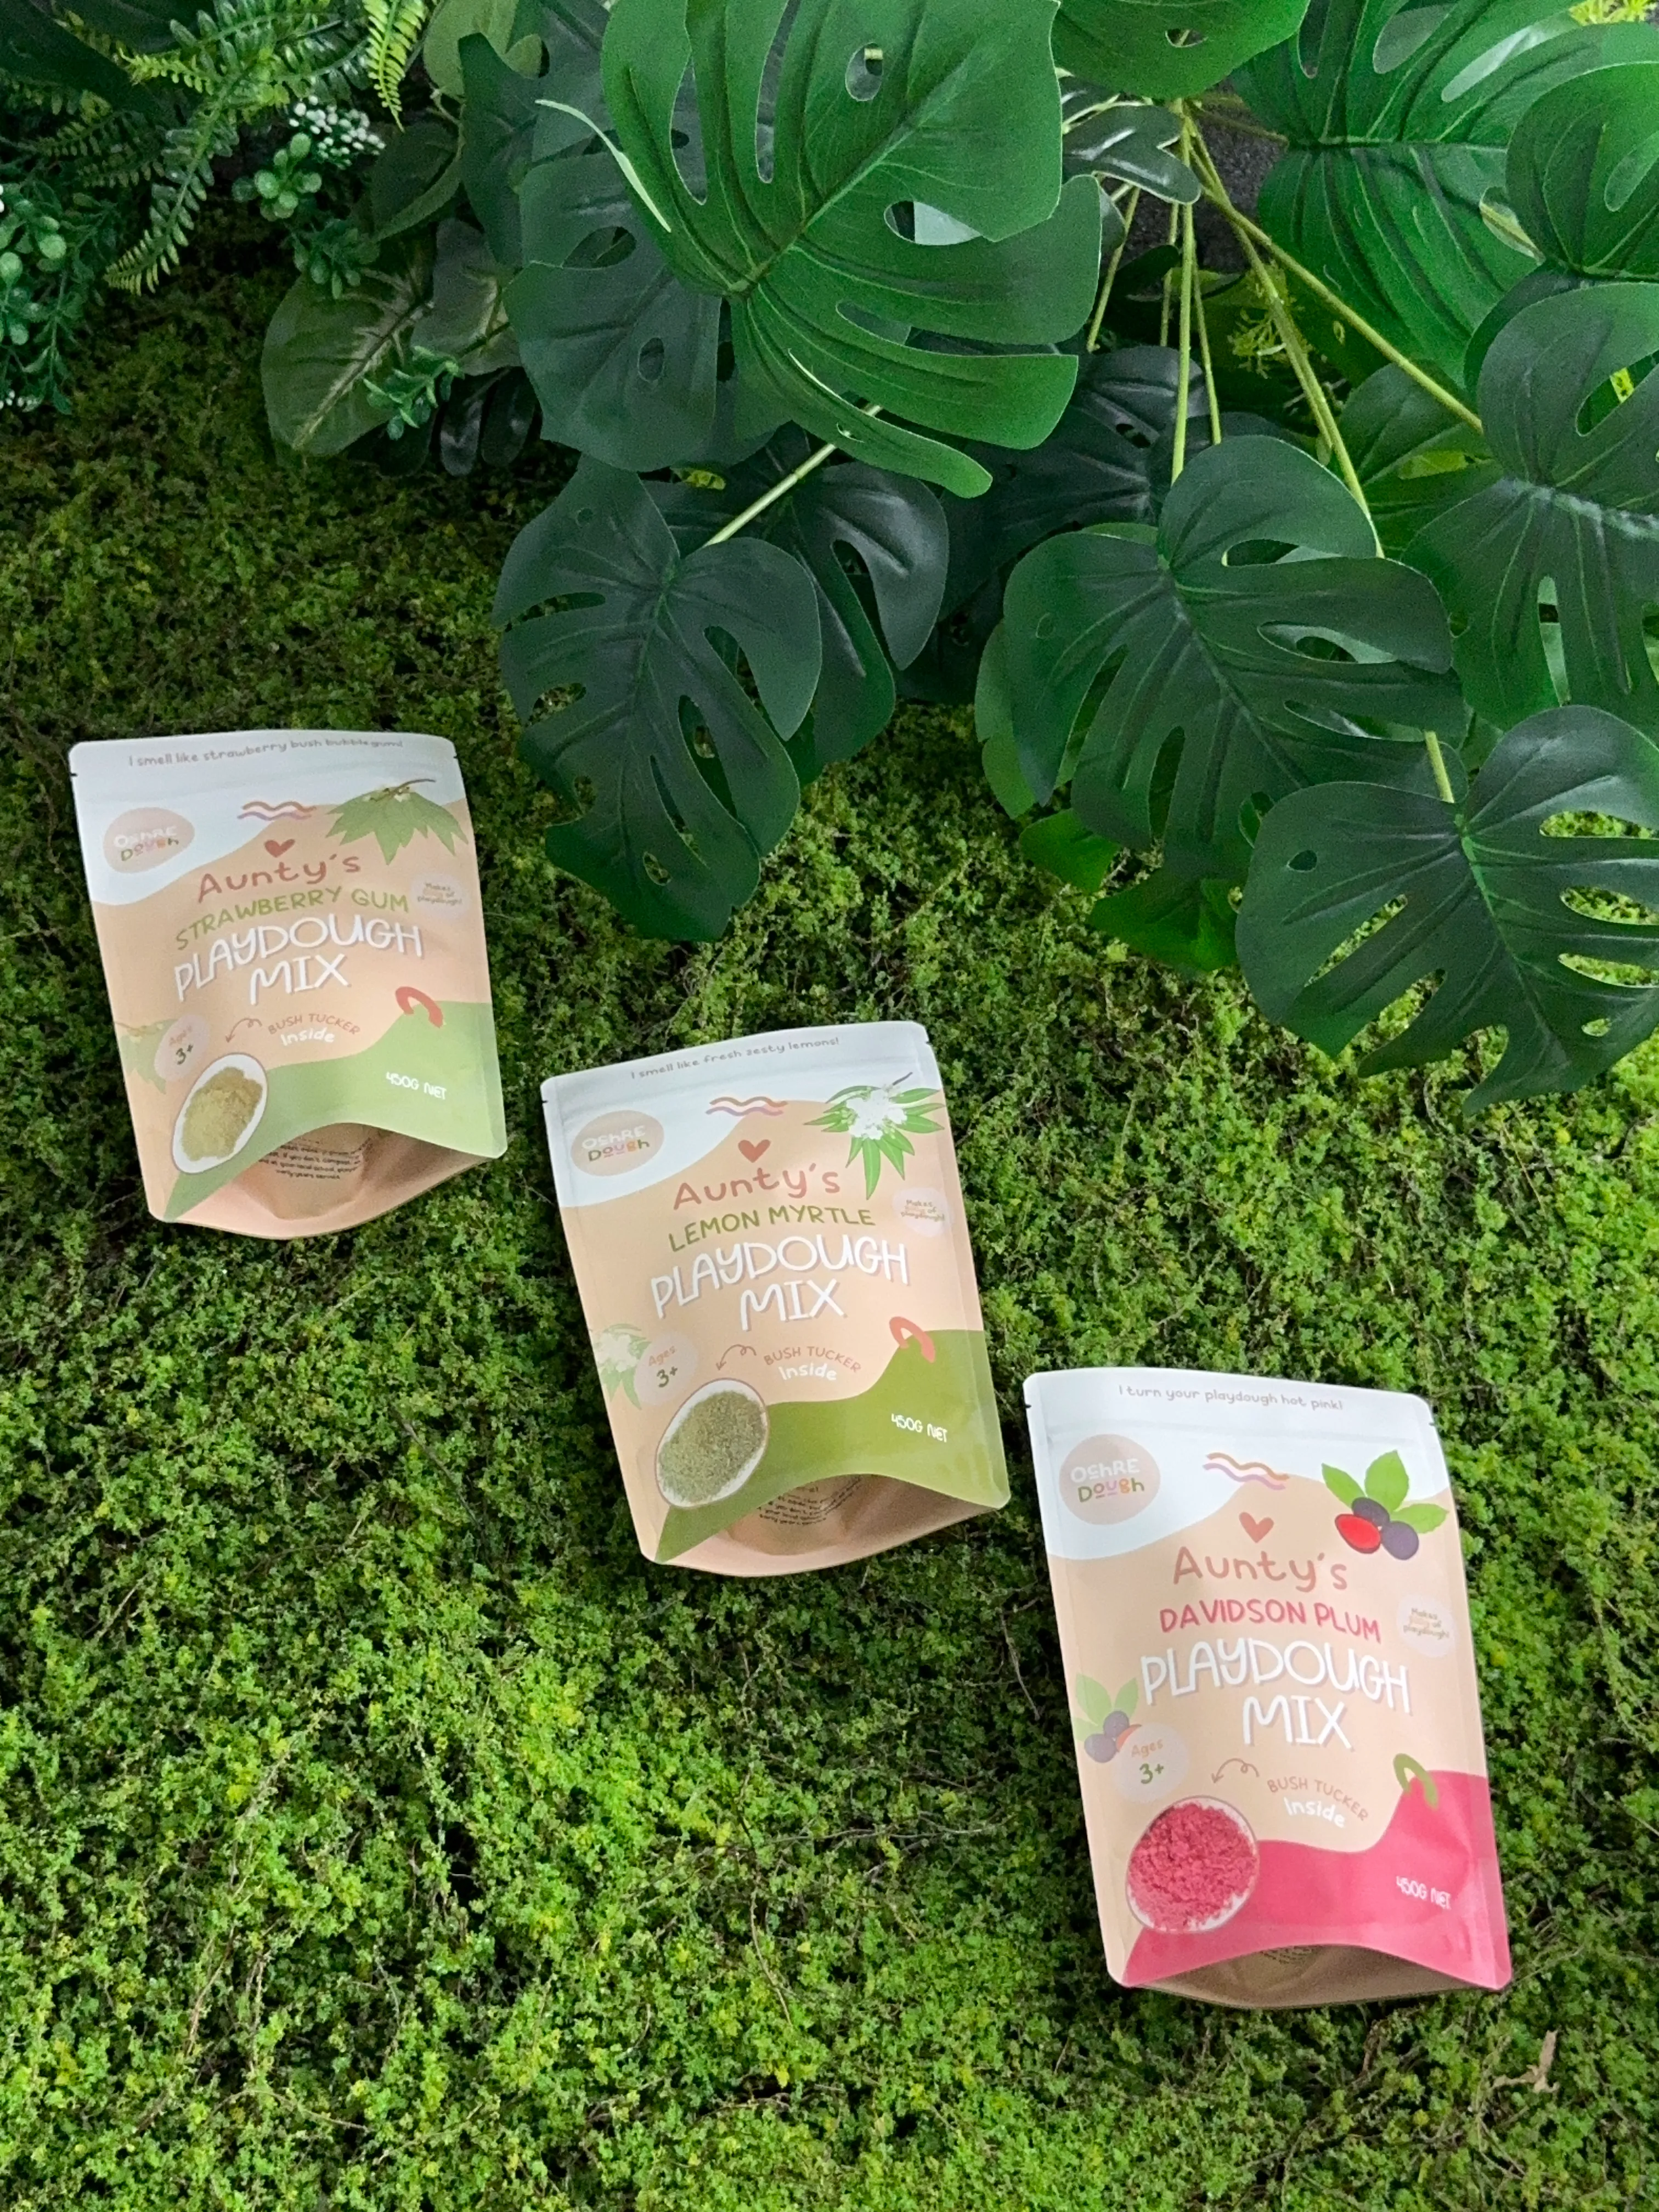
Superfood Brand Case Study | Recyclable Mono-PE Packaging for B-Corp Certified Brand Specifications
Solving Core Packaging Challenges for Superfood Brand Case Study | Recyclable Mono-PE Packaging for B-Corp Certified Brand
Concise B2B technical benchmarks designed to eliminate transit failures, regulatory penalties, and shelf-life loss.
Structure Approved Before It Is Ever Tested
Risk: The laminate looks right on paper and fails on your actual product, wasting the run.
Sample Packs in the Exact Structure, Tested With Your Product
You run your own fill and shelf-life test before any tooling is cut.
Barrier Numbers Missing From the Quote
Risk: You approve a film without knowing its oxygen or moisture transmission rate, then find out on shelf.
OTR and WVTR Stated on Every Quotation
The barrier figure is on the quote, not buried in a datasheet you never see.
Sustainability Claim Without a Certificate Behind It
Risk: An unsubstantiated compostable or recycled claim fails retailer and marketplace review.
Certificate Numbers Issued With the Quote
TÜV OK Compost HOME, BPI, EN 13432, AS 5810, GRS — referenced by certificate number.
Experience 3D Packaging Design & Free Dielines
Preview your pouch in 3D WebGL Studio and export production-ready dielines.
Who Is This Client?
Company
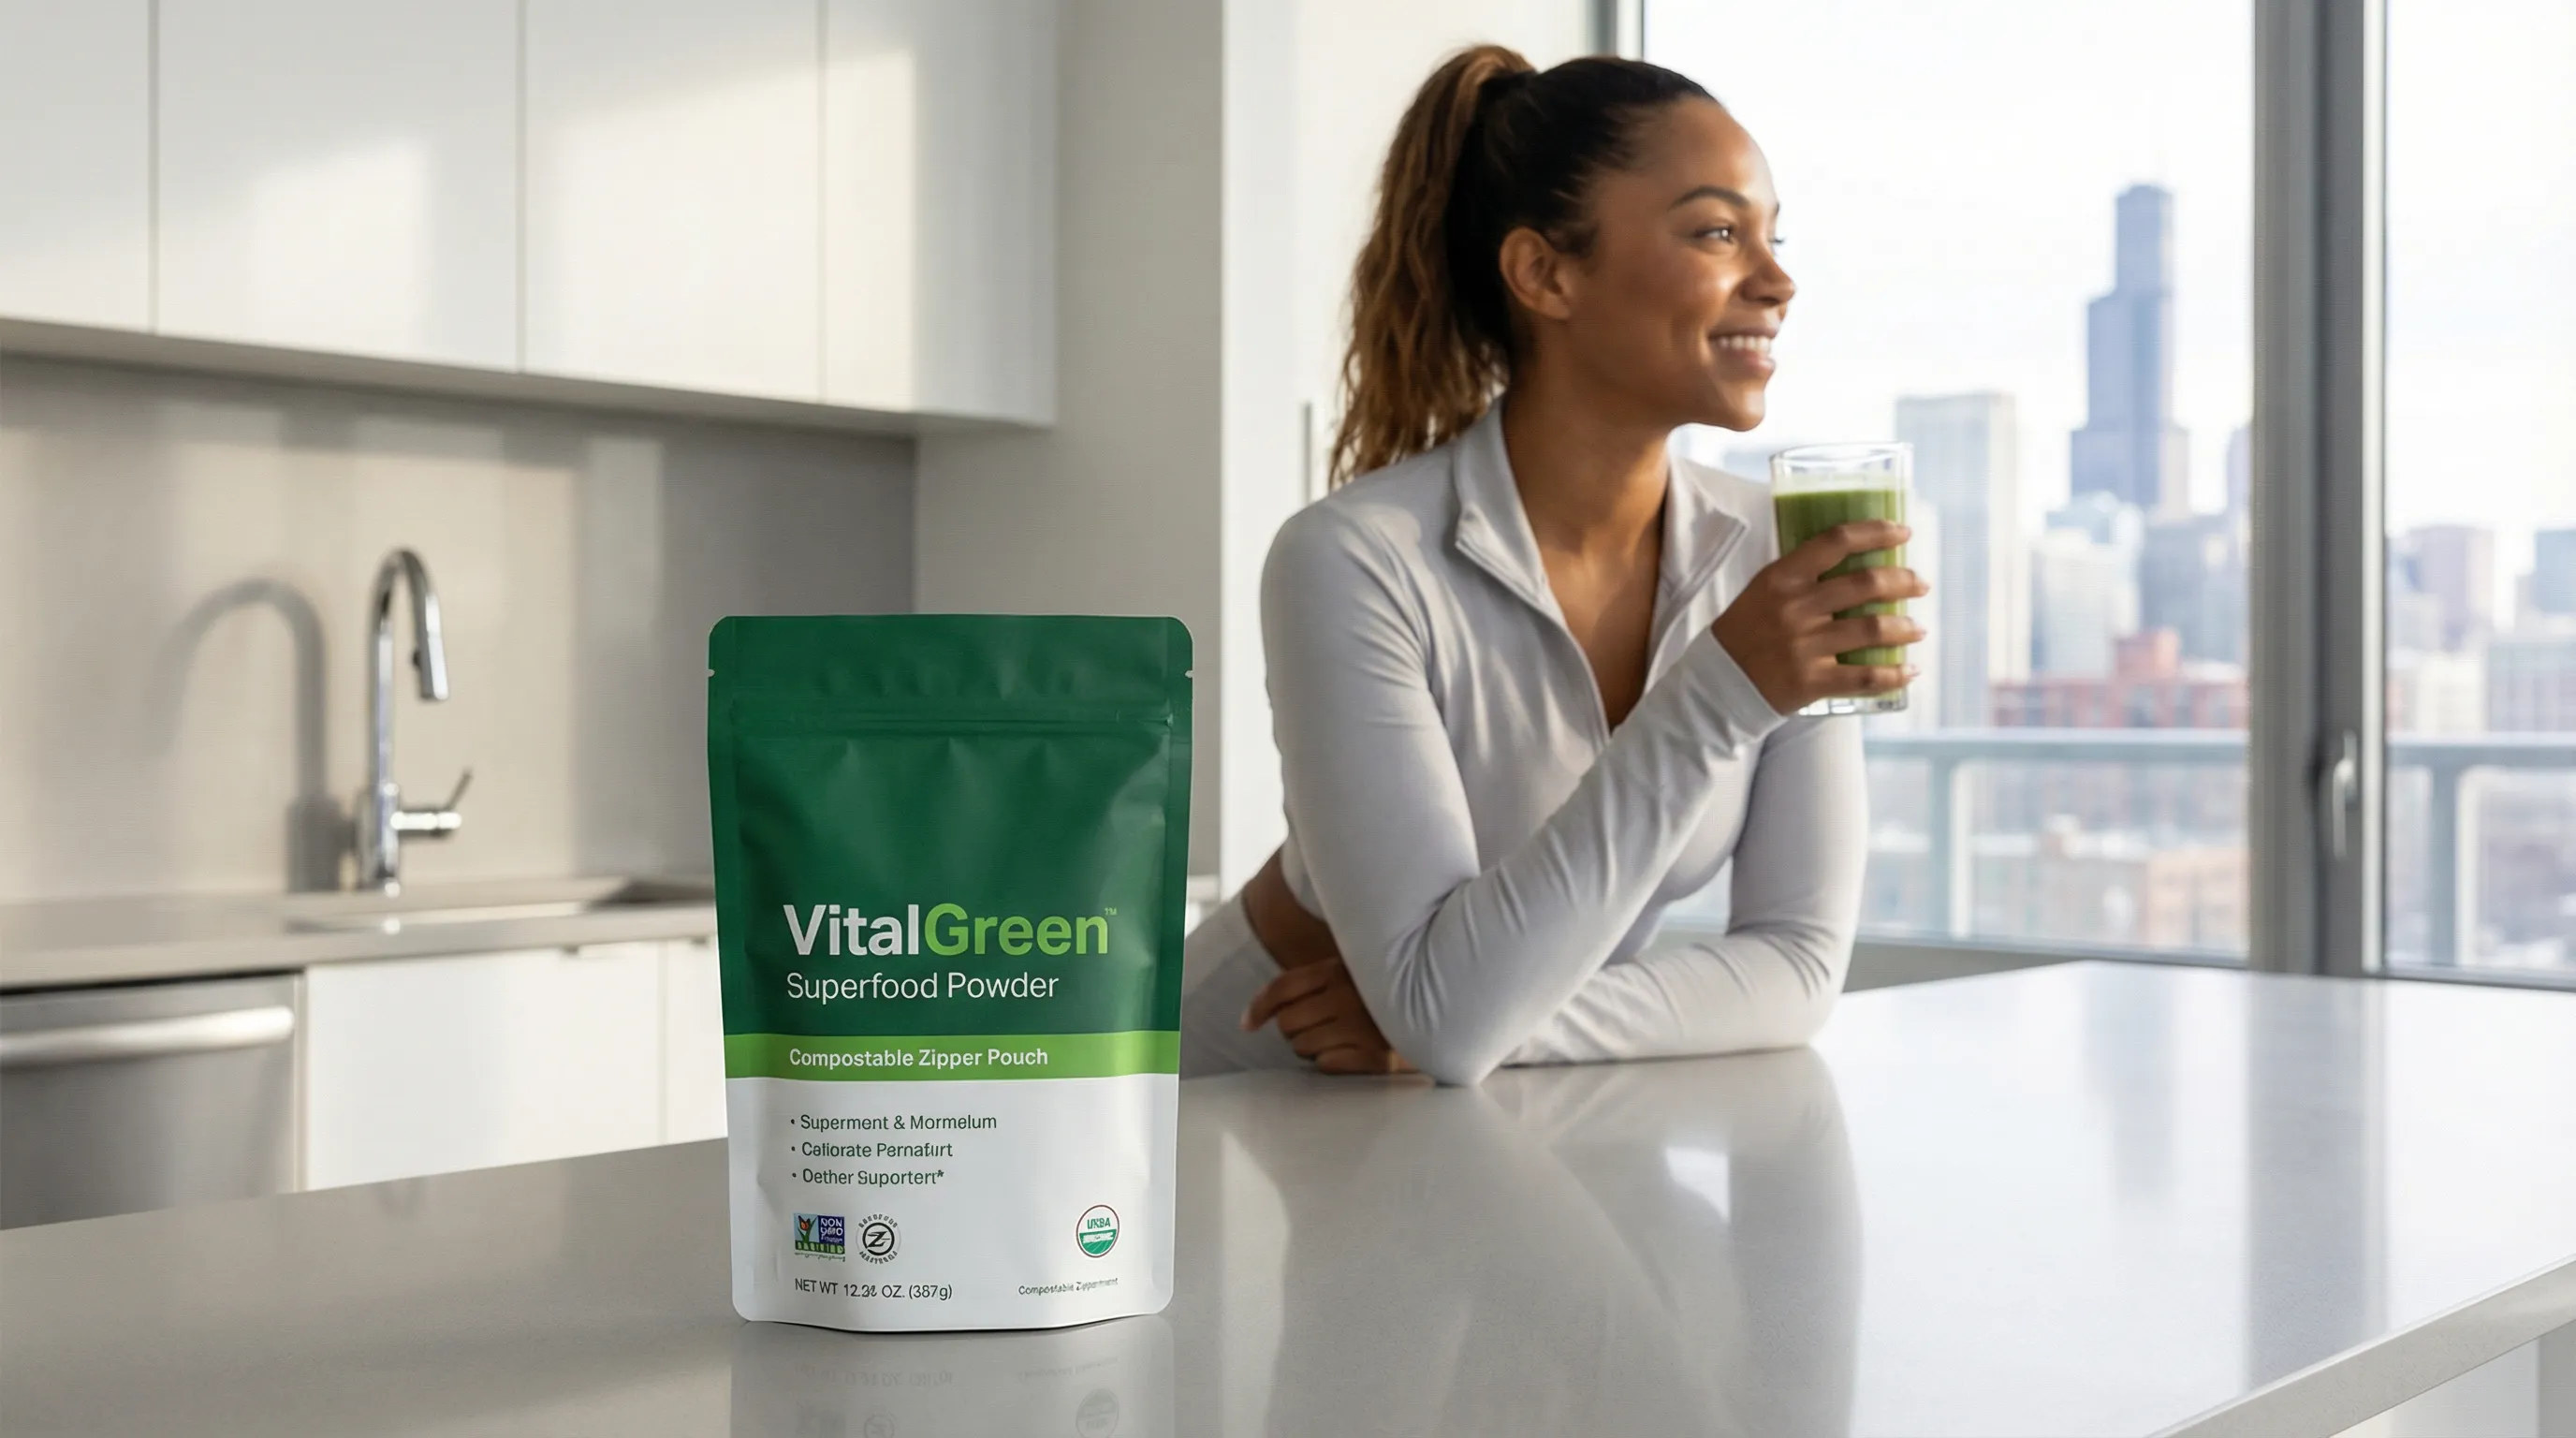
VitalGreen Superfoods
Industry
Superfood & Wellness Powders
Location
Chicago, Illinois, USA
Package Type
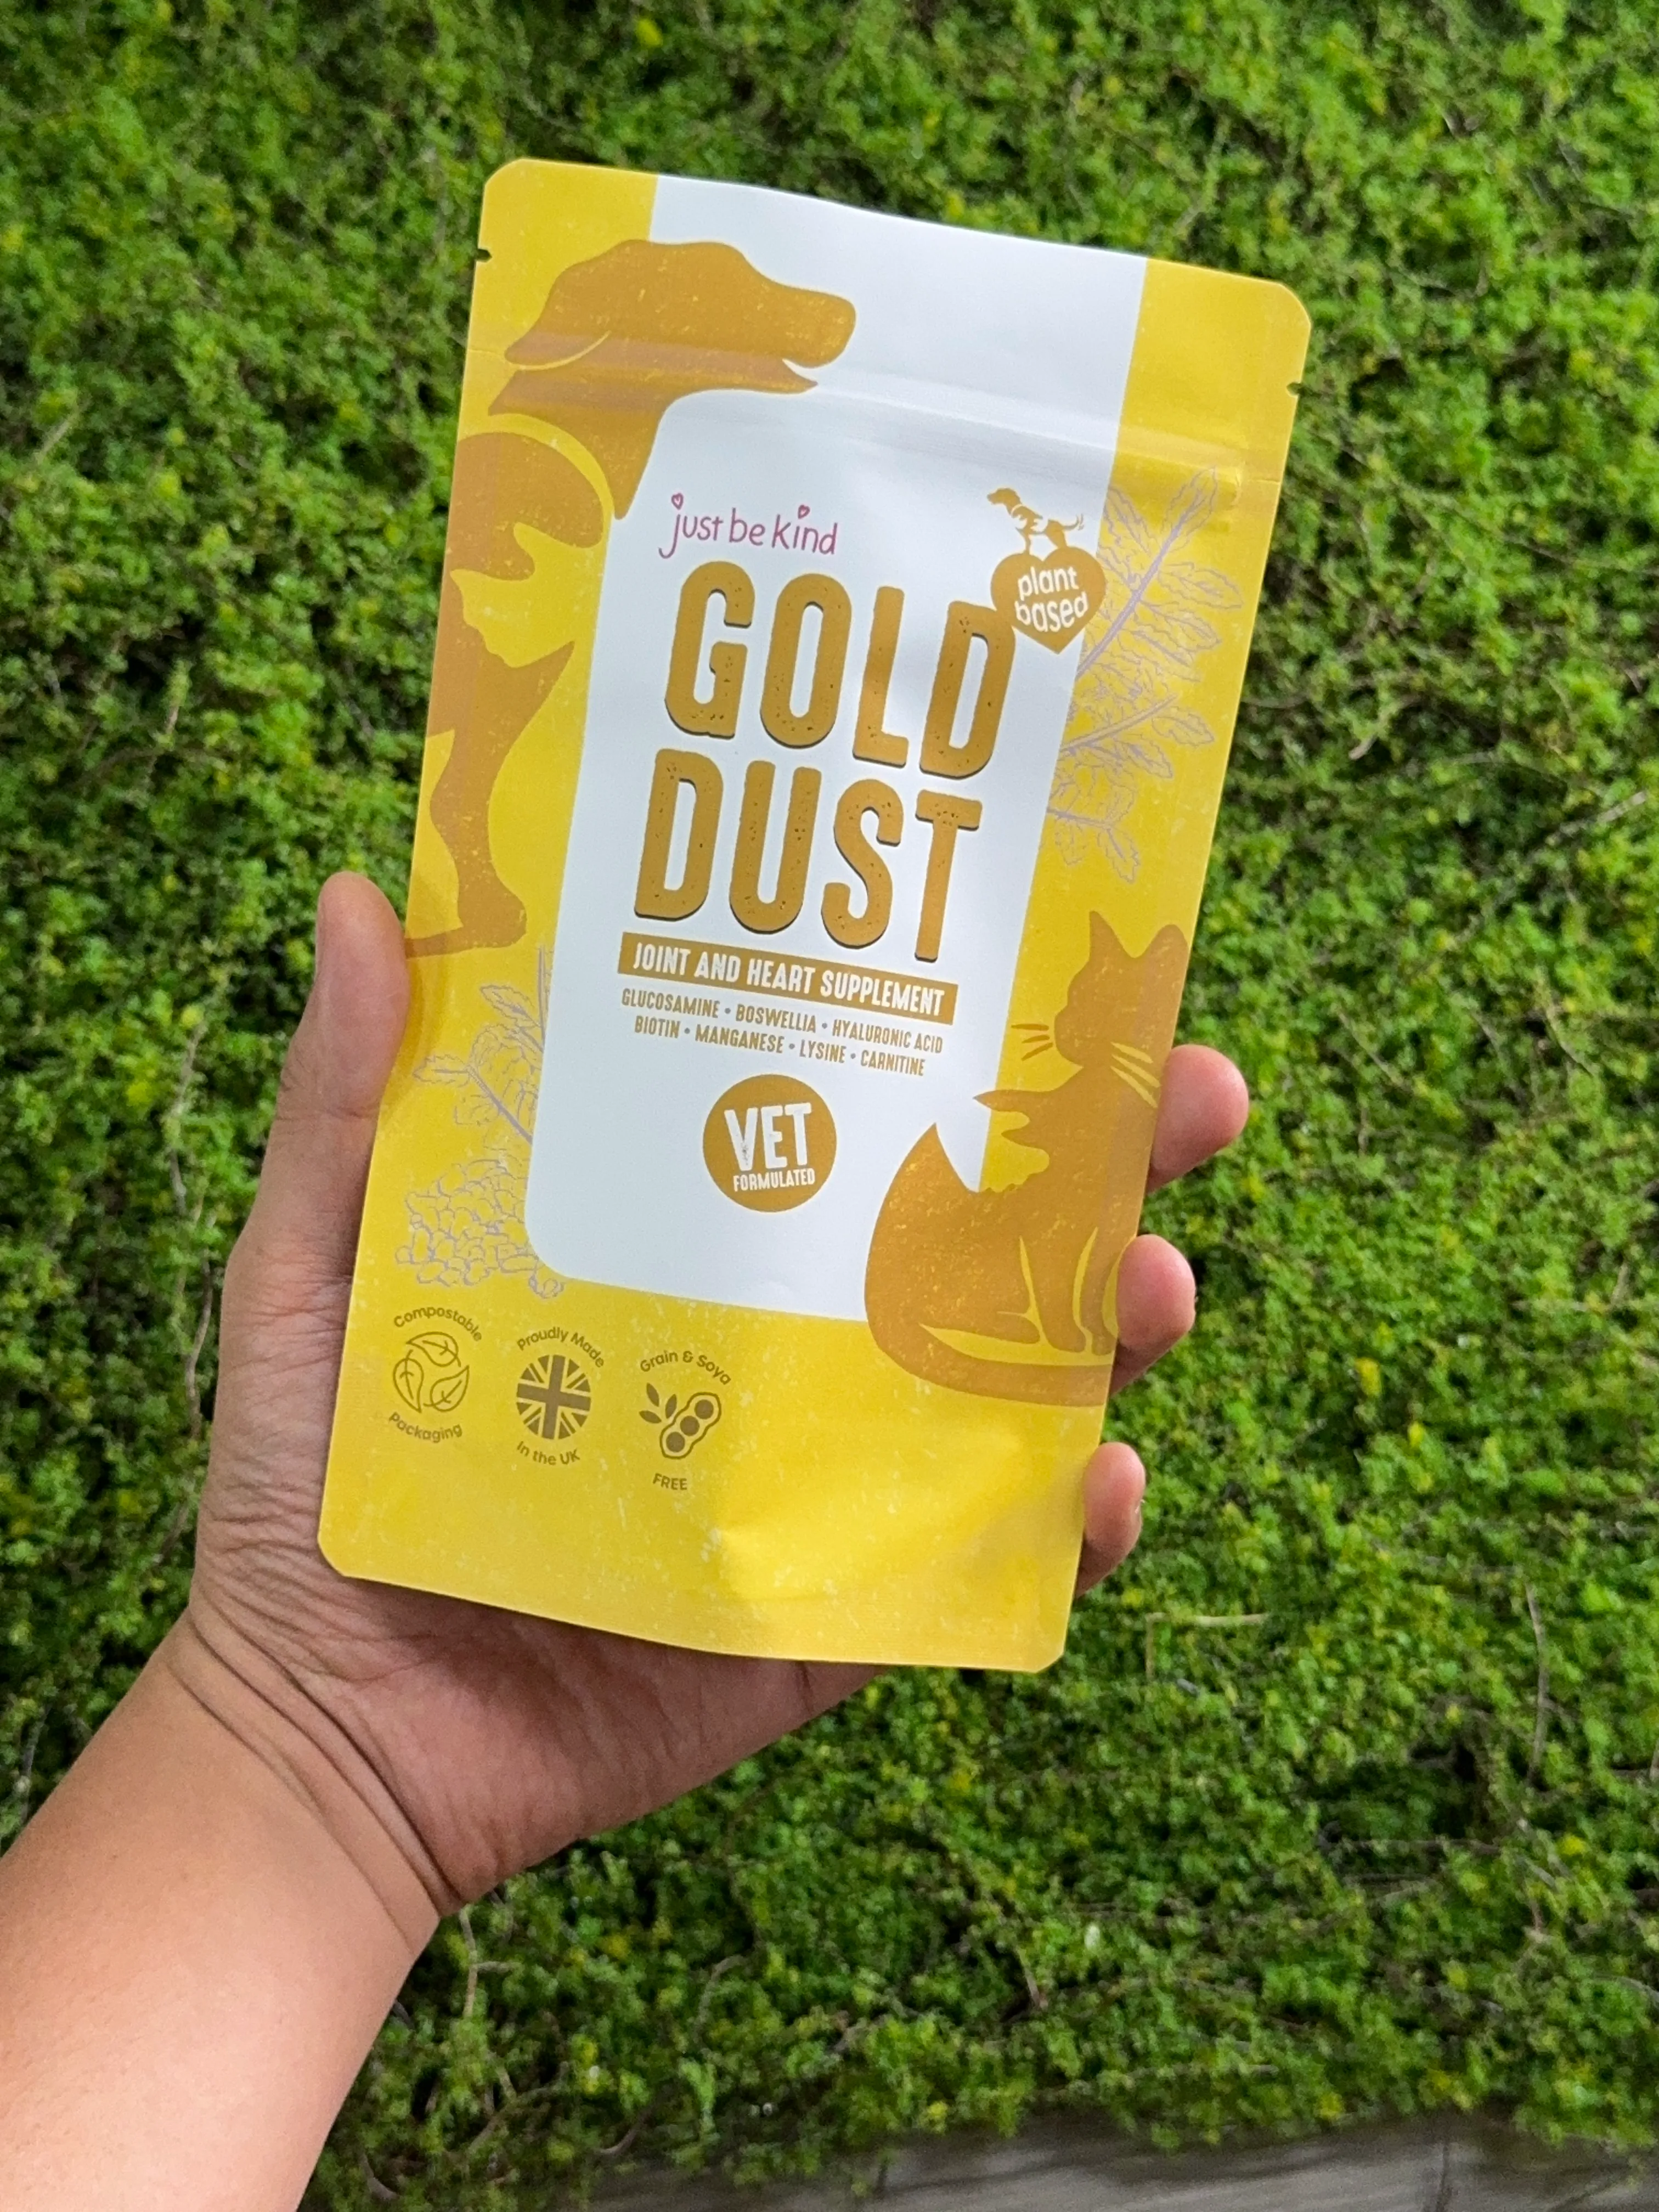
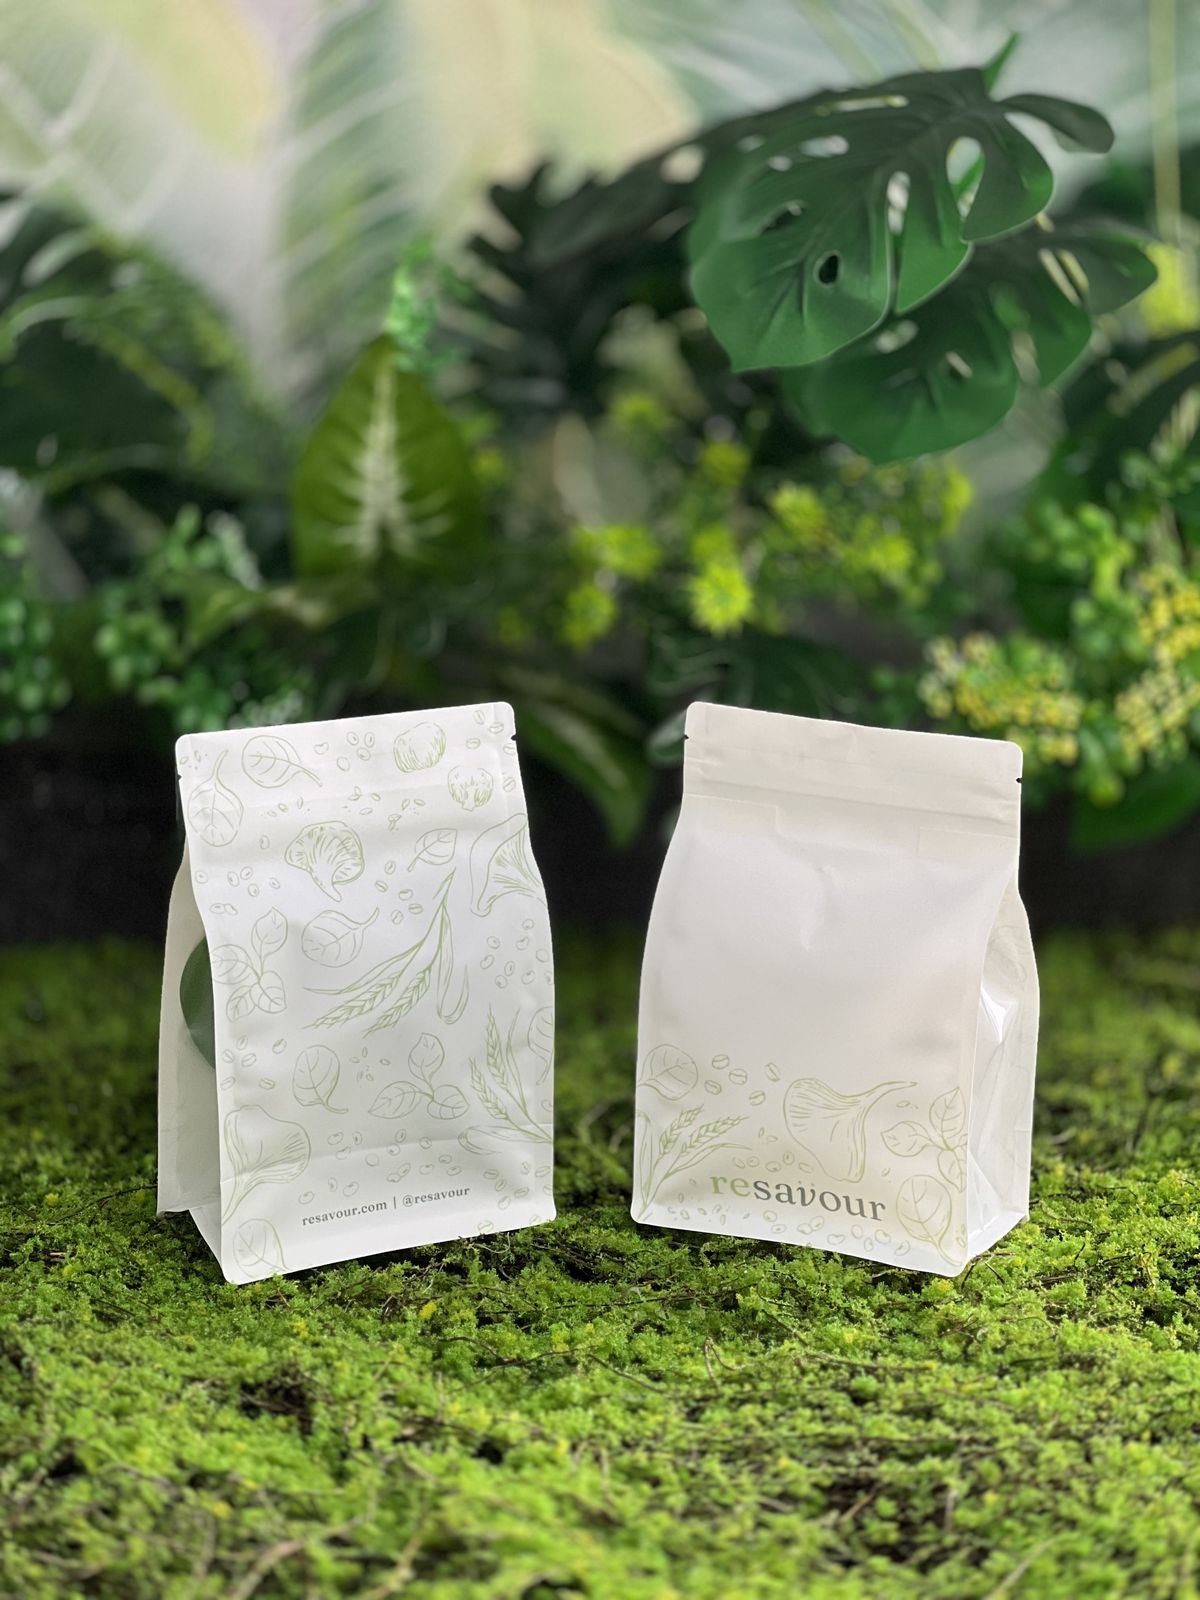
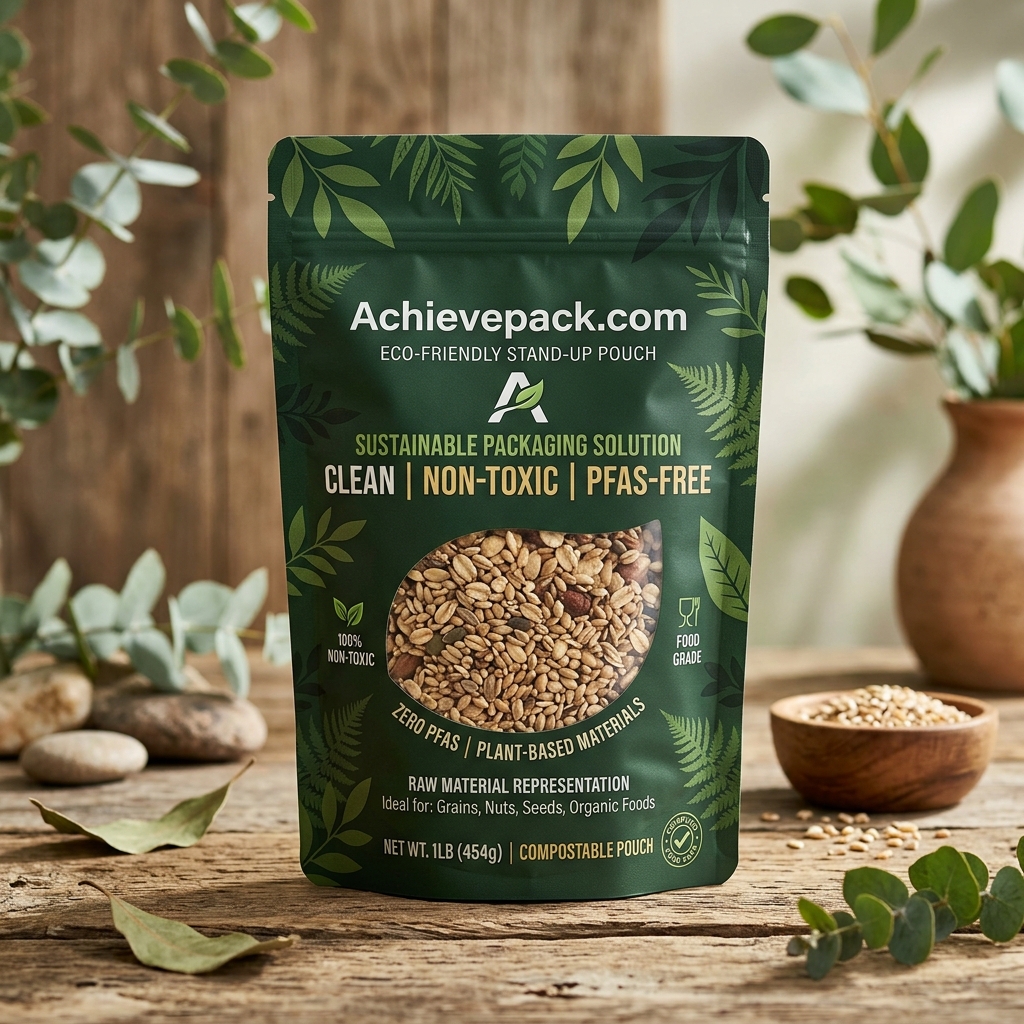
Stand-Up Pouches with Zipper
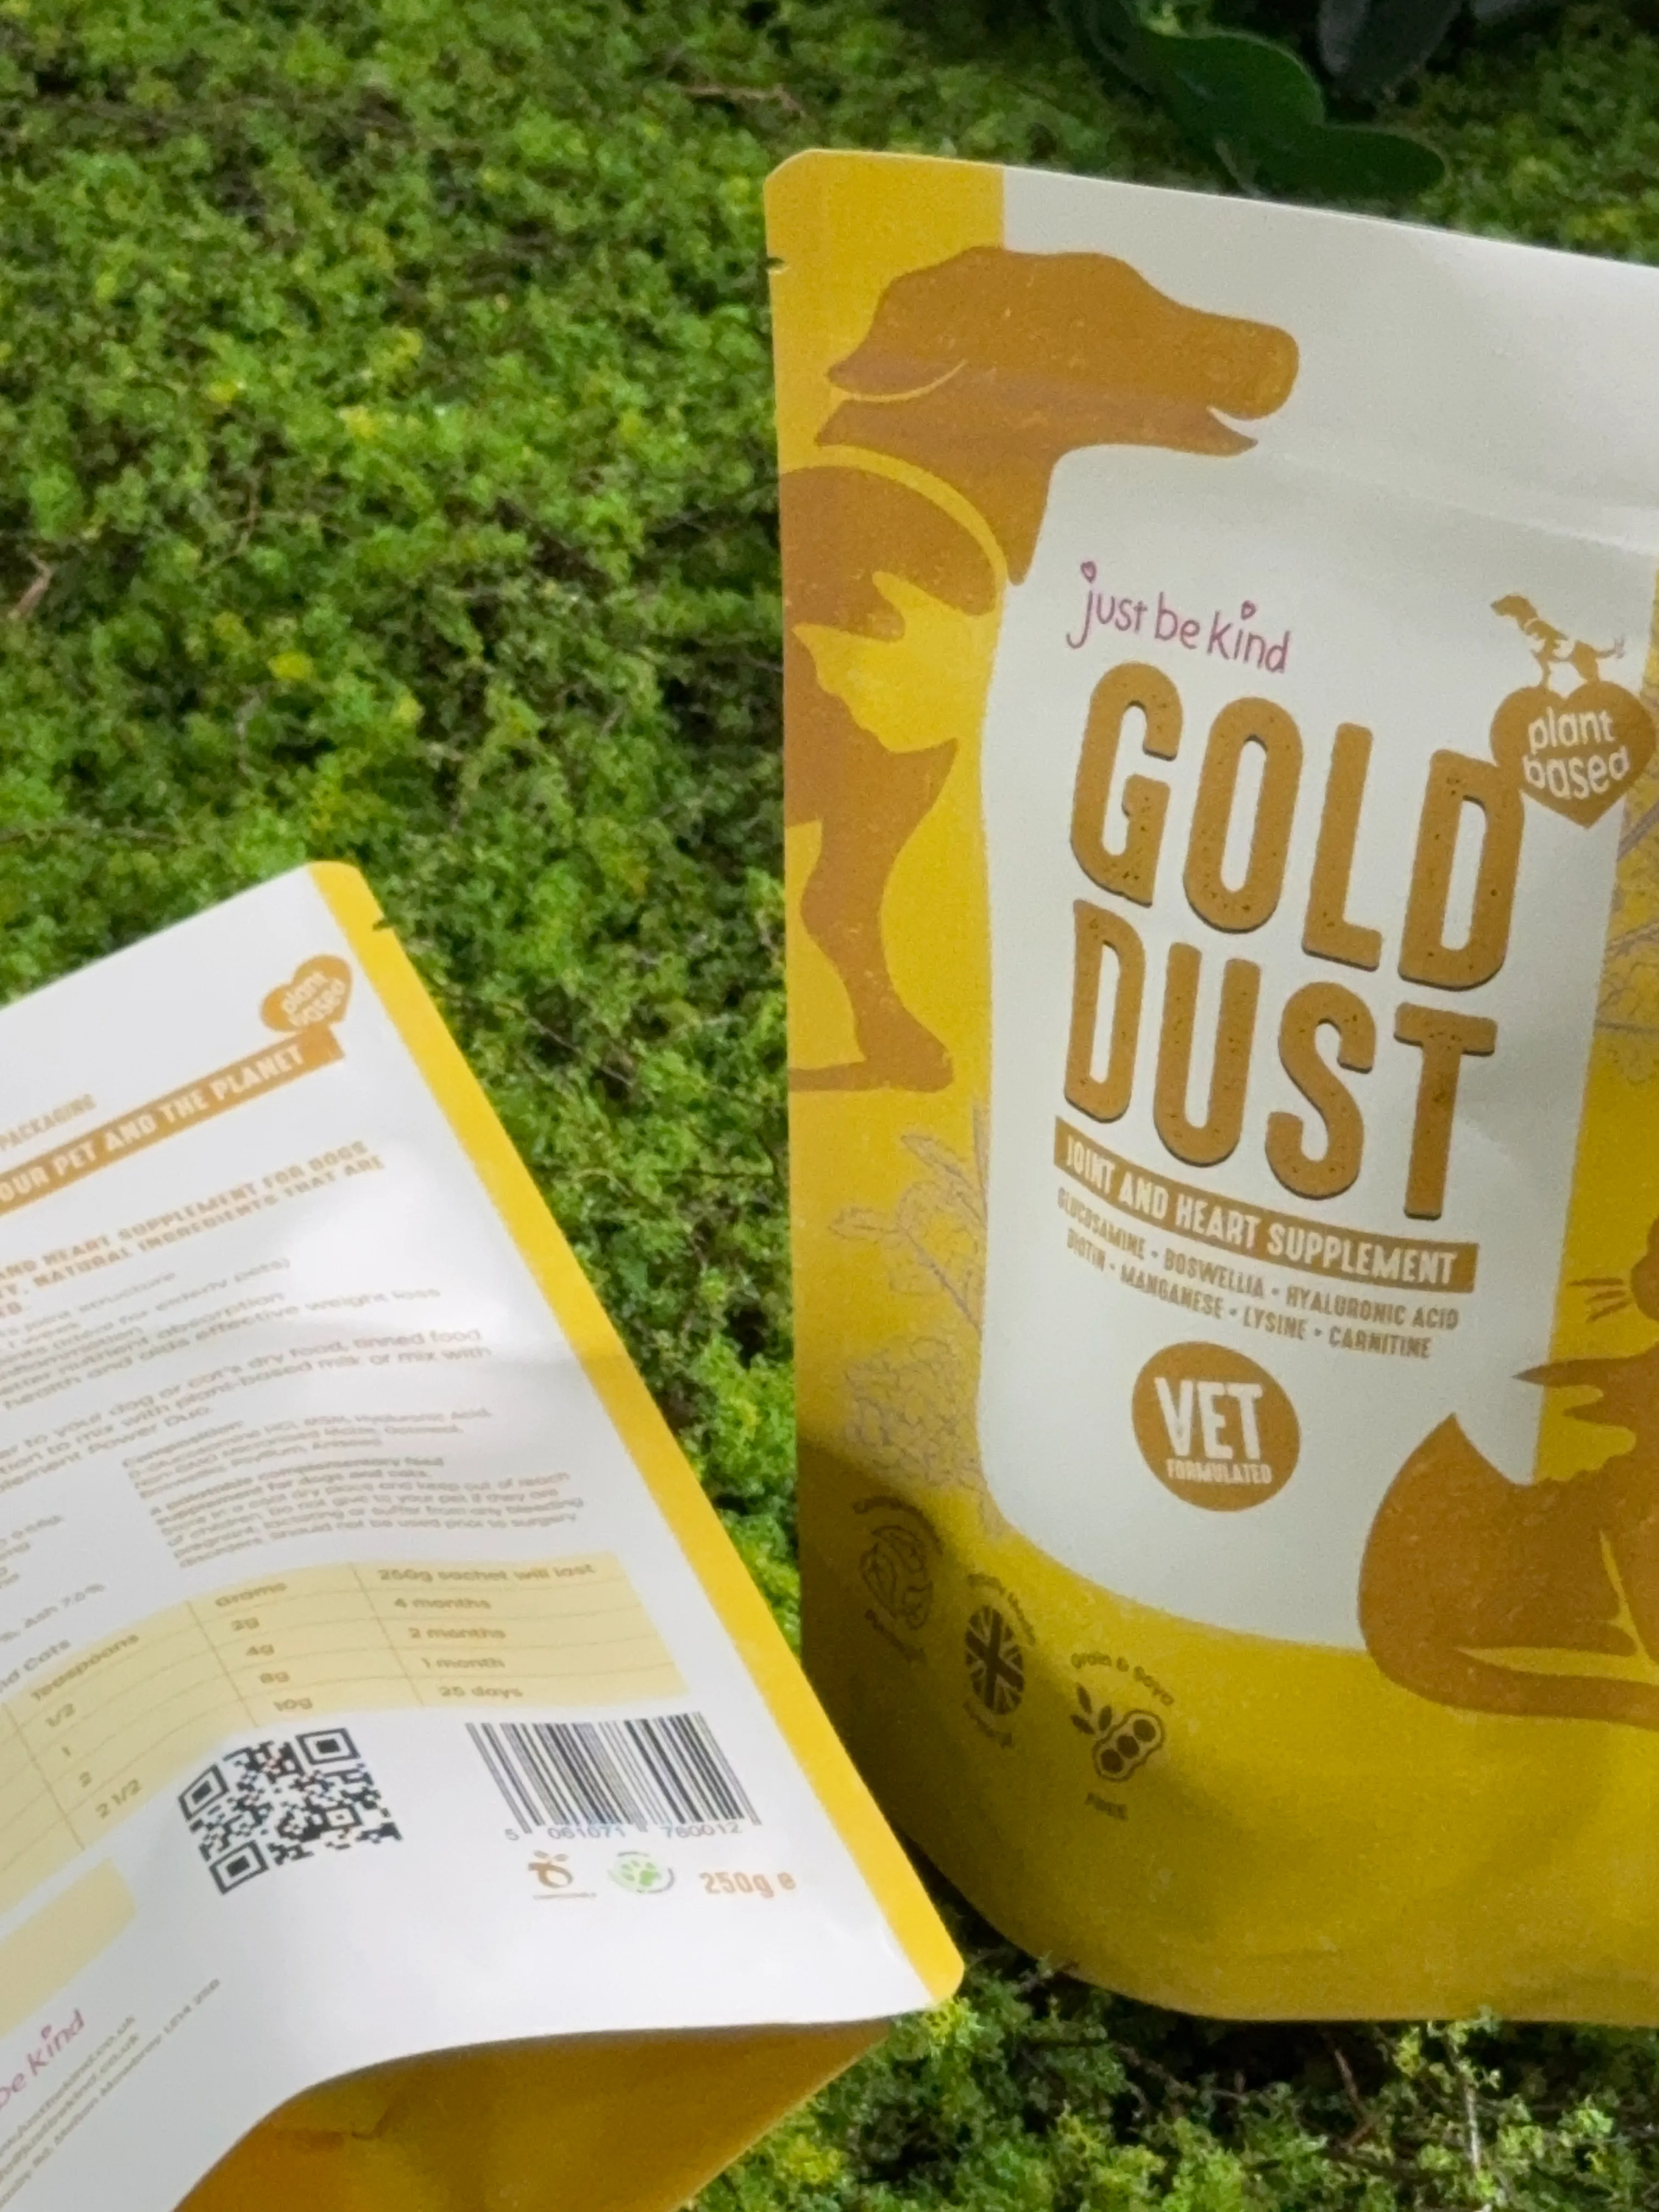
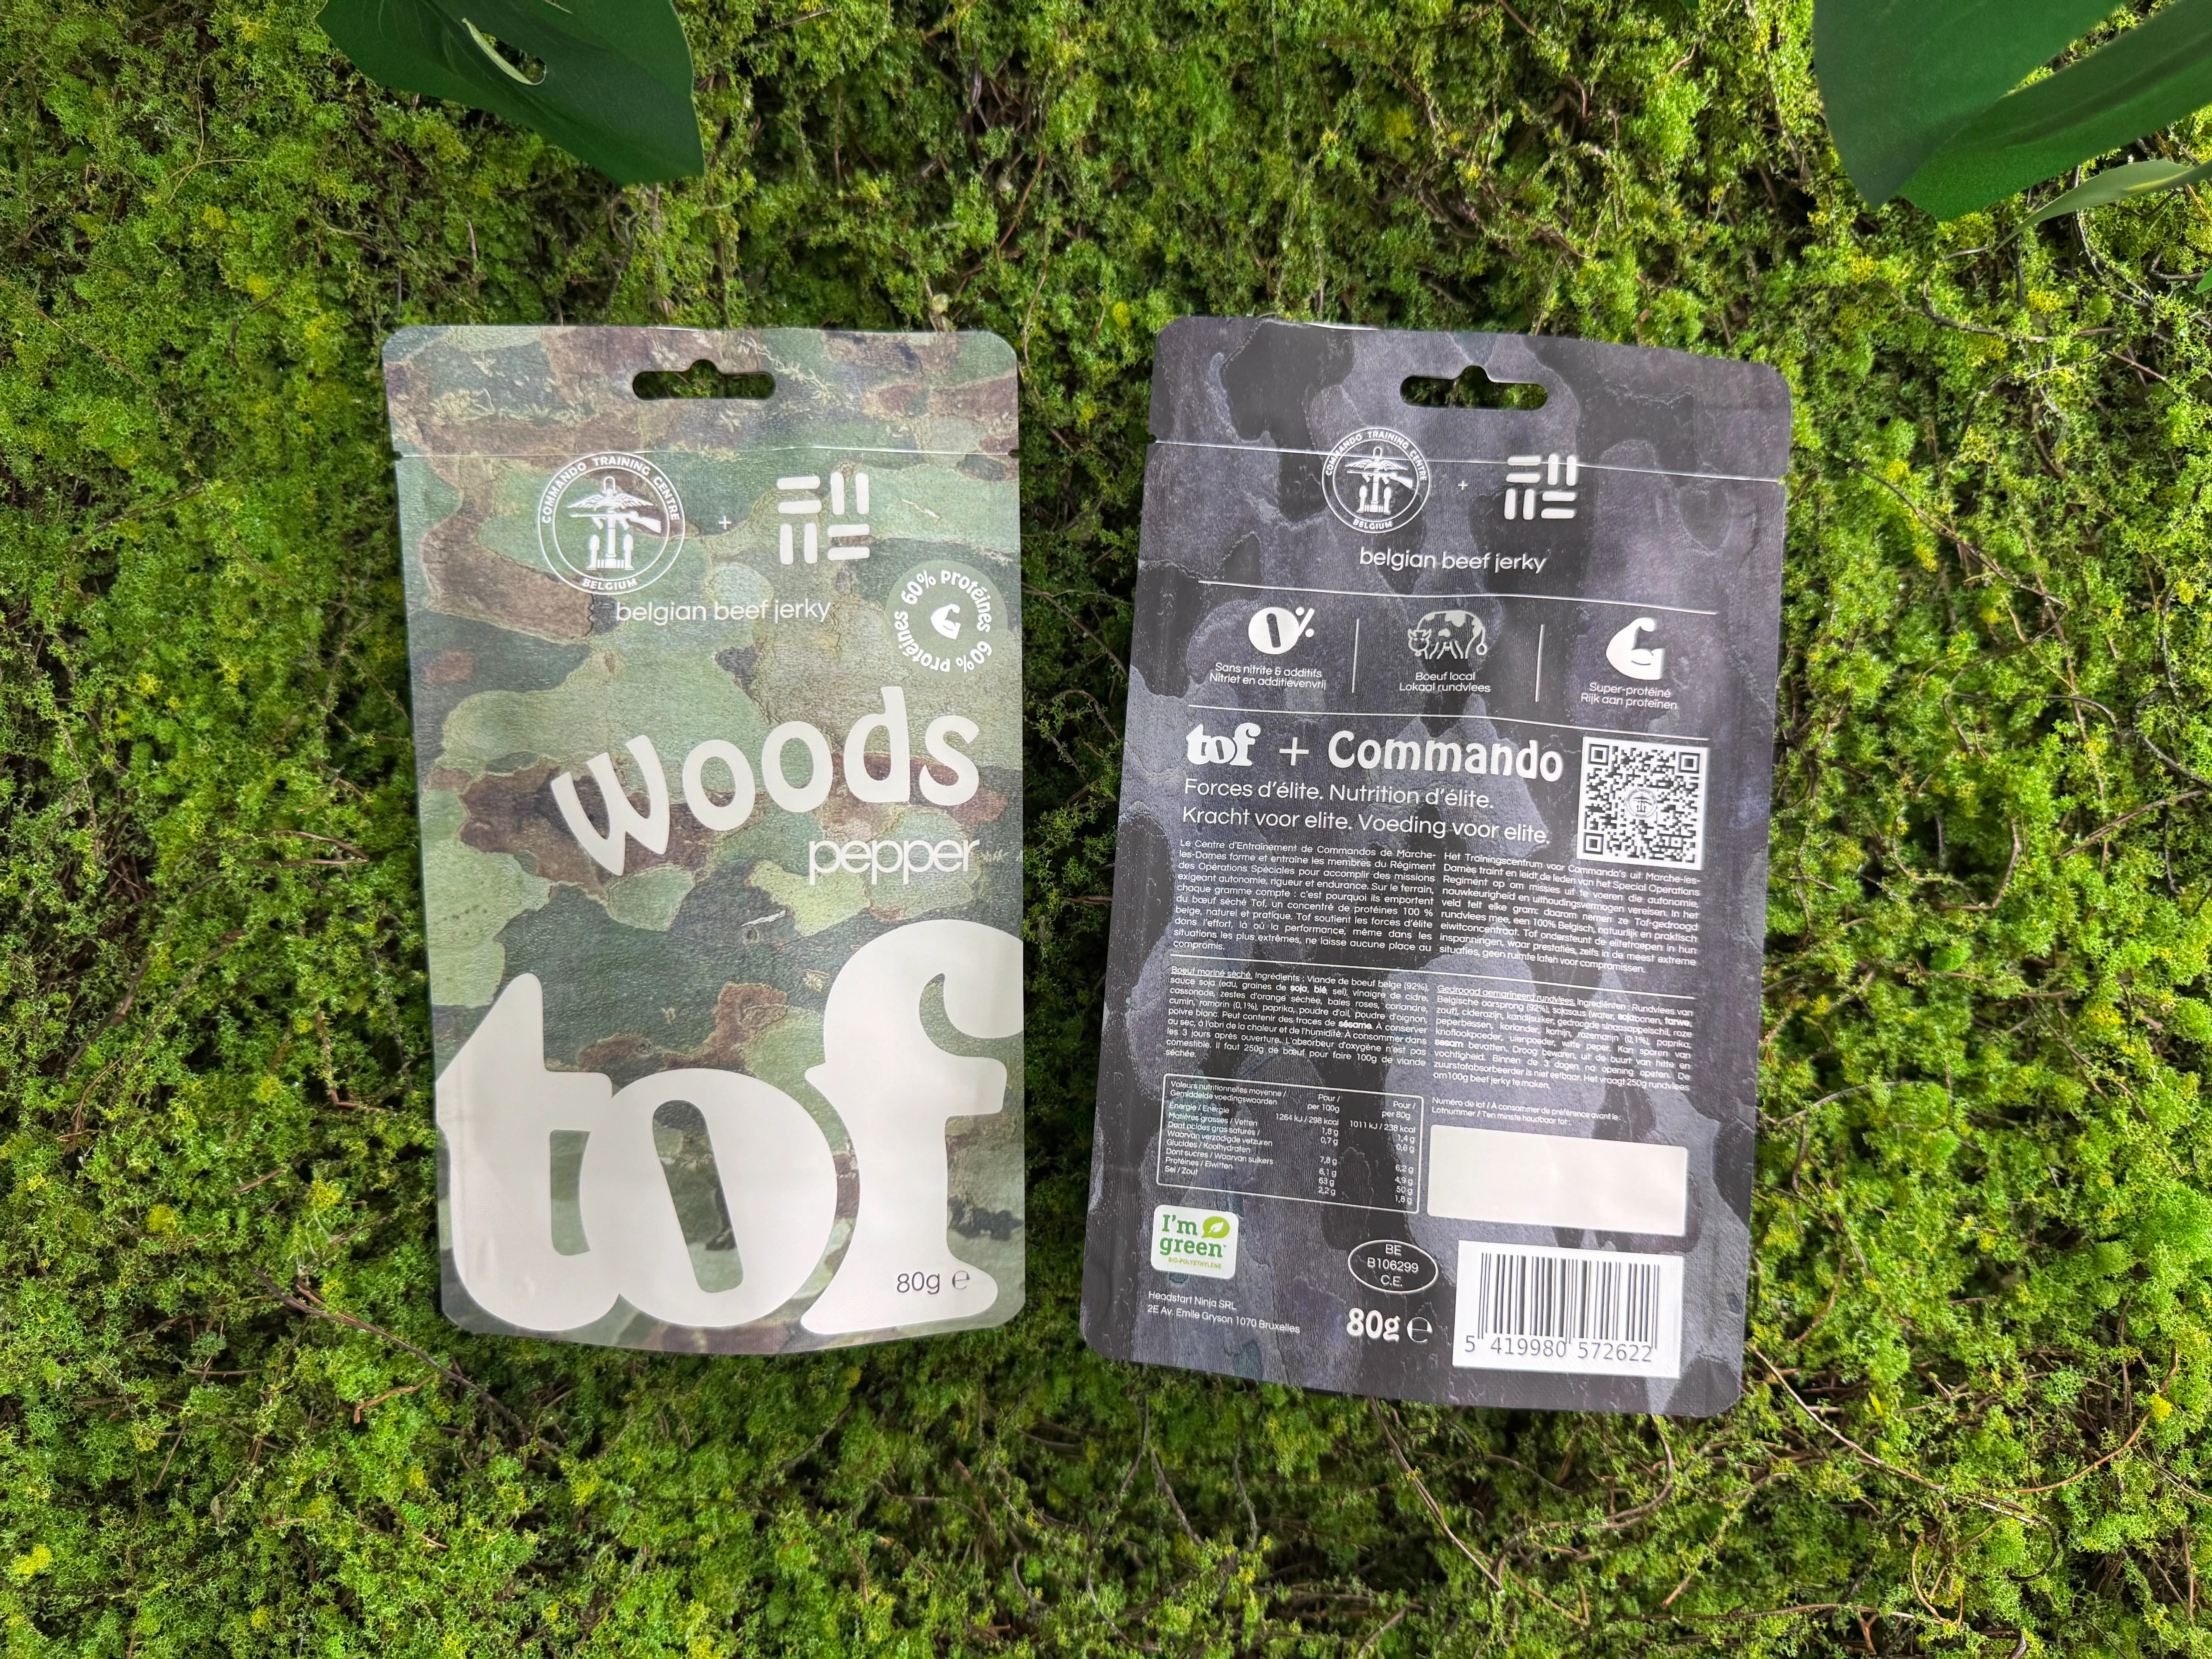
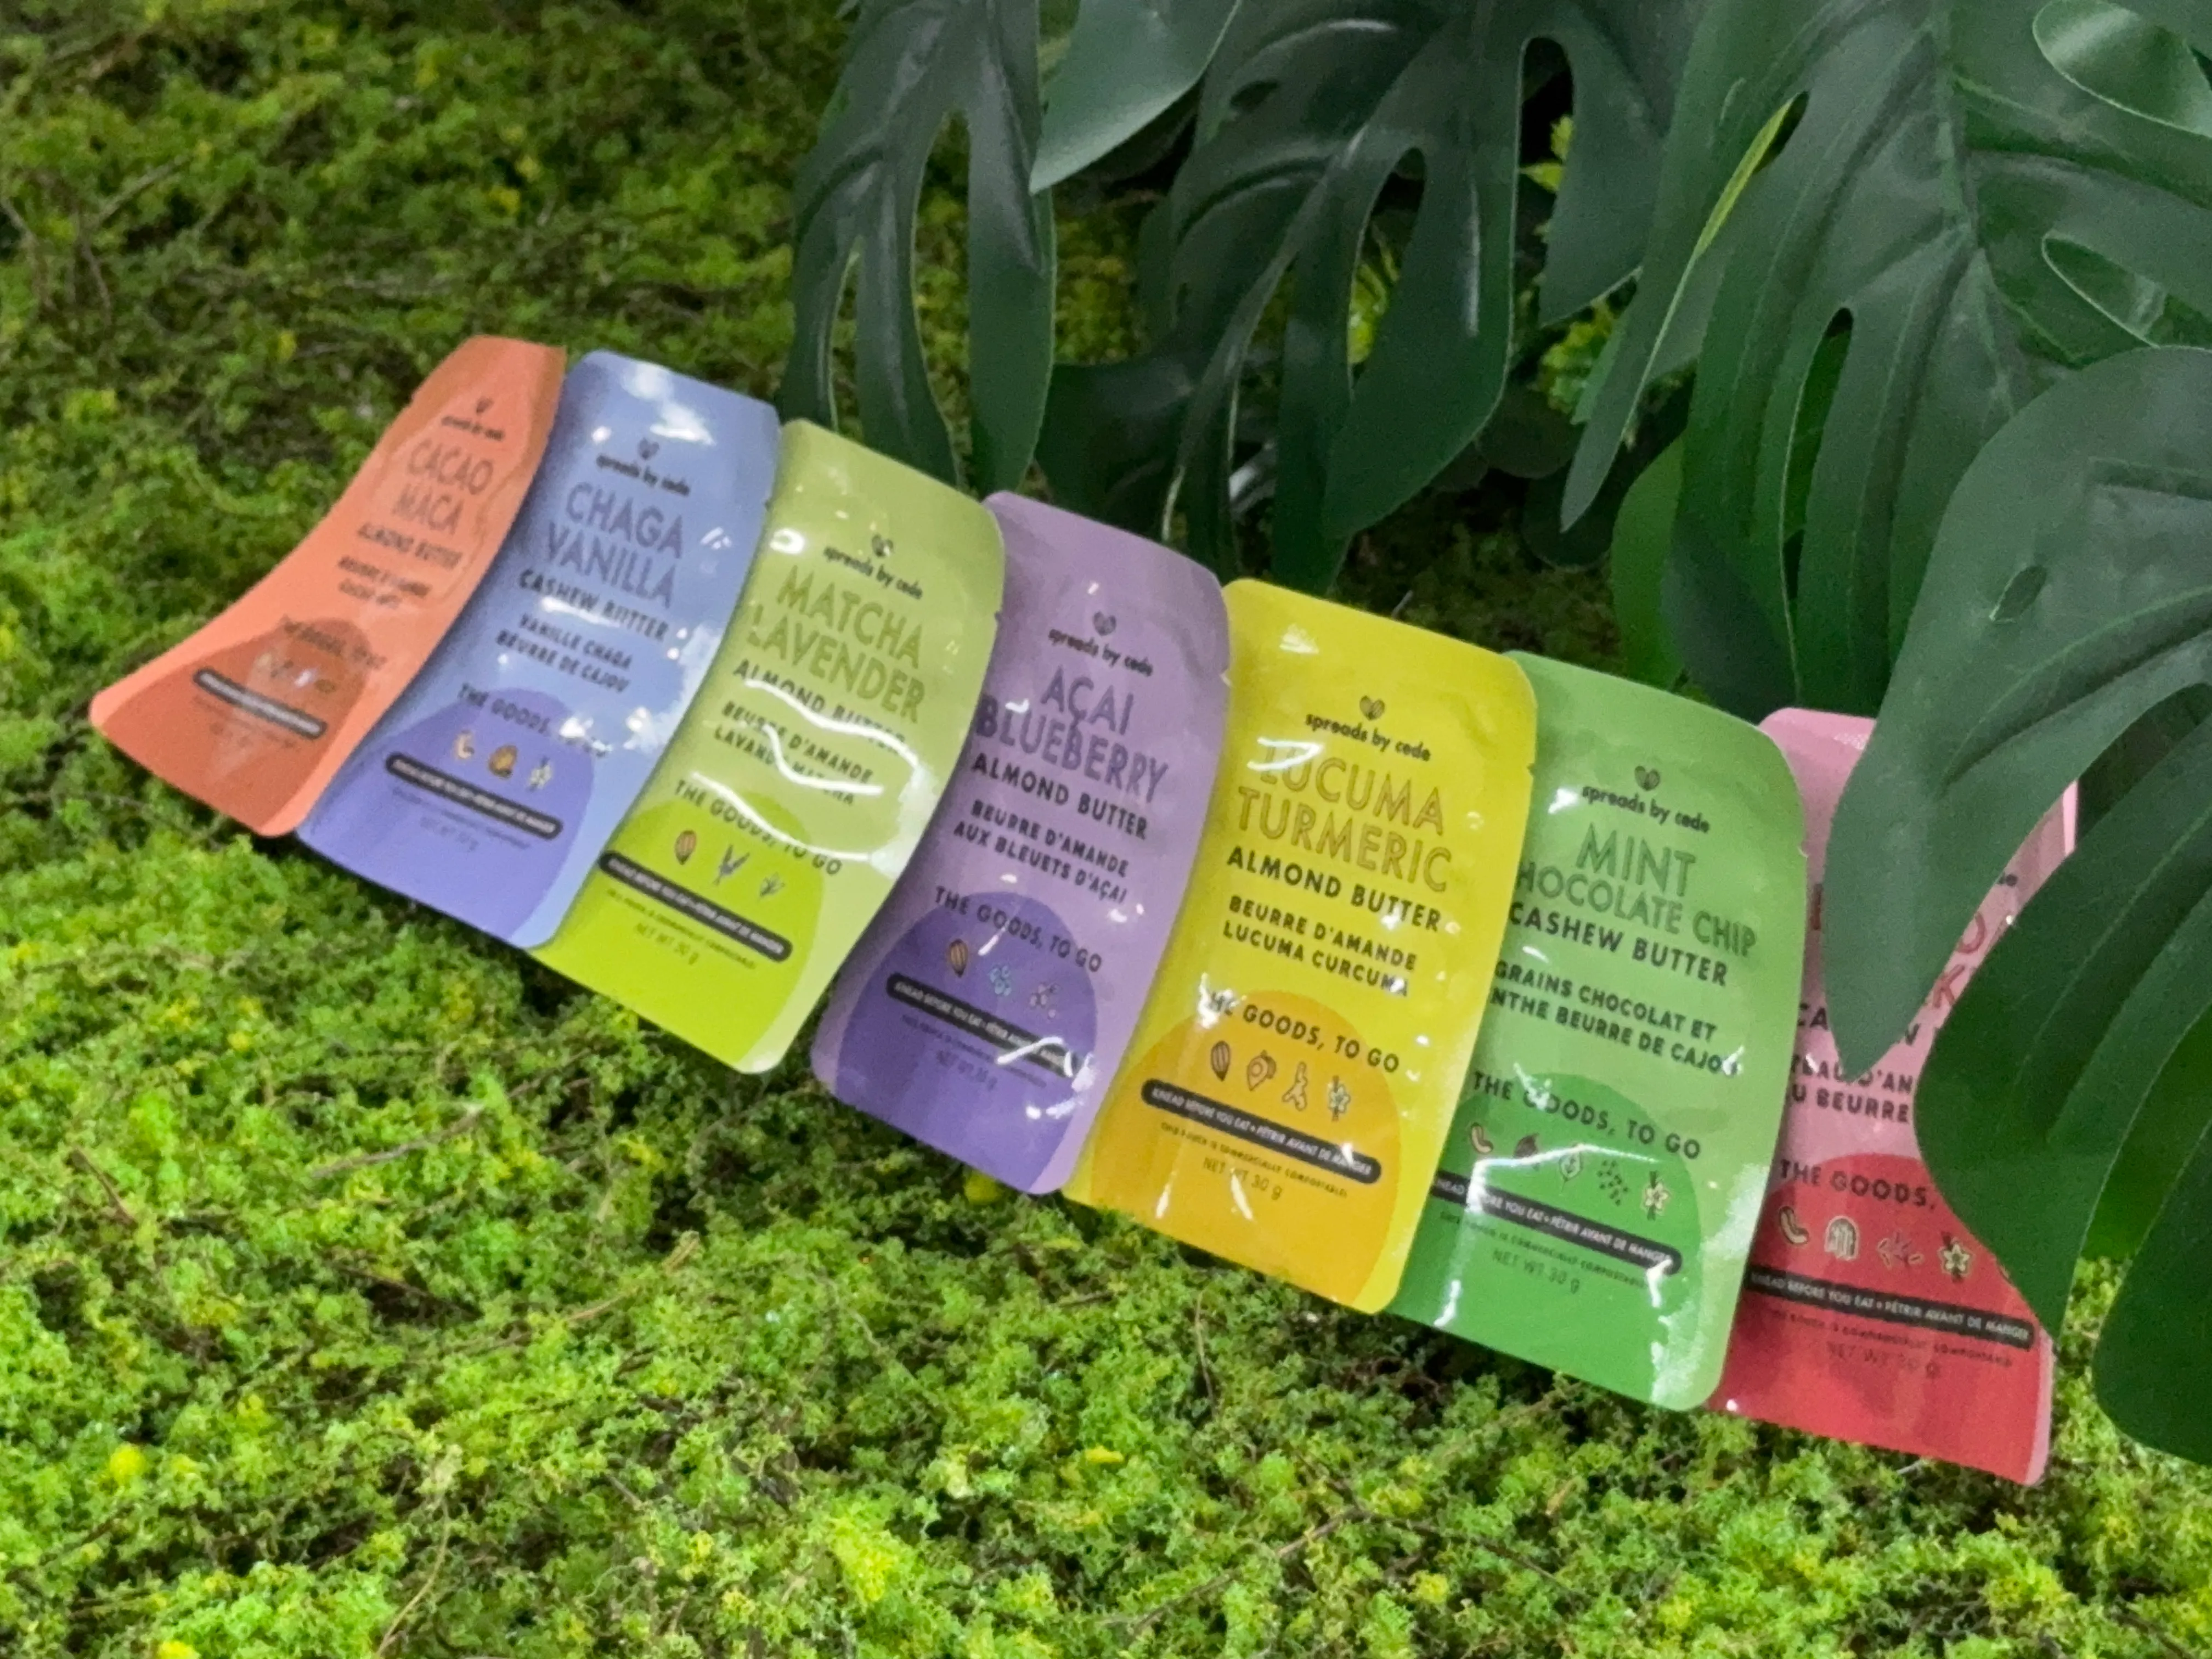
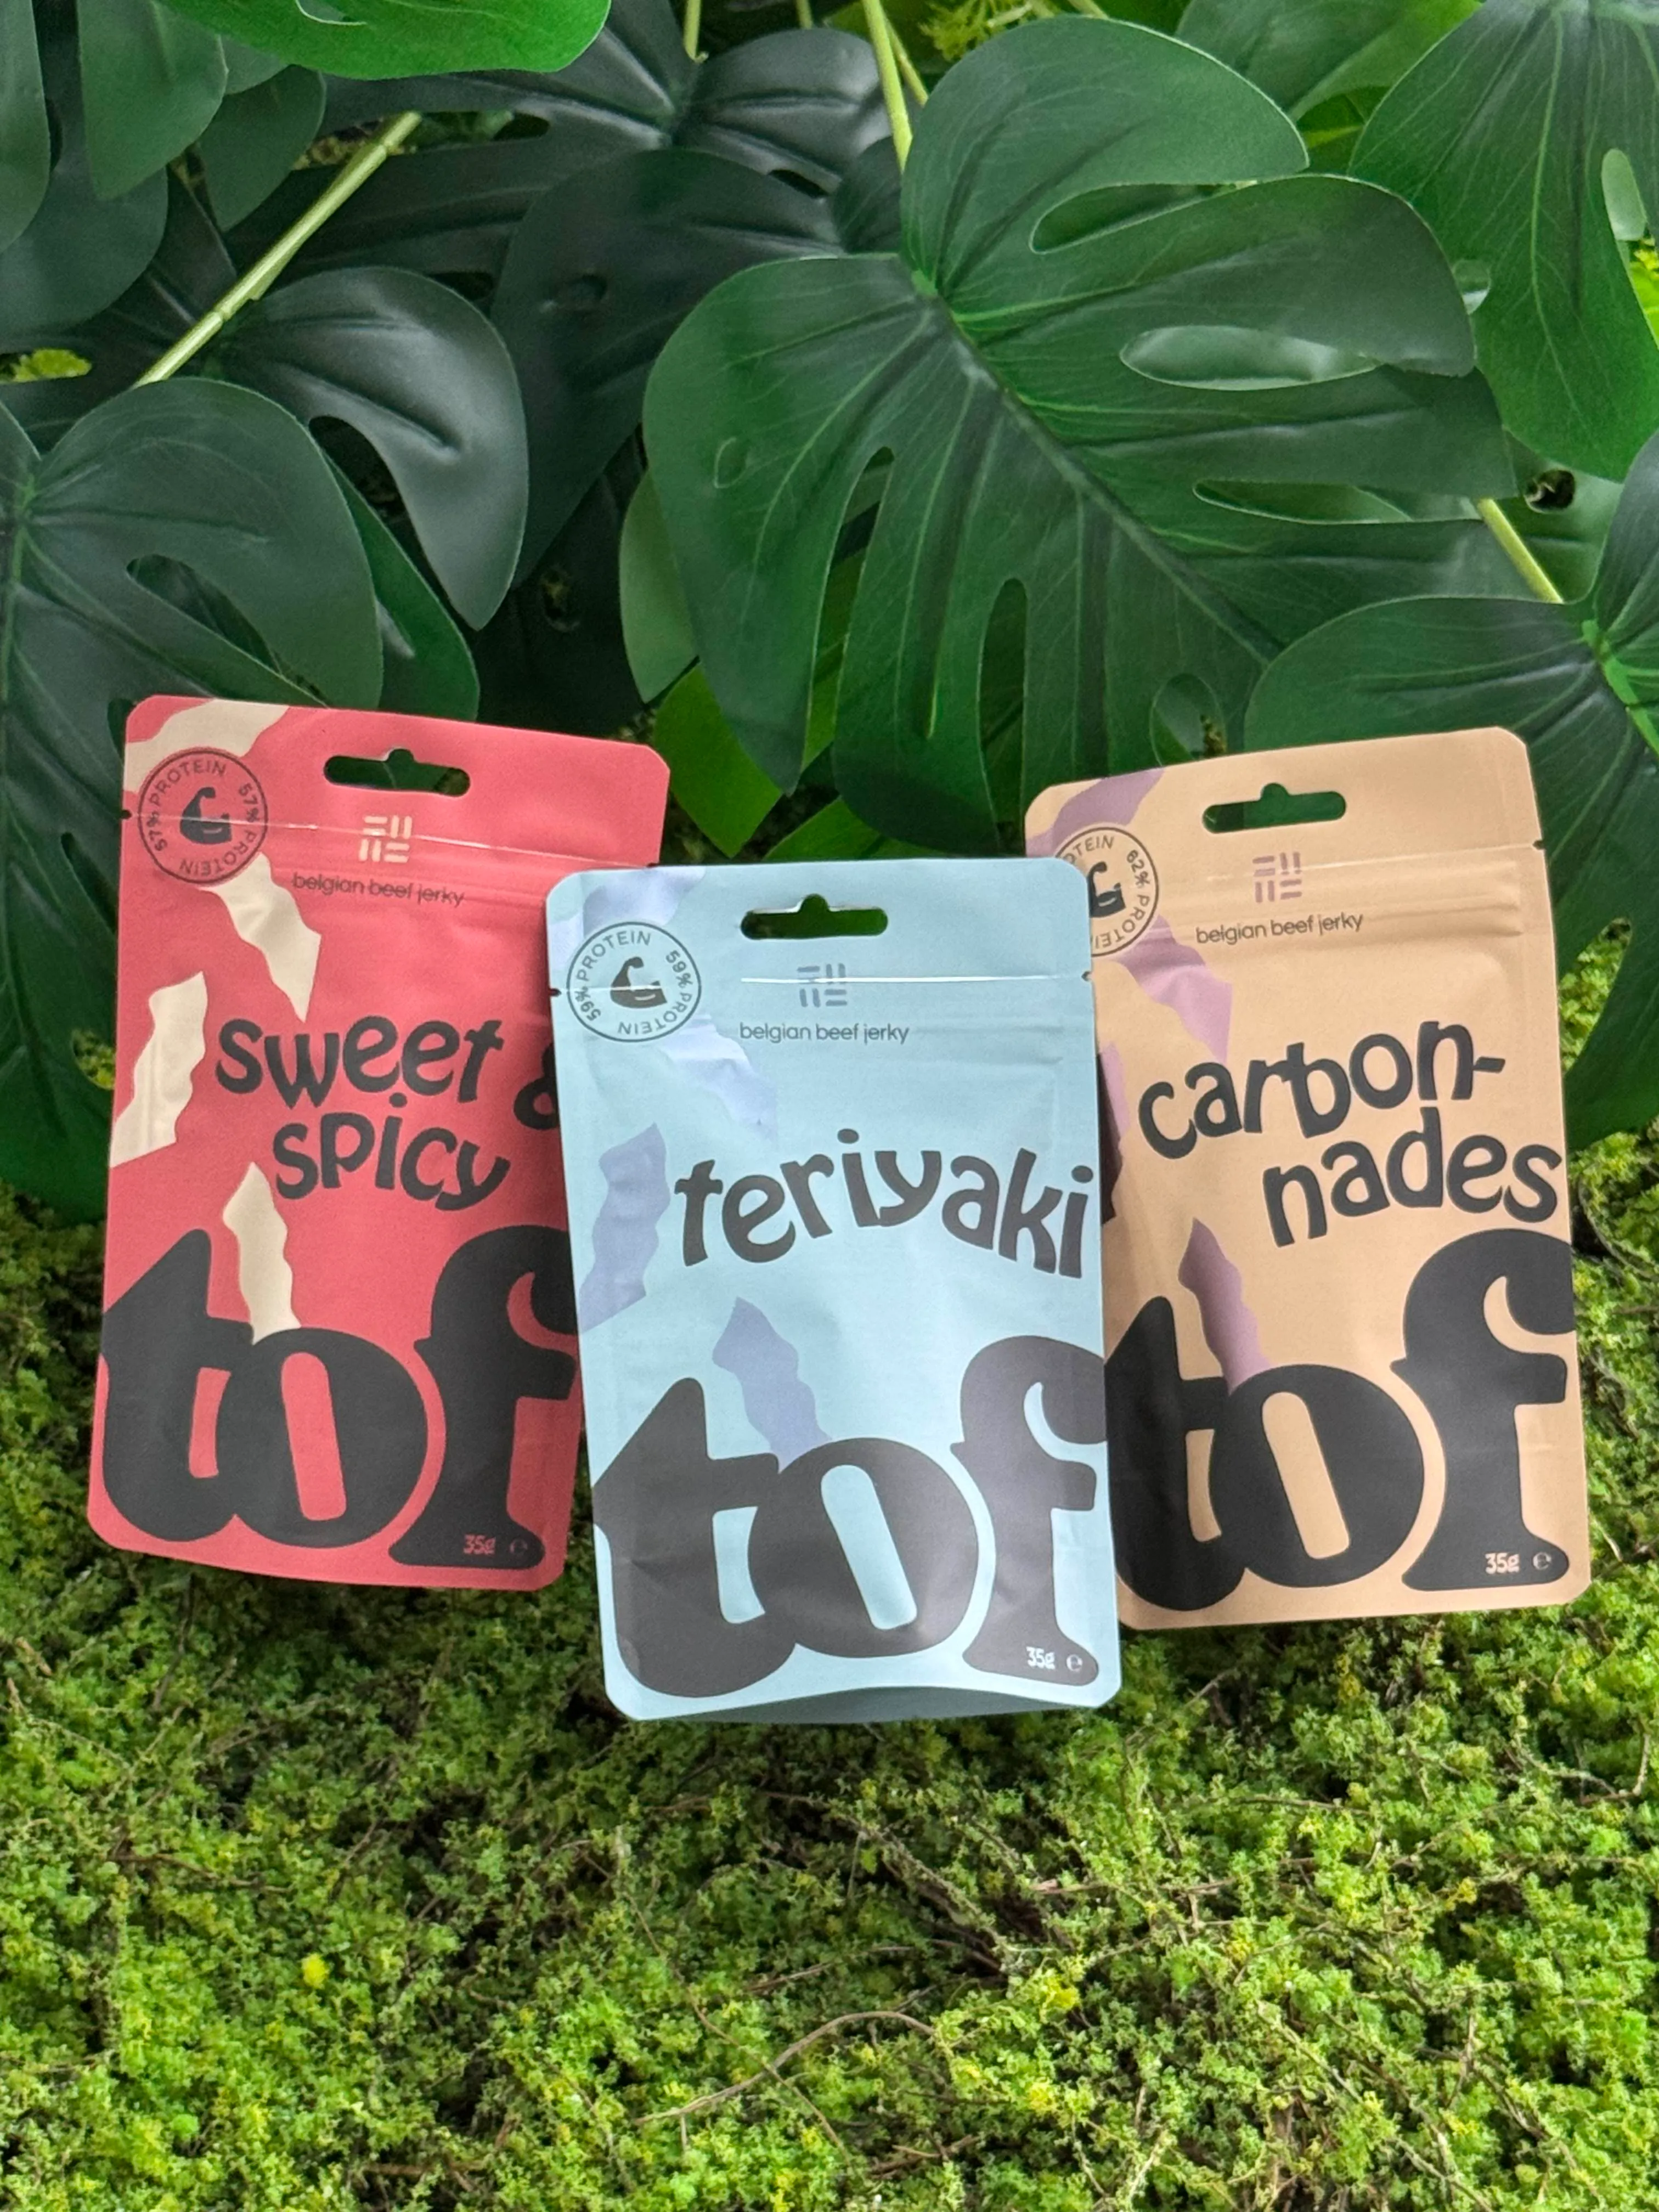
VitalGreen produces organic superfood powders including spirulina, chlorella, and custom blends. As a B-Corp certified company, they needed packaging that matched their environmental commitments while protecting sensitive powder products. They chose Achieve Pack for their recyclable mono-PE solutions.
What Challenge Did They Face?
VitalGreen faced unique powder packaging challenges:
- ✗Oxygen sensitivity of superfood powders required high barrier
- ✗Moisture protection critical for powder quality
- ✗B-Corp certification required documented sustainability improvements
- ✗Multiple SKUs needed with quick market entry
How Did Achieve Pack Help?
We developed recyclable mono-PE packaging with enhanced barriers:
Mono-PE Structure
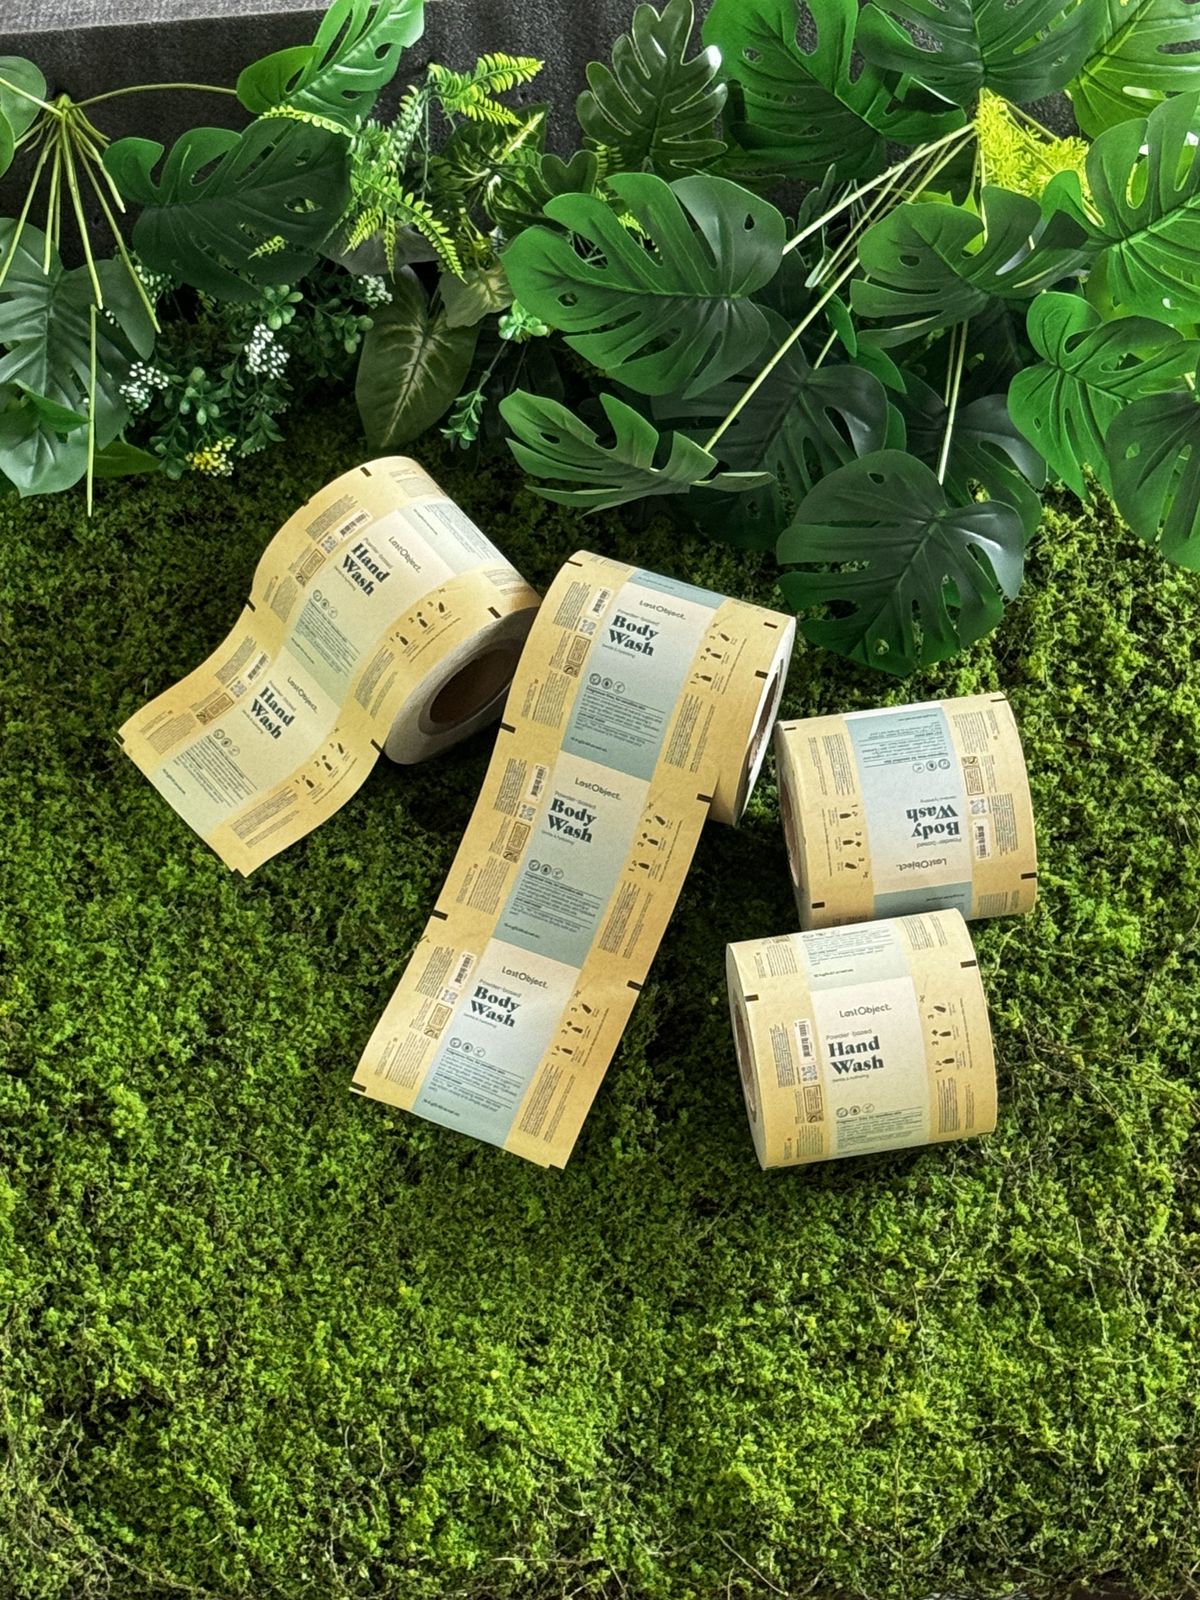
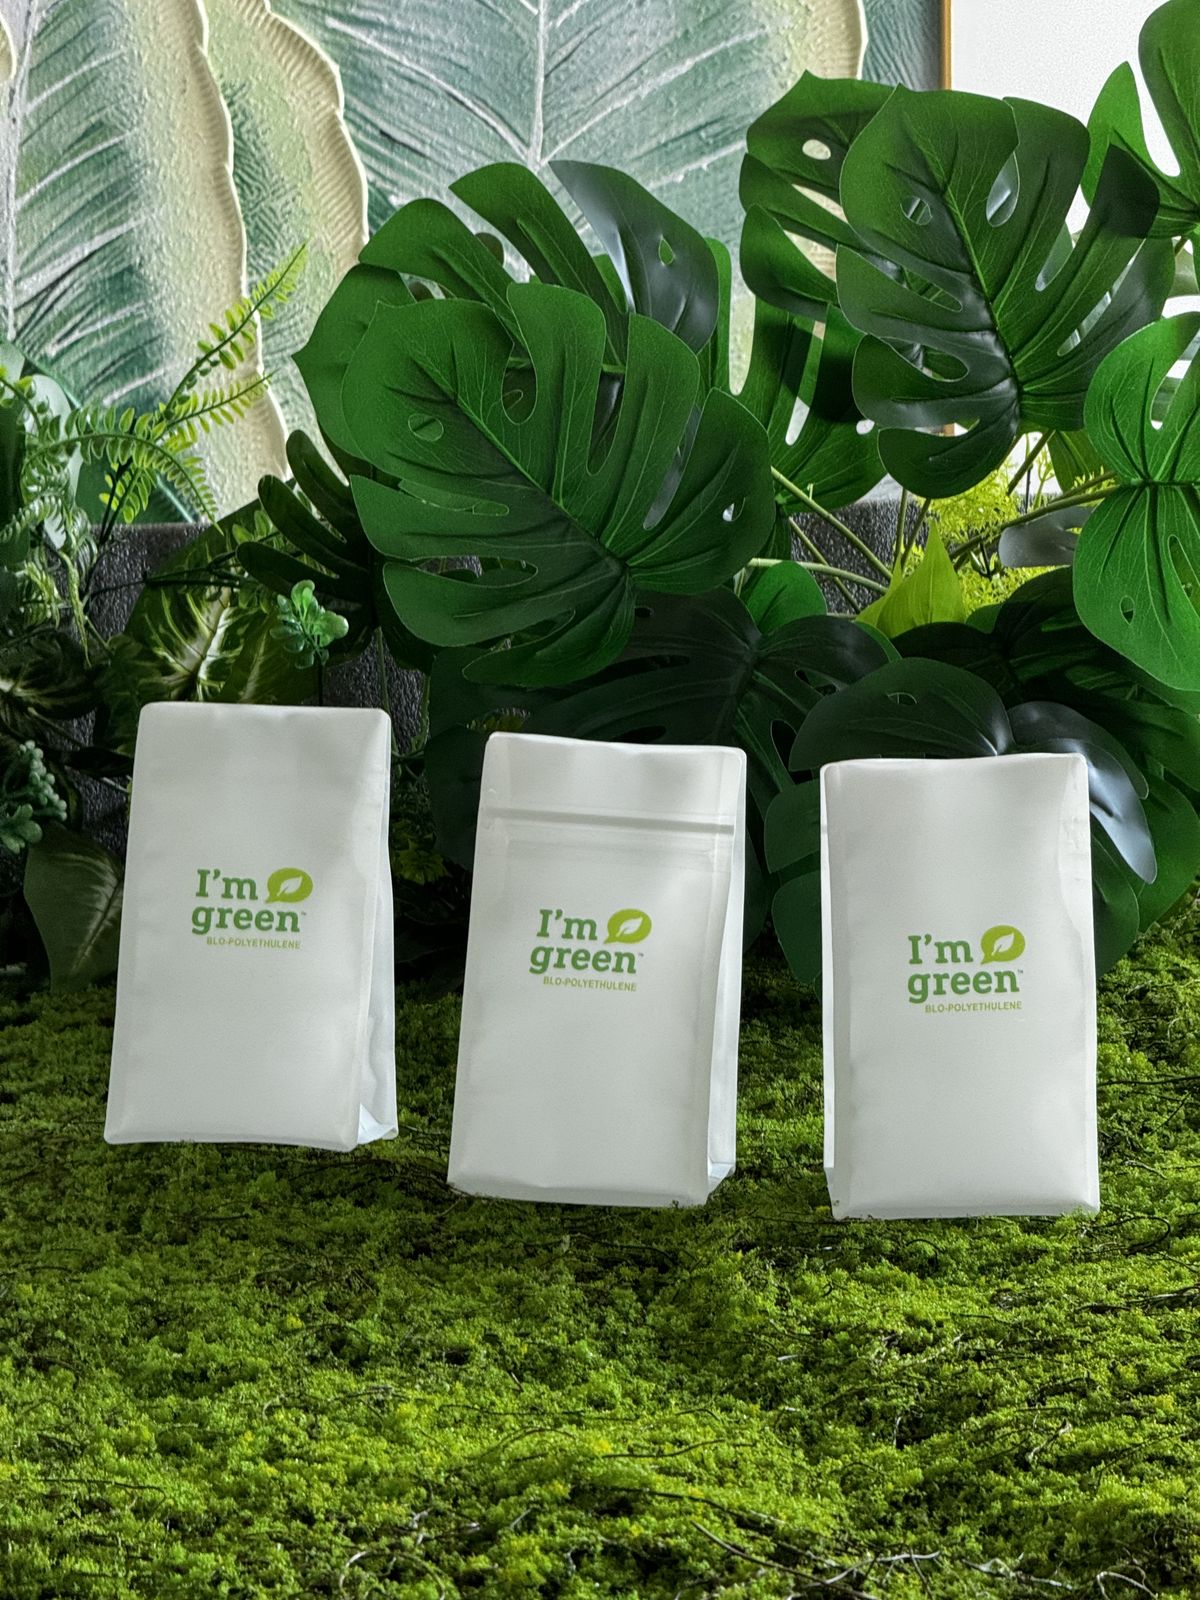
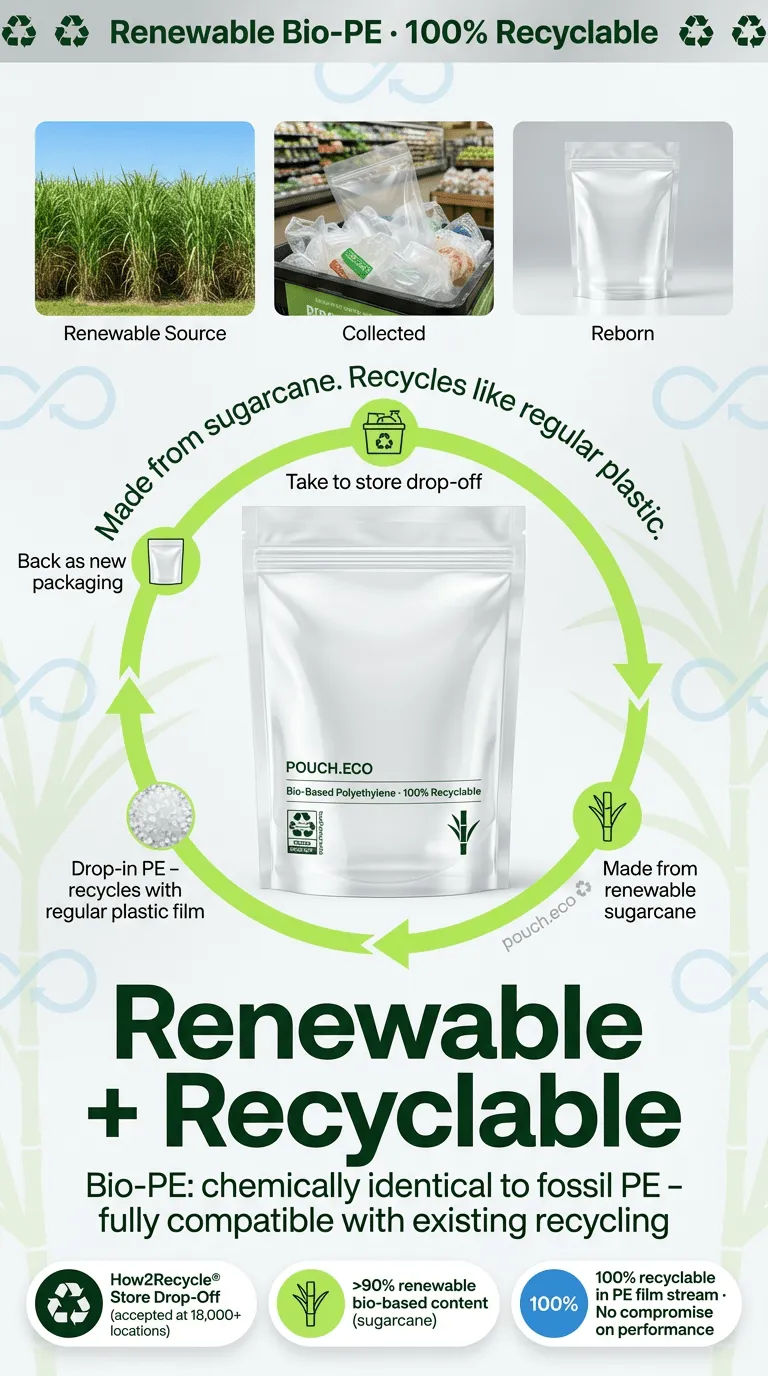
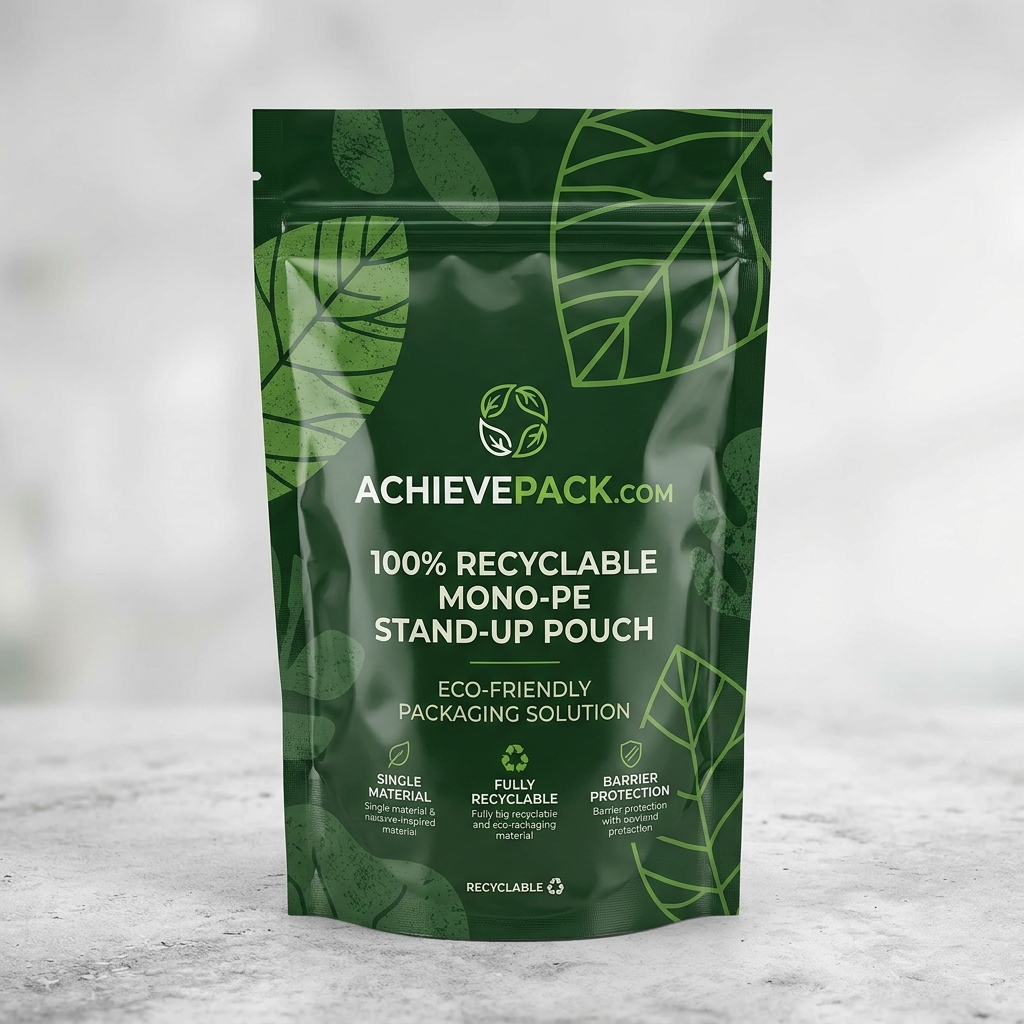
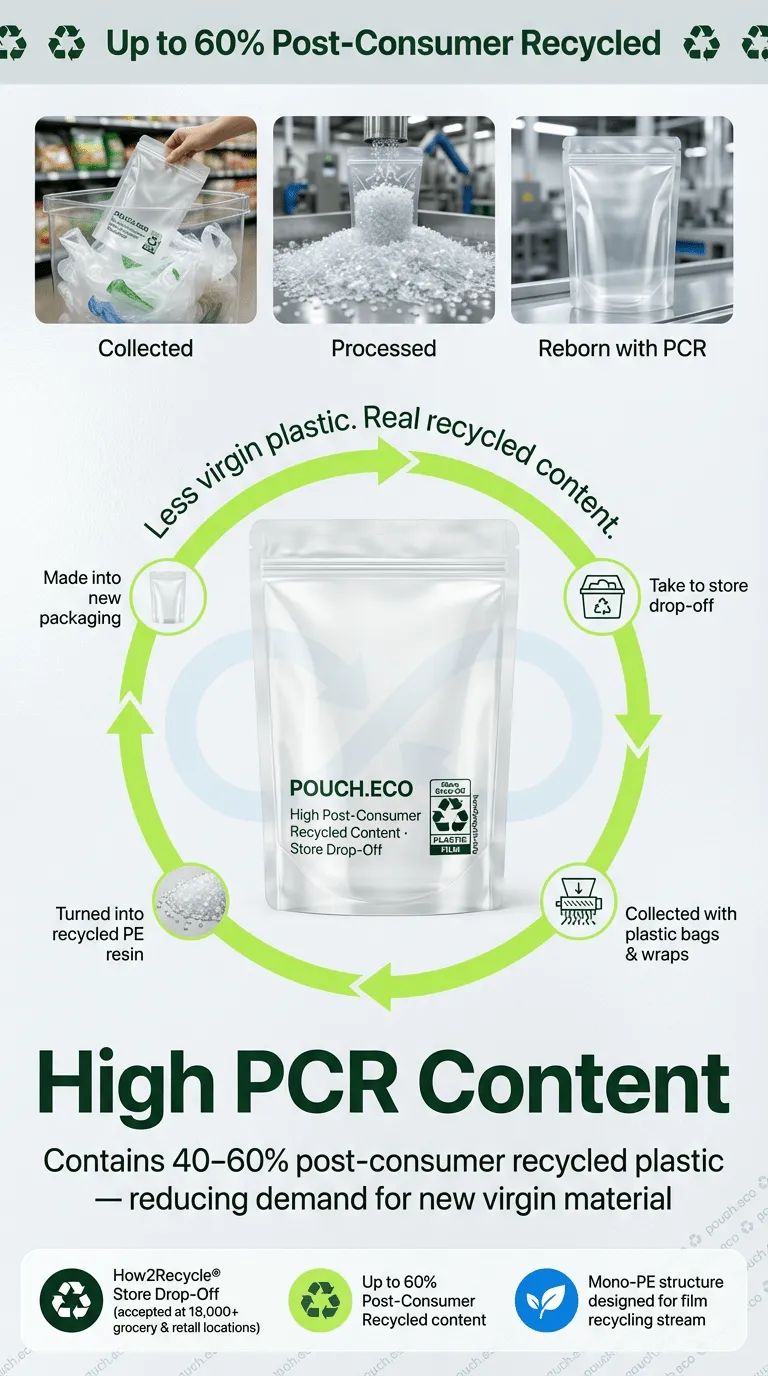
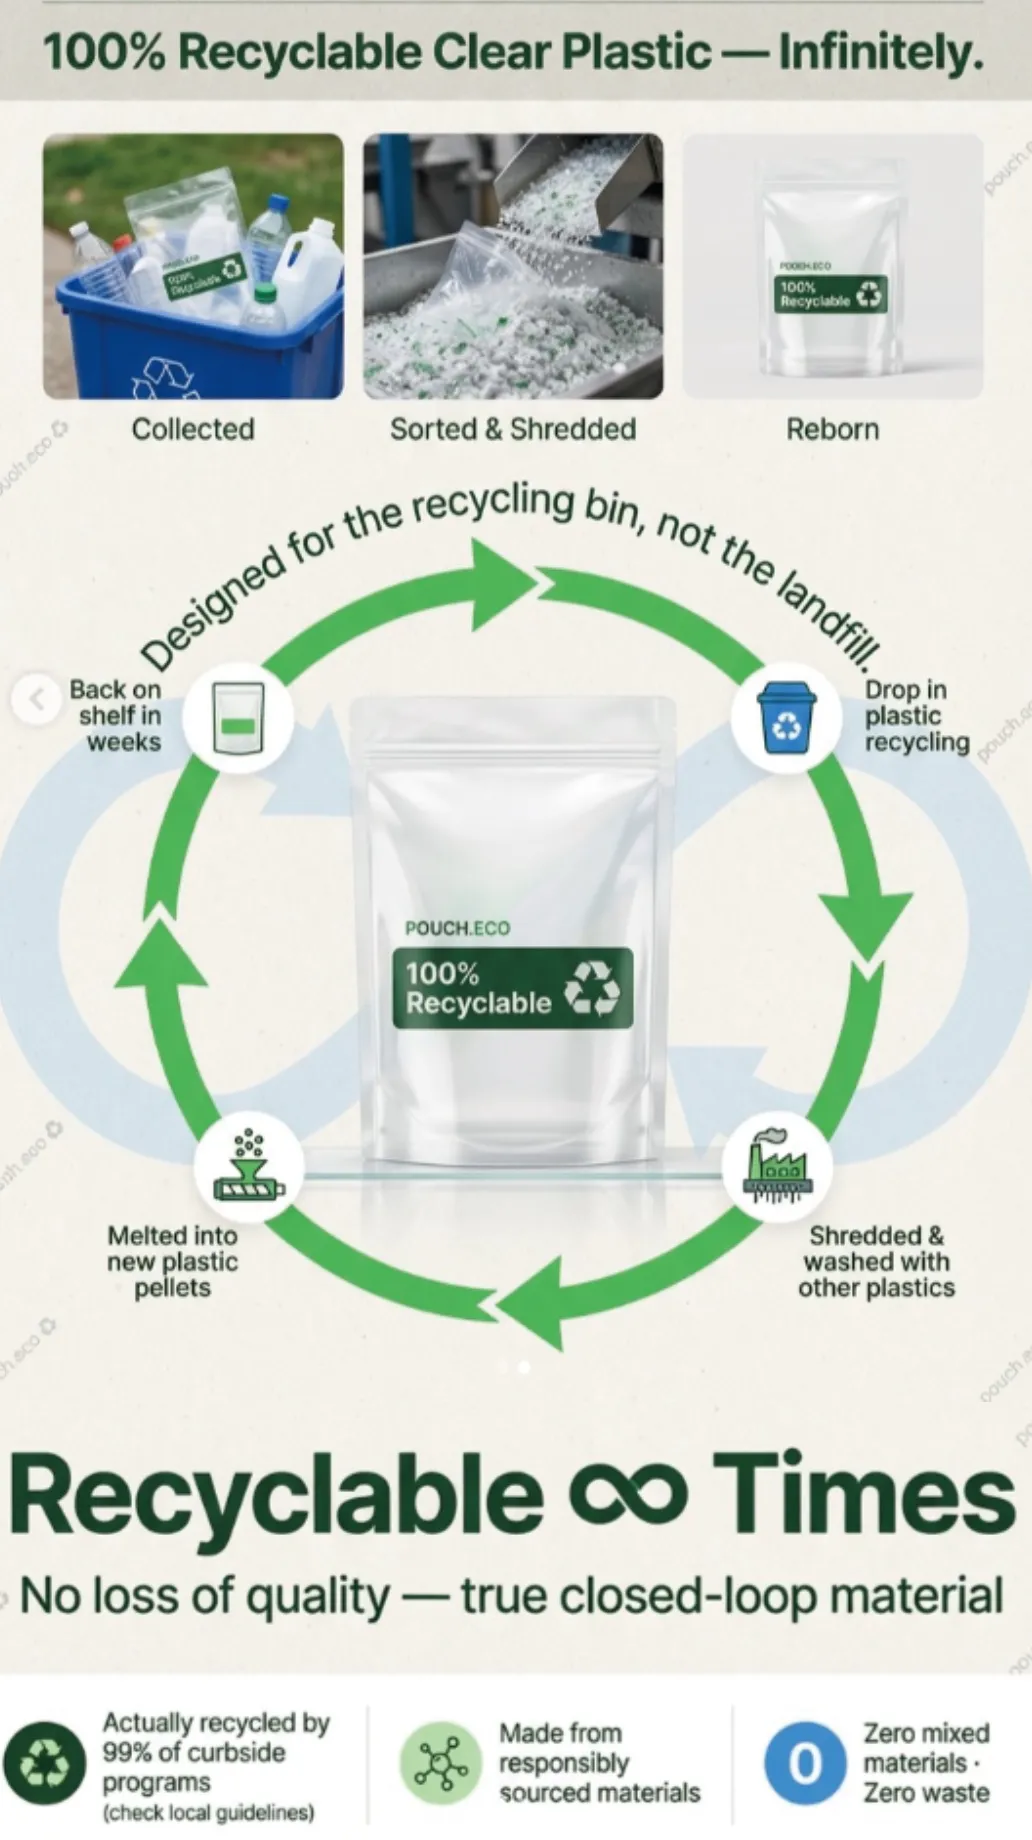
100% recyclable mono-material polyethylene with EVOH barrier layer for oxygen protection. Store drop-off recyclable.
High Barrier Performance
OTR below 1.0 cc/m²/day protects sensitive superfood nutrients from oxidation.
Digital Printing Flexibility
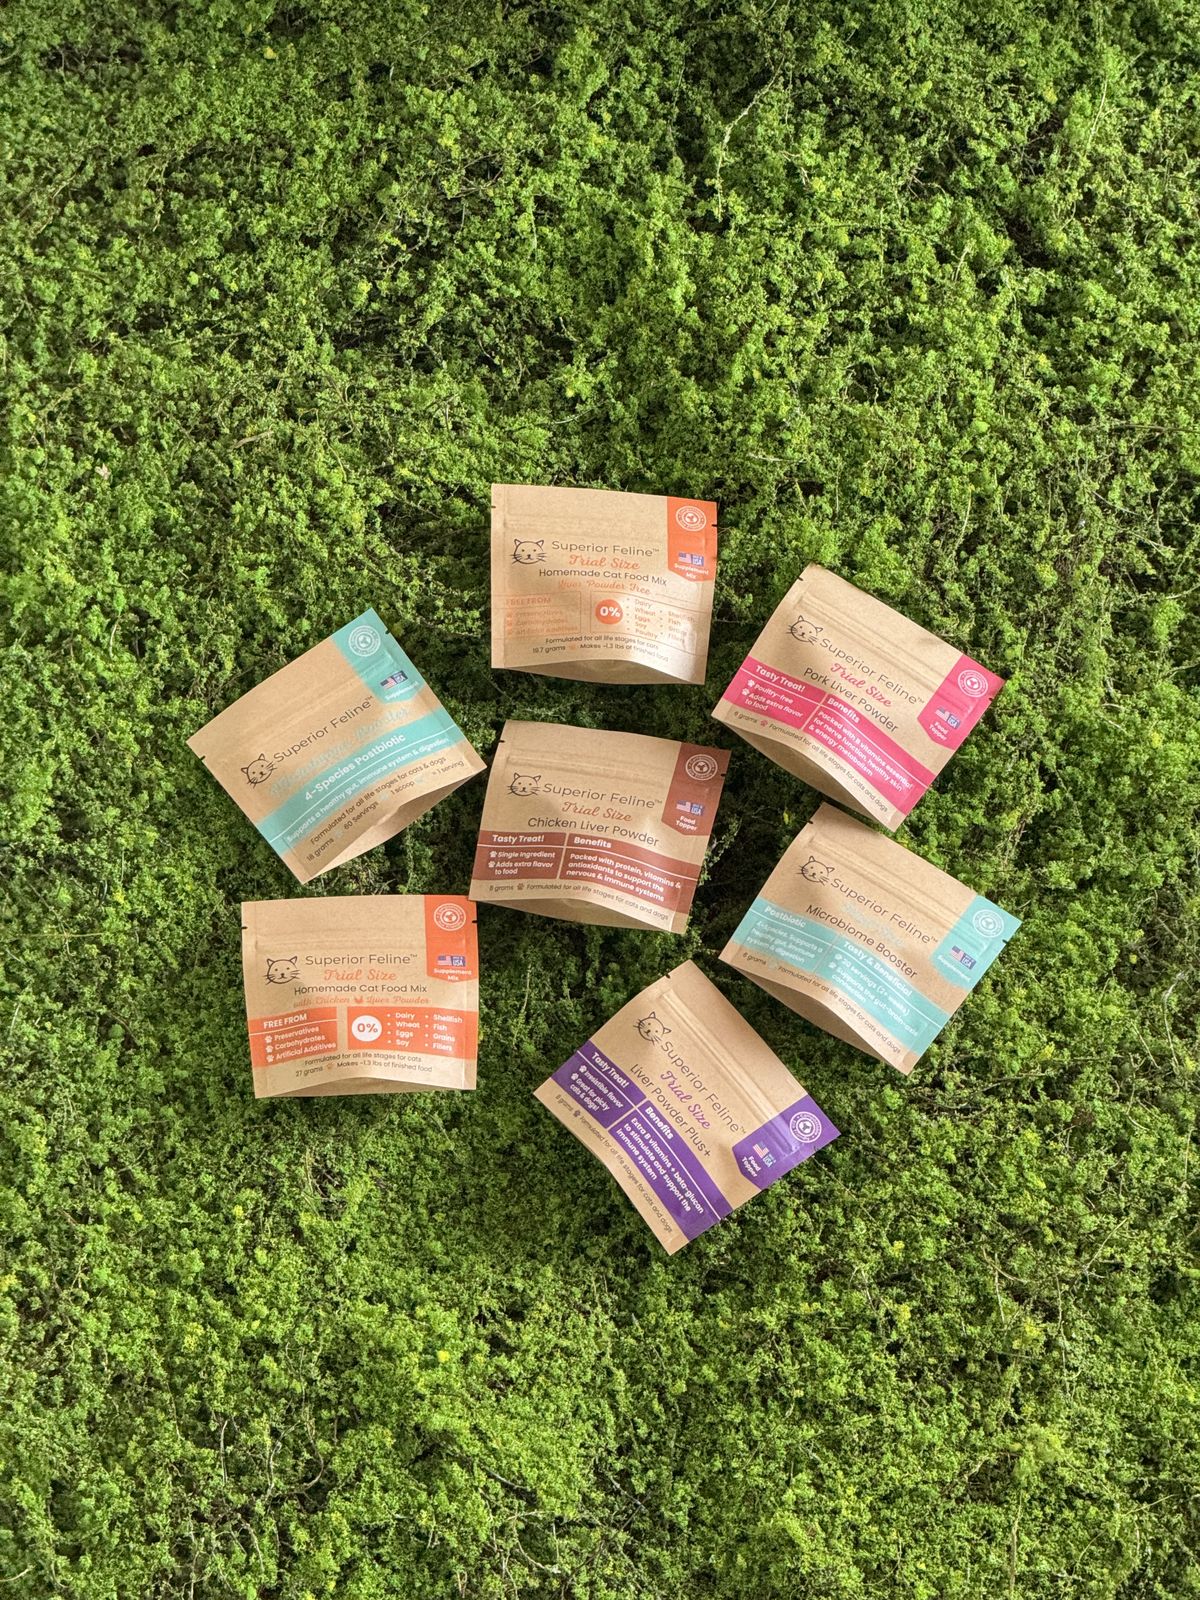
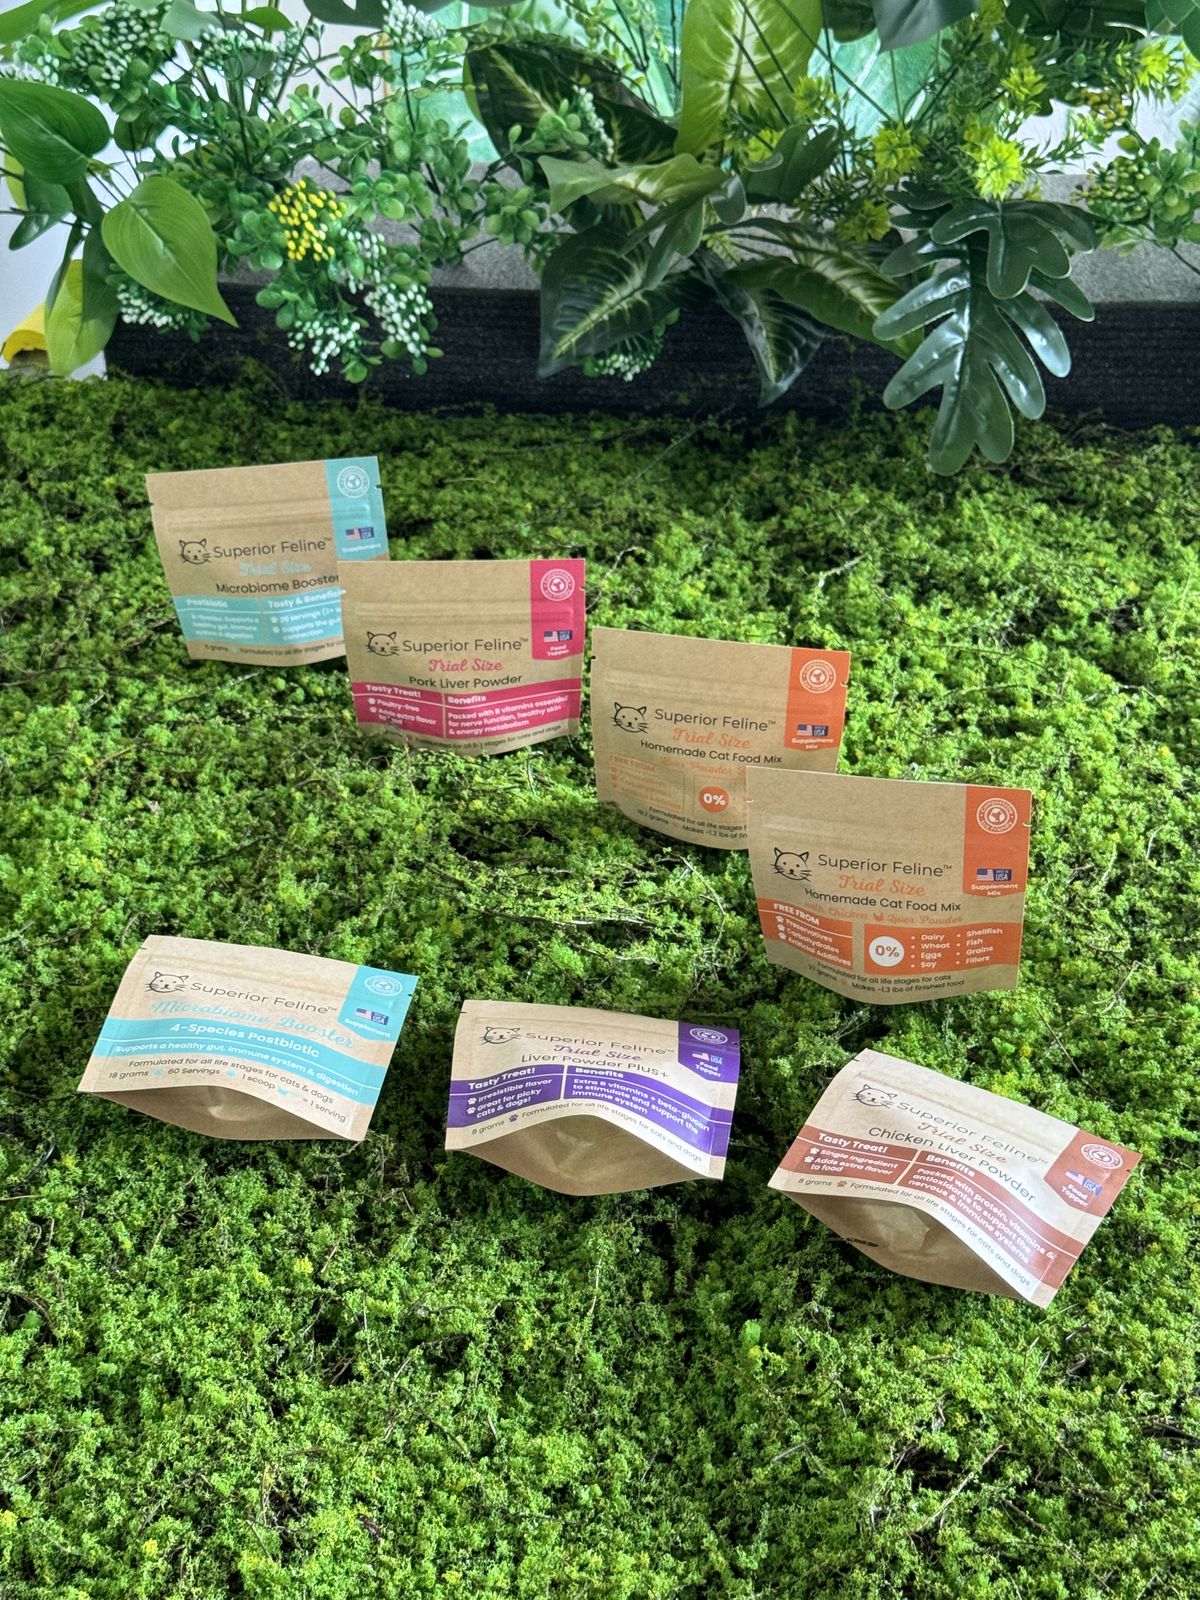
8 SKUs launched simultaneously with digital printing. 500 bags per SKU minimum.
GRS Certification
Global Recycled Standard documentation for B-Corp reporting requirements.
What Results Did They Achieve?
"The GRS certification documentation was exactly what we needed for our B-Corp recertification. Our customers appreciate the recyclable packaging, and our products stay fresh longer than expected."
What Packaging Specs Were Used?
What Can You Learn From This?
What made this project successful for VitalGreen:
- 100% recyclable: Mono-PE structure for curbside/store drop-off recycling
- High barrier: OTR < 1.0 protects sensitive superfood nutrients
- 8 SKUs launched: Digital printing enabled quick market entry
- B-Corp documentation: GRS certification for sustainability reporting
Mono-PE & Mono-PP Mechanical Validation
Single-polymer bags must match the physical performance of multi-layer co-extrusions. We test MDO-PE orientation, EVOH content, and sliding friction to enable flawless high-speed packaging runs and curbside recycling.
EVOH High Barrier Ratio
Maintains high barrier performance while meeting circular economy recycling rules.
ASTM D882 Tensile Test
Mechanical tensile strength ensures bag retains structural form under stress.
Heat Seal Window (ASTM F88)
Enables hermetic seals without melting or shrinking the mono-PE outer layers.
RecyClass Sorting Grade
Certified sorting compatibility in standard municipal recycling streams.
Puncture Test (ASTM F1306)
Prevents bag tears and punctures from dry pet kibbles or sharp snacks.
Friction Coefficient (COF)
Ensures film glides smoothly over packaging machinery forming collars without jamming.
Packaging Transformation for Superfood Brand Case Study | Recyclable Mono-PE Packaging for B-Corp Certified Brand
See how upgrading from generic commoditized bags to precision-engineered flexible barrier packaging eliminates transport failures and boosts shelf authority.
Standard / Generic Packaging (Before)
Standard stock bags fail under transit stress and expose sensitive goods to moisture, UV light, and oxygen.
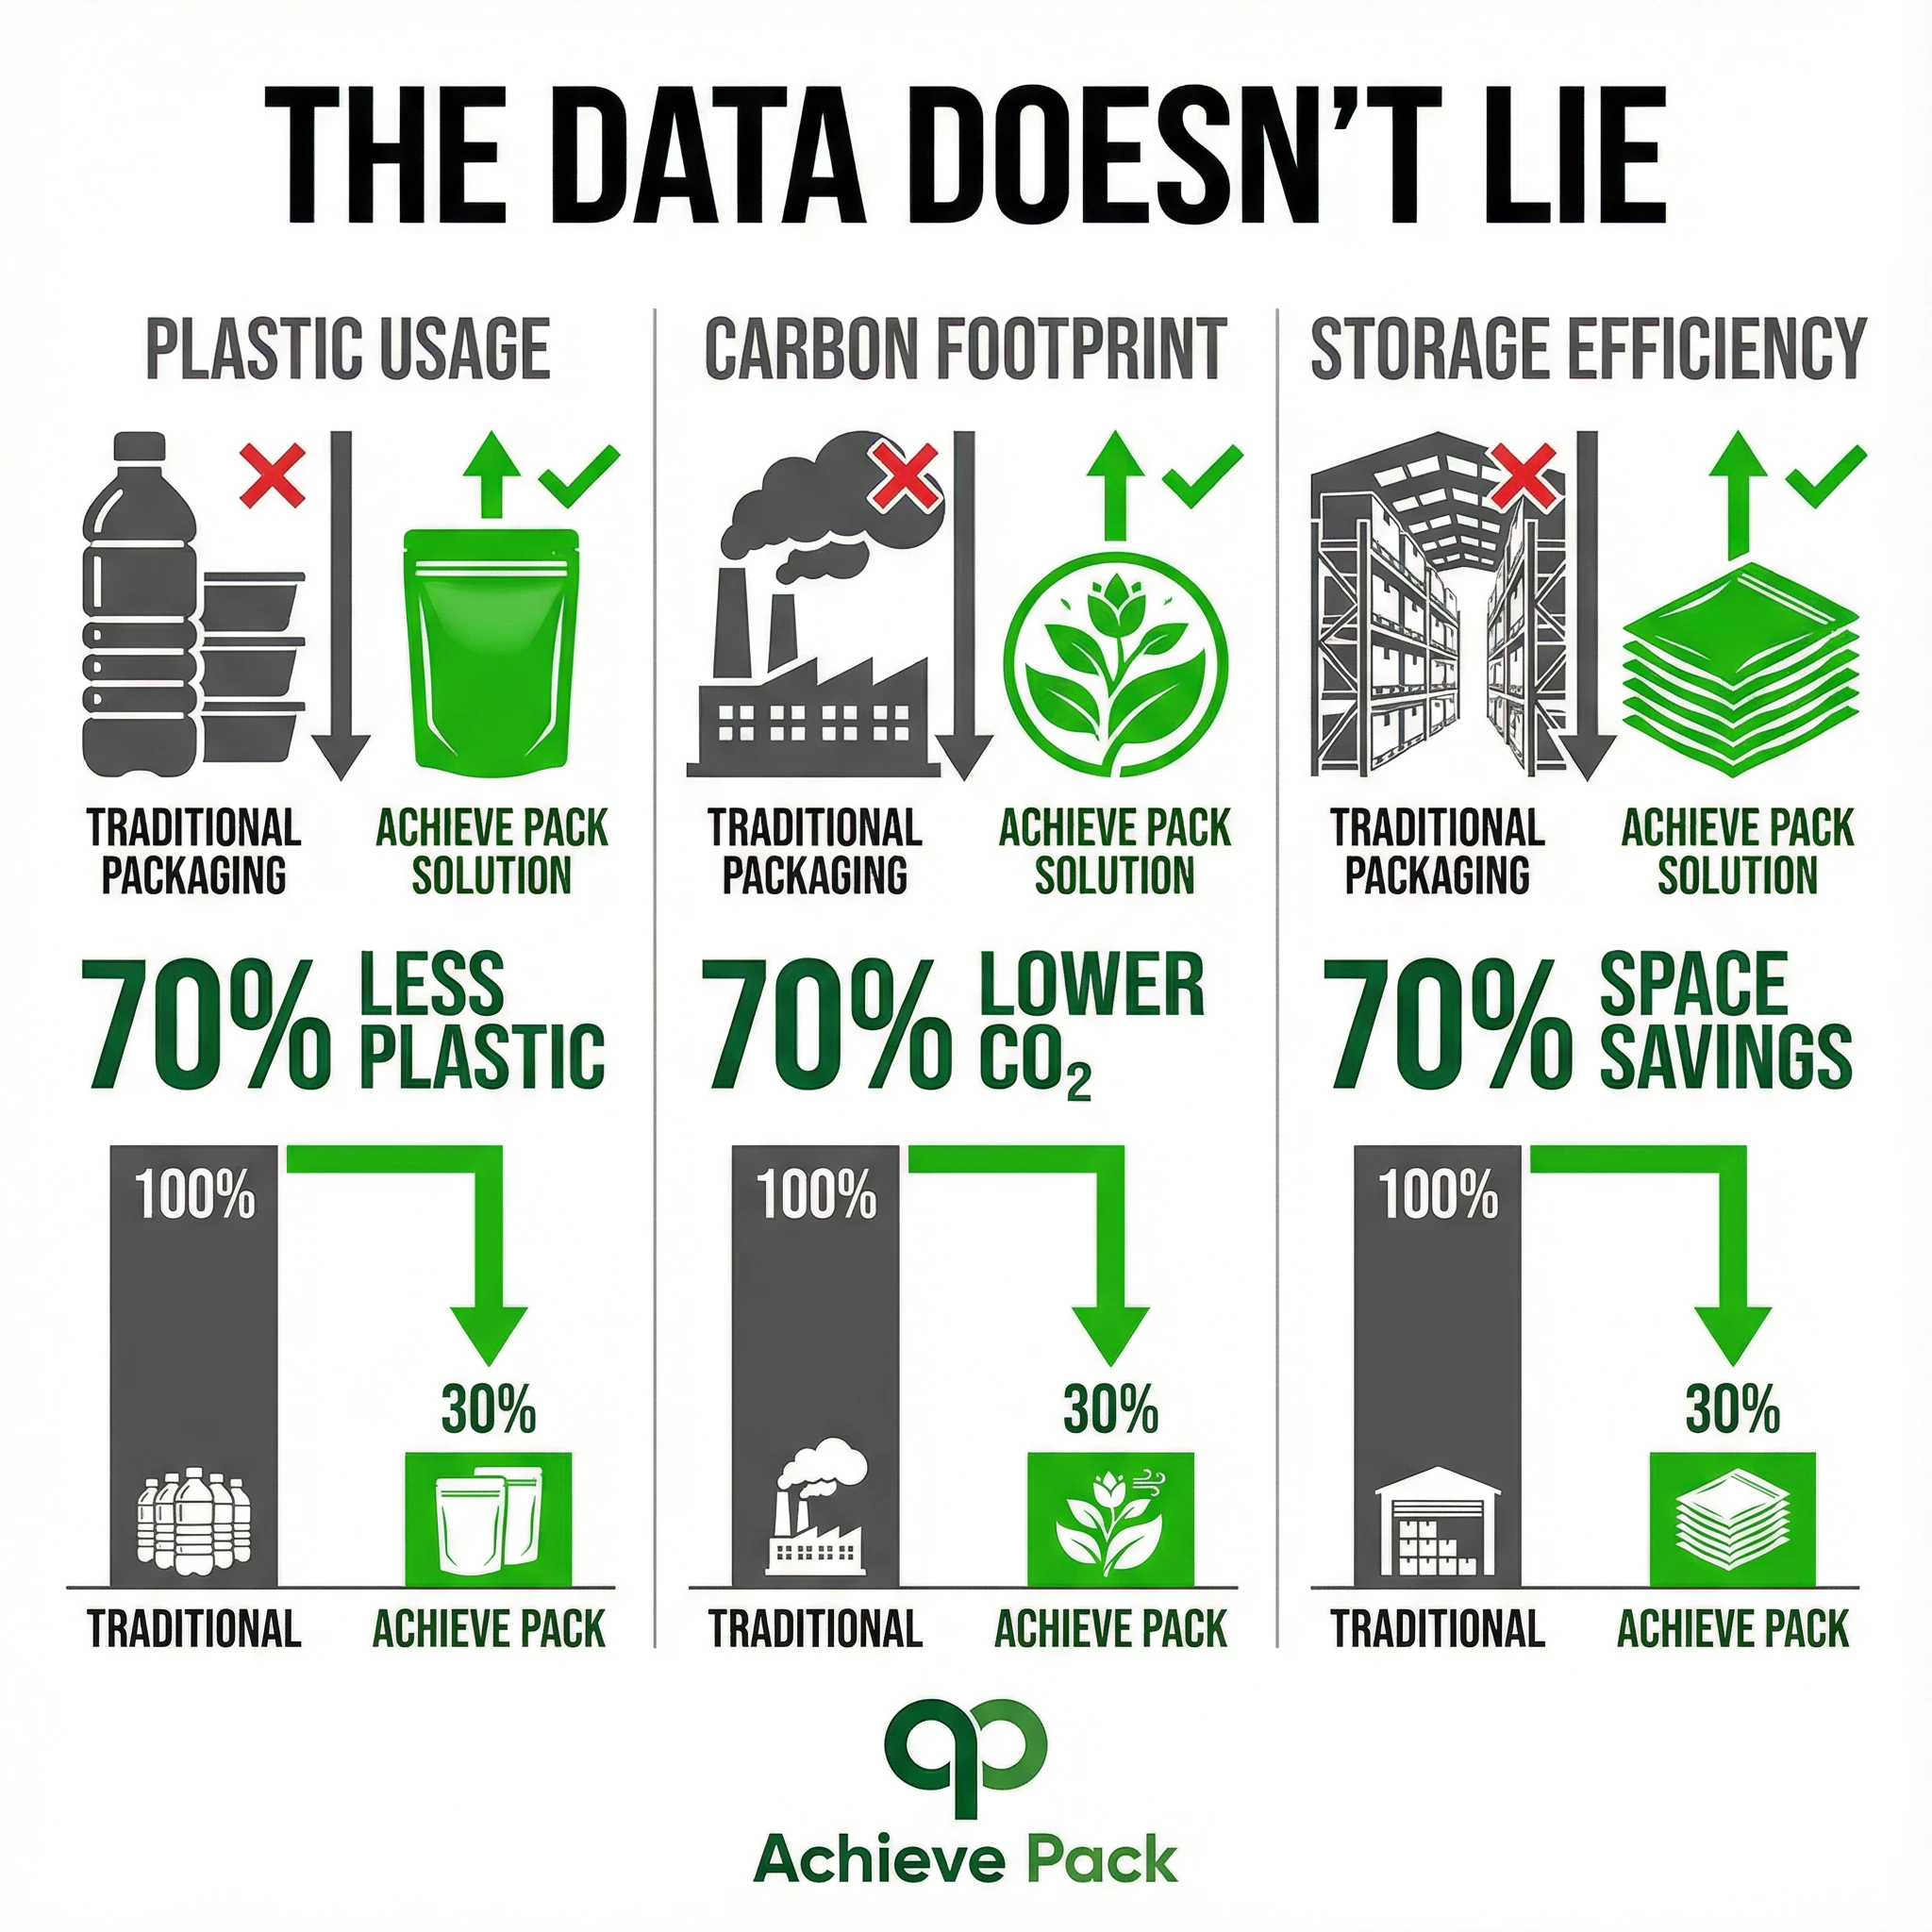
- Rapid Oxidation & Flavor DegradationCheap films allow O2 & moisture ingress, spoiling contents in < 30 days.
- High Seal Breakage in TransitThin seams fail under drop tests, leading to customer refunds & lost trust.
- Heavy Plastic Tax PenaltiesMulti-layer unrecyclable packaging incurs up to €800/ton in EU PPWR fines.
- High MOQs & Plate Cost FrictionTraditional printers force 10,000+ unit minimums and $1,500 cylinder fees.
Achieve Pack / Pouch Eco Solution (After)
Custom engineered multi-layer pouch structure tailored to your exact moisture barrier, seal strength, and aesthetic requirements.
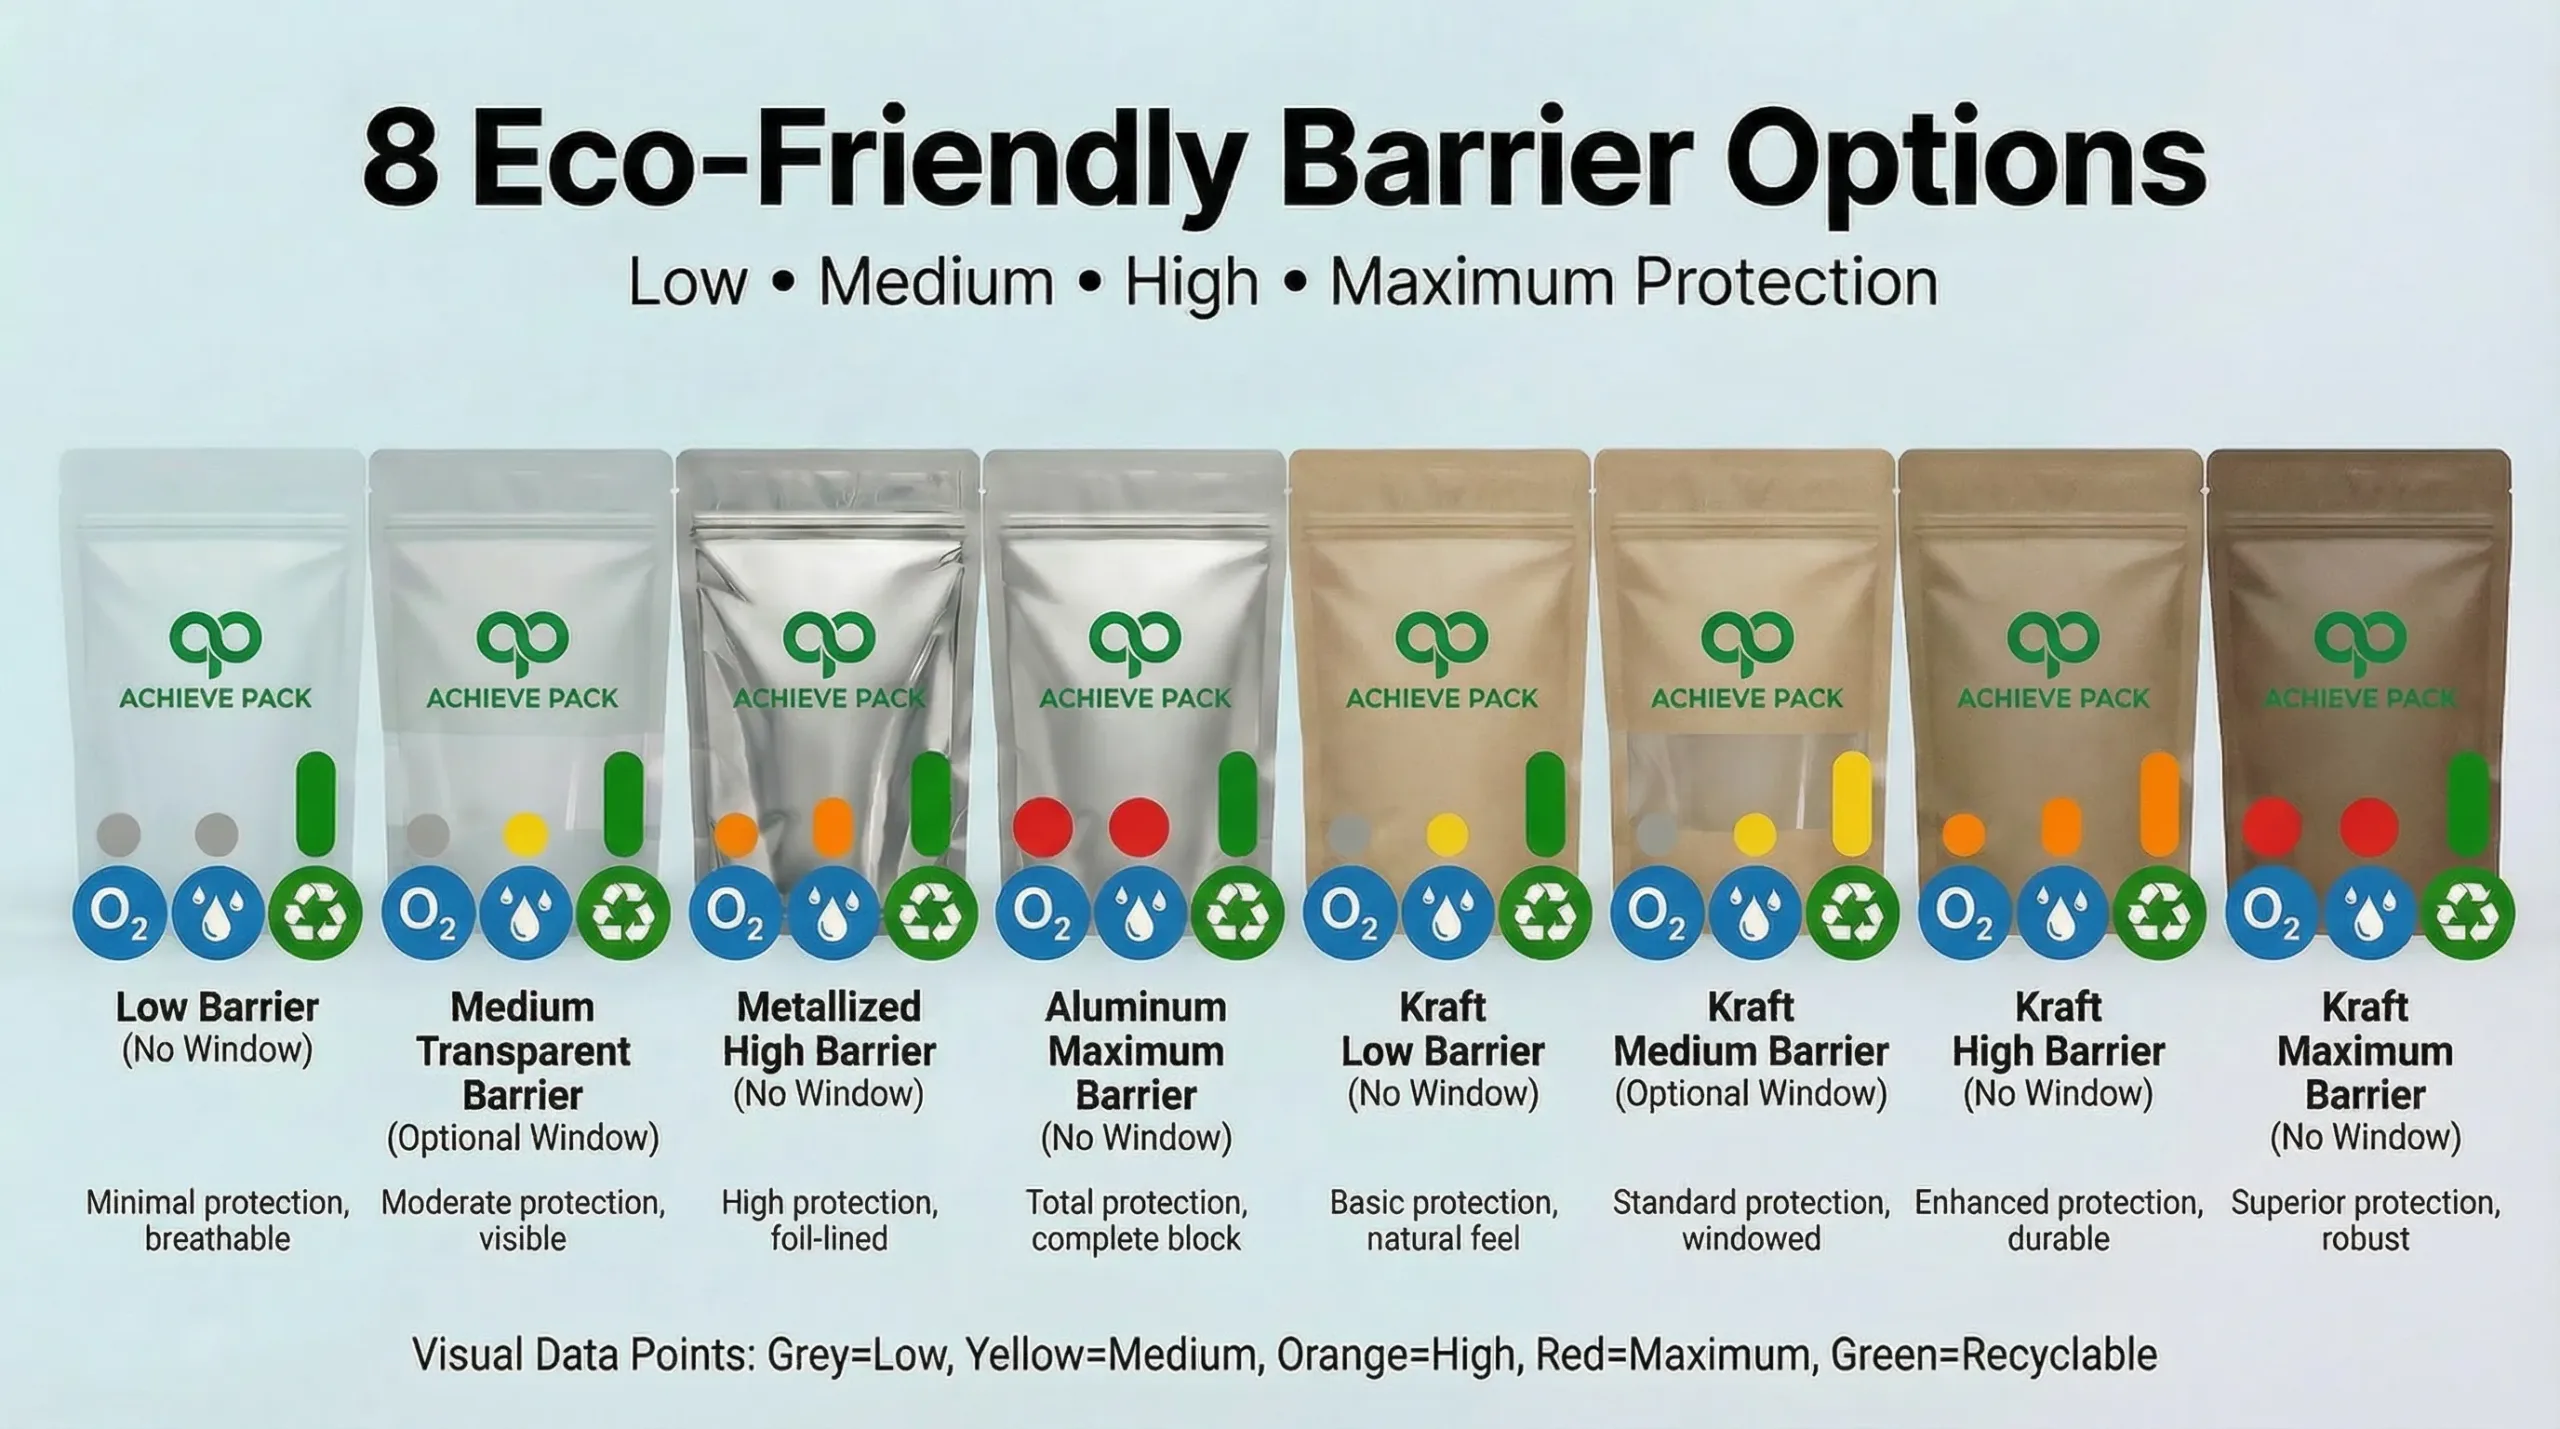
- Ultra High-Barrier Foil/EVOH CoreGuaranteed OTR < 0.1 cc/m²/day, keeping contents fresh for 18–24 months.
- Reinforced 45N/15mm Localized Heat Seal180°C precision seam dwell time prevents bursting even under 2-meter drops.
- 100% Certified Eco ComplianceTÜV OK Compost HOME (EN13432) & Mono-PE Recyclable structures (0% Tax).
- HD Digital Printing with 500-Unit Low MOQsPrint multi-SKU runs in 7 business days with zero setup plate charges.
Questions We Get Asked
What is mono-PE recyclable packaging?▼
Can recyclable packaging have high oxygen barriers?▼
What documentation do you provide for B-Corp certification?▼
What is the MOQ for digital printed superfood pouches?▼
How do you protect superfood powder from clumping?▼
Related Stuff
How We Ensure Absolute Accuracy and Trustworthiness
At Achieve Pack, sustainable packaging isn't just about printing; it's about hands-on material science. This article has been written and verified by Ryan Wong, a packaging specialist with 14+ years of experience engineering biopolymer stacks for DTC startups and Fortune 500 companies.
All research, material barrier specifications (OTR, WVTR), heat-seal values (N/15mm), and compostability timelines cited in our guides are backed by testing inside the Achieve Pack Materials Testing Lab. We cross-reference our data with official certification registries from BPI (Biodegradable Products Institute), TÜV Austria (OK Compost HOME), and FSC (Forest Stewardship Council).
Ryan Wong
Supply Chain Director
B.Eng honors degree graduate from Hong Kong Polytechnic University. Serving brands in 8 countries.
View Expert Profile →Packaging for Your Wellness Brand
Let's create recyclable packaging that meets your sustainability goals.
Recyclable Mono-Material
Engineered using Mono-PE or Mono-PP structures to enable simple, circular sorting and recycling. Combined with specialized high-barrier coatings to preserve freshness without compromising recyclability.
- 100% recyclable mono-polymer structure
- Meets EU Circular Economy directives
- EVOH barrier layer for oxygen protection
- Highly customizable surface finishes